

Lean Studio board · Problem solving
Fishbone diagram template (Ishikawa, 6M)
In one sentence
A fishbone diagram, also called an Ishikawa or cause-and-effect diagram, sorts every possible cause of one problem into categories, usually the six M's, so a team sees where the causes cluster before it tests any of them. A fishbone diagram template gives you that chart ready drawn, with the bones labelled.
This free fishbone diagram template comes three ways: a printable PDF for a session at the line, an Excel cause list, and a Lean Studio board for a team on screens. The Ishikawa diagram template has the problem statement at the head and six bones for the six M's: man, machine, method, material, measurement and mother nature. Page 2 of the PDF is the same sheet filled in for a scrap problem on a stamping line, so you can see what good looks like before you start. Kaoru Ishikawa, who first used the diagram in 1943, describes it in his Guide to Quality Control.
Free to use: print it, copy it and edit it for your team. Enter your name and work email once to download.
When to use it
When to use the Fishbone (Ishikawa) board
- At the start of a root cause analysis, once the problem is defined and before 5 Whys narrows one cause.
- When a problem has many possible causes and the team keeps arguing about which one matters.
- In a kaizen event or an 8D team meeting, to get every idea on the wall in ten minutes.
- For recurring defects, downtime or safety events where the first fix did not hold.
What is on the board
- 1
Problem statement (the head)
One measured problem, for example scrap on Line 2 up from 1.8% to 4.1% since March.
- 2
Man
Training, staffing, handover, fatigue.
- 3
Machine
Equipment, tooling, settings, wear.
- 4
Method
The procedure, the standard, the sequence.
- 5
Material
Raw material, components, supplier lots, storage.
- 6
Measurement
Gauges, inspection method, how the data is collected.
- 7
Mother nature
Temperature, humidity, lighting, layout.
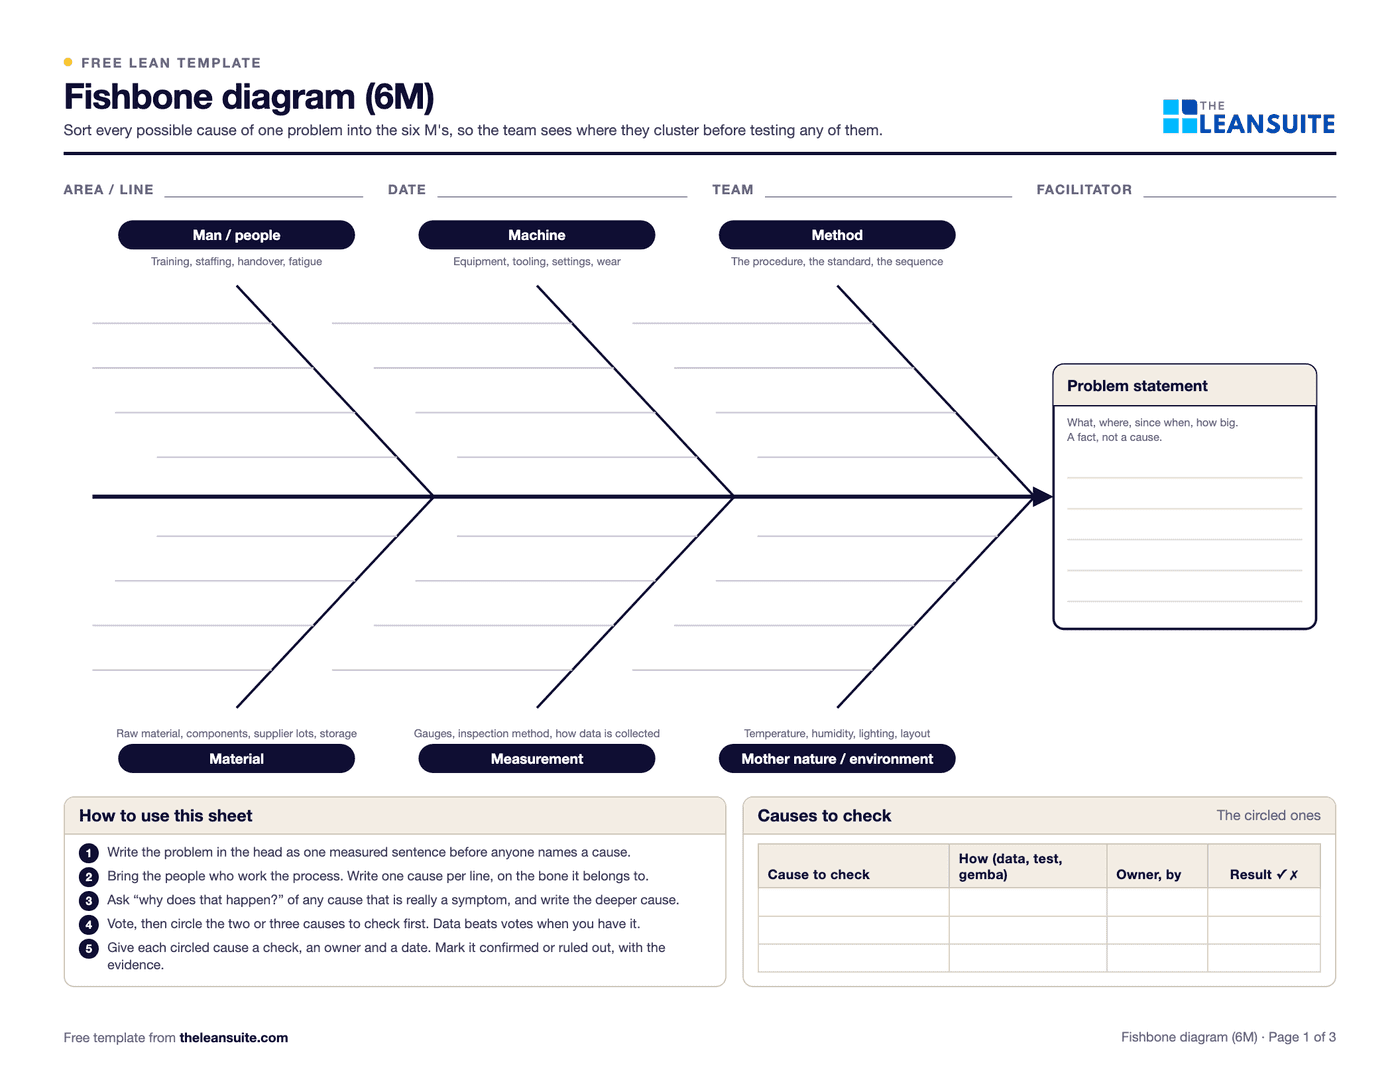 A problem statement box at the head, six bones labeled man, machine, method, material, measurement and mother nature with blank lines for causes, a how-to-use strip and a table for the causes to check.
Free template
Free fishbone diagram template: printable PDF and Excel cause list
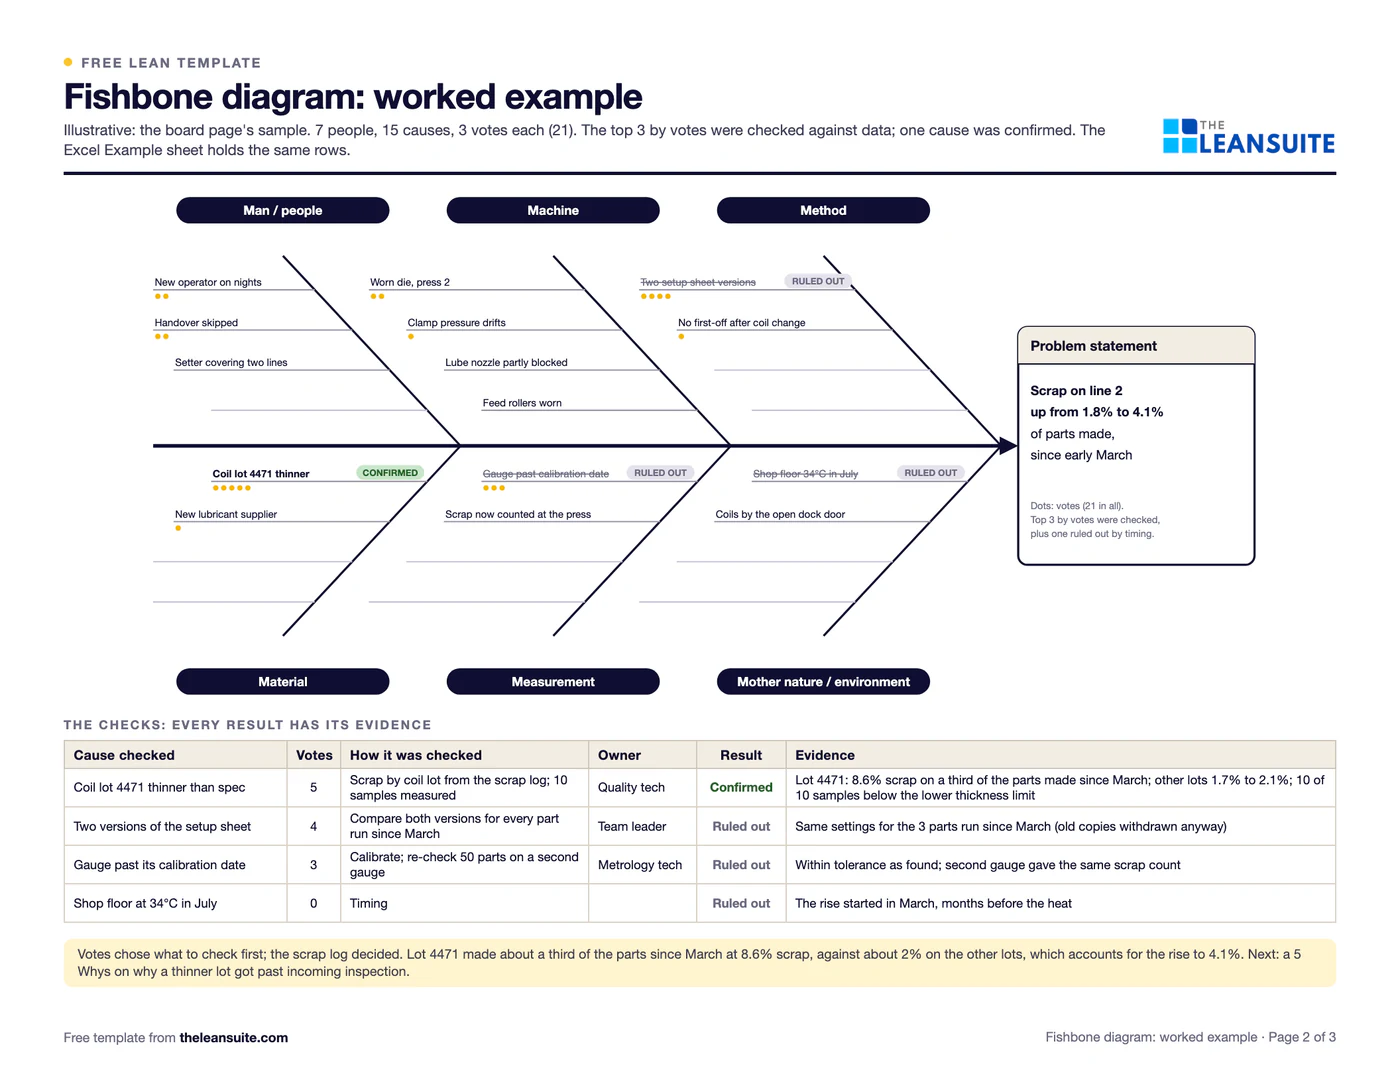
The same six-M fishbone on a landscape sheet for a session on paper, with a table for the causes you will check. Page 2 is this board's sample filled in: 15 causes, 21 votes, the top 3 checked against the scrap log and one confirmed. Page 3 covers how to pick and check causes, five traps and the source. The Excel cause list ranks the votes, picks the top causes to check, flags empty bones and causes marked confirmed with no evidence, and totals each bone.
Free to use: print it, copy it and edit it for your team. Enter your name and work email once to download.
How to fill in the template
- 1Write the problem in the head as one measured sentence: what, where, how much and since when. The sample reads: scrap on line 2, up from 1.8% to 4.1% of parts made, since early March.
- 2Fill the bones in a short, silent round, one cause per line, then read each bone aloud and move any cause that sits on the wrong bone. Rename a bone if your process needs another heading.
- 3Give everyone three votes and mark them as dots beside the causes they think most likely. Seven people make 21 dots.
- 4Copy the causes and votes into the Excel cause list. It ranks them and marks the top three, or the number you set, as the causes to check.
- 5Give each cause to check a method, an owner and a date. The sheet flags a check that is past its date.
- 6Write the result as confirmed or ruled out, with the evidence. The sheet flags a cause marked confirmed with no evidence and any bone left empty.
Running it
How to run a Fishbone (Ishikawa) session
- 1
Write the problem as one measured sentence and put it in the head before anyone names a cause. If the team cannot agree on the sentence, it is not ready for a fishbone.
- 2
Bring the people who touch the process: an operator from each shift, the setter, maintenance, quality. Five to eight people, typically an hour; a manager in the room should ask questions, not fill bones.
- 3
Brainstorm in silence for five minutes, one cause per sticky, then place the stickies on the bones. Ask 'why does that happen?' of any sticky that is really a symptom.
- 4
Read each bone aloud and move the stickies the team disagrees with. Merge duplicates rather than deleting them: two people naming the same cause is information.
- 5
Pick the two or three causes to test, by data if you have it, by dot vote if you do not, and mark them with a different sticky colour.
- 6
Give each chosen cause a person and a date to check it on the floor: measure it, watch it, pull the record. The fishbone ends when the causes to test have names against them.
- 7
Good output: 15 to 30 causes, every bone with something on it, three causes marked, three owners, and a date for the 5 Whys or the test.
Worked example · sample data
Worked example
The sample board has 'Scrap on Line 2 up to 4.1%' at the head. Under Man the team put a new operator on nights and a skipped handover; under Machine, a worn die on press 2 and clamp pressure that drifts; under Method, two versions of the setup sheet; under Material, coil lot 4471 running thinner than spec; under Measurement, a gauge past its calibration date; under Mother nature, a shop floor at 34°C in July. Seven people voted and checked the top three against the scrap log. Lot 4471 ran at 8.6% scrap against about 2% on the other lots: confirmed. The gauge was within tolerance and both setup sheets held the same settings: ruled out. The heat was ruled out by timing, since the rise began in March. The team booked a 5 Whys on how a thin lot passed incoming inspection.
The board shown at the top of this page, read through. Invented data, not a customer.
15 causes, 21 votes, bone by bone
Man4 votes
- New operator on nights2 votes
- Handover skipped between shifts2 votes
- Setter covering two linesno votes
Machine3 votes
- Worn die on press 22 votes
- Clamp pressure drifts1 vote
- Die lubrication nozzle partly blockedno votes
- Press 2 feed rollers wornno votes
Method5 votes
- Two versions of the setup sheet in circulation4 votesRuled outBoth versions hold the same settings for the 3 parts run since March
- No first-off check after a coil change1 vote
Material6 votes
- Coil lot 4471 thinner than spec5 votesConfirmed8.6% scrap on lot 4471 against 1.7% to 2.1% on the other lots; 10 of 10 samples below the thickness limit
- New lubricant supplier since February1 vote
Measurement3 votes
- Gauge past its calibration date3 votesRuled outWithin tolerance as found; a second gauge gave the same scrap count
- Scrap now counted at the press, not at final inspectionno votes
Mother natureno votes
- Shop floor at 34°C in Julyno votesRuled outThe rise started in March, months before the heat
- Coils stored next to the open dock doorno votes
one voteStruck through: checked and ruled out.
Man, 4 votes: New operator on nights (2 votes); Handover skipped between shifts (2 votes); Setter covering two lines (no votes). Machine, 3 votes: Worn die on press 2 (2 votes); Clamp pressure drifts (1 vote); Die lubrication nozzle partly blocked (no votes); Press 2 feed rollers worn (no votes). Method, 5 votes: Two versions of the setup sheet in circulation (4 votes, ruled out); No first-off check after a coil change (1 vote). Material, 6 votes: Coil lot 4471 thinner than spec (5 votes, confirmed); New lubricant supplier since February (1 vote). Measurement, 3 votes: Gauge past its calibration date (3 votes, ruled out); Scrap now counted at the press, not at final inspection (no votes). Mother nature, no votes: Shop floor at 34°C in July (no votes, ruled out); Coils stored next to the open dock door (no votes). The top 3 by votes were Coil lot 4471 thinner than spec, Two versions of the setup sheet in circulation, Gauge past its calibration date.
Common mistakes
- A vague head. 'Quality problems on Line 2' produces a fishbone nobody can test; a number and a date do.
- Filling the bones from the meeting room. Walk the line first, or bring the people who work it.
- Treating the fishbone as the analysis. It lists candidates; the root cause still has to be proven on the floor.
- Letting one loud voice decide which cause is right before the board is full.
- Leaving a bone empty and moving on. An empty bone usually means nobody in the room knows that part of the process.
- Never coming back. Update the board when a tested cause is ruled out, so the team does not test it twice.
How it works in Lean Studio
- 1Start from the Fishbone (Ishikawa) template and type the problem into the head.
- 2Add a sticky per candidate cause and drop it on its bone; drag it to another bone when the team changes its mind.
- 3Mark the causes to test next with a different sticky colour, then take them to a 5 Whys board.
- 4Save the finished board to My templates so the next team starts from your version.
Lean Studio boards are drawn with stickies, text, shapes (rectangle, rounded rectangle, ellipse, diamond), arrows and charts, and any board can carry the 15 data widgets, from a scorecard to a kanban. See all widgets and boards.
Also in LeanSuite
Where it goes next in LeanSuite
LeanSuite's RCA Agent drafts 5 Whys, 4M1D and fishbone analyses from a problem and its attached documents.
The causes to test become actions with owners and due dates in a Kaizen project, which has a fishbone section of its own alongside 5 Whys, 5W1H and 4M1D. Kaizen & Projects
If the problem was raised as a tag on the floor, a recurring tag can be escalated into a Kaizen or A3 project in one click, with its history. Daily Issue Management
The RCA Agent drafts a fishbone from the problem description and attached SOPs or manuals, for the team to edit. AI Root Cause Analysis
Open this board in LeanSuite
Fishbone (Ishikawa) is one of the 30 ready-made boards in Lean Studio, LeanSuite's whiteboard. Try the interactive demo in your browser with sample data, or pilot LeanSuite on your own lines for 90 days, with the setup done by our team.
What Lean Studio isRelated boards and templates
- Fishbone diagram guide: what it is, the categories, six steps and how to read one
- Free fishbone diagram maker: draw it online, download a PNG or SVG
- Root cause analysis: the method guide
- The 6 Ms of production (guide)
- Fishbone diagram examples: five worked problems, from diagram to action
- Best root cause analysis software (buyer's guide)
- 5W1H templatePDF
- 5 Whys templatePDF
- 3C Problem Board
- A3 problem solving templatePDF
- 8D report templatePDF
- Poka-yoke worksheetPDF
In the lean glossary
FAQ
Fishbone (Ishikawa) board: common questions
This one comes as a PDF to print and an Excel file. The Excel file is a cause list rather than a drawing: it ranks the votes, marks the causes to check and tracks each one to confirmed or ruled out. For a drawn diagram to paste into a Word report or a slide, type the causes into the free fishbone diagram maker and download it as a PNG or SVG.
Man (people), machine, method, material, measurement and mother nature (environment). Some plants add management and maintenance to make eight. Office and service teams often use the four P's instead: policies, procedures, people and plant. Pick categories that cover the whole process and keep to six or so, or the diagram turns into a list.
Fishbone first. It spreads the possible causes wide, then 5 Whys drills one of them down to a root cause. Doing 5 Whys first tends to chase the first cause somebody names.
Use it to list the suspects, then prove one. Vote or use data to pick the two or three causes to check, then split the defect data by each one (lot, shift, machine), check the cause started when the problem did, and where you can, put it back and take it away. Mark each cause confirmed or ruled out and write the evidence. Run 5 Whys on the confirmed cause.
As many as the team can name in a short, timed session, usually 15 to 30. Then vote or use data to pick the two or three worth testing. A bone with nothing on it is a prompt to think harder, not a finding.
Yes. Lean Studio is a shared whiteboard, so people add stickies from their own screens and the board updates for everyone. Teams without LeanSuite can share the Excel cause list instead.
More problem solving boards
All 30 Lean Studio boards- 5 WhysDrill from a symptom to its root cause in five steps.
- PDCA CycleContinuous improvement cycle for iterating on a change through Plan, Do, Check, Act.
- A3 Problem SolvingSingle-page structured problem-solving report following the Toyota A3 method.
- DMAIC StoryboardGuide an improvement project through Define–Measure–Analyze–Improve–Control.
- 8D ReportWork a structured 8D problem-solving report from team formation through closure.
- 3C Problem BoardTrack Concern, Cause and Countermeasure with clear ownership.