Free tool
OEE calculator
Overall equipment effectiveness (OEE) measures how much of a machine's planned production time is truly productive. It is availability × performance × quality: the share of planned time the machine runs, how fast it runs against its ideal rate, and the share of parts that are good.
OEEequalsAvailability × Performance × Quality
AvailabilityequalsRun time divided by Planned production time
PerformanceequalsIdeal cycle time × Total count divided by Run time
QualityequalsGood count divided by Total count
Breaks, meetings, no orders
Breakdowns, changeovers, waiting
Fastest possible time for one unit
Good and bad units
Scrapped or reworked
Pre-filled with the worked example. Replace the numbers with your own shift; results update as you type.
OEE
72.9%
486 good units in 400 minutes of planned production time.
Availability
90.0%
360 of 400 min running
Performance
90.0%
Actual speed vs ideal
Quality
90.0%
486 of 540 good
How to calculate it
Six numbers from one shift
Shift length and planned stops give planned production time, the time the machine was meant to run. Breaks and meetings are not losses, so they are taken out first.
Unplanned downtime is every minute the machine should have run but did not: breakdowns, changeovers, waiting for material. It sets availability.
Ideal cycle time and total count set performance: how many units the run time could have made at full speed, against how many were made.
Rejects set quality. Count anything scrapped or reworked, since a reworked part was not good the first time.
Each factor points at a different kind of loss. The six big losses sort them into equipment failures and setups (availability), minor stops and slow running (performance), and defects and startup losses (quality).
Worked example
Illustrative numbers, not a benchmarkA 450-minute shift with 50 minutes of planned breaks, 40 minutes of unplanned downtime, an ideal cycle time of 36 seconds, 540 units made and 54 rejected.
- 1Planned production time = 450 − 50 = 400 min. Run time = 400 − 40 = 360 min.
- 2Availability = 360 ÷ 400 = 90%.
- 3Performance = (36 s × 540) ÷ (360 min × 60) = 19,440 ÷ 21,600 = 90%.
- 4Quality = (540 − 54) ÷ 540 = 486 ÷ 540 = 90%.
A note on the 85% “world-class” figure
The 85% OEE figure often called world-class is usually attributed to Seiichi Nakajima, who set out Total Productive Maintenance in Introduction to TPM (Productivity Press, 1988). Treat it as a reference point, not a target for every process: the Wikipedia article on OEE lists situations where it does not fit. Your own line's OEE, tracked shift by shift, is the comparison that shows whether improvements are working.
Embed this calculator
Teaching this, or writing about it? Paste this code into your site, course page or intranet and the calculator works right there. It is free, with no sign-up.
<iframe src="https://www.theleansuite.com/tools/oee-calculator/embed" title="OEE calculator by LeanSuite" width="100%" height="1000" style="border:0;max-width:1000px" loading="lazy" allow="clipboard-write"></iframe>
<p style="font:13px/1.4 sans-serif"><a href="https://www.theleansuite.com/tools/oee-calculator">OEE calculator</a> by LeanSuite</p>How LeanSuite helps
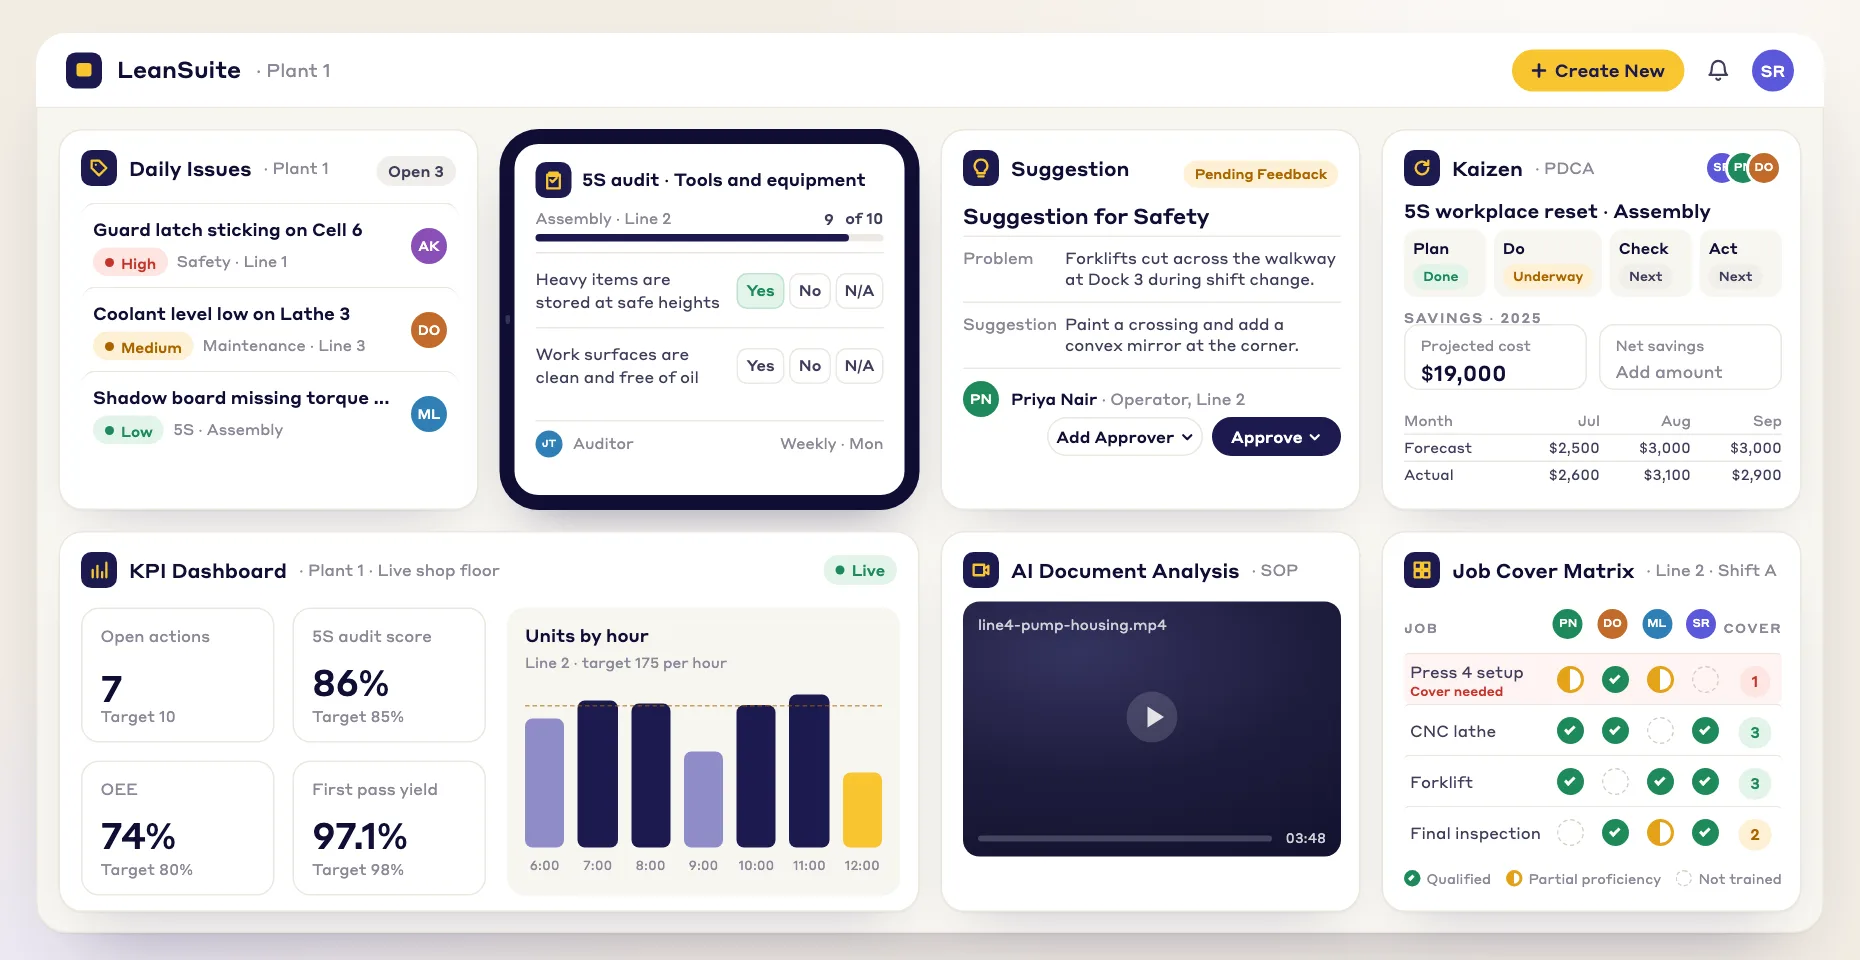
LeanSuite's KPI Dashboards track OEE, downtime and production counts live, so you can clear bottlenecks early and keep production on schedule.
See KPI DashboardsFAQ
OEE calculator: common questions
More free lean tools
All tools- Downtime cost calculatorWhat an hour, an event and a year of unplanned downtime cost, from lost output, idle labour, scrap and overtime.
- SMED changeover calculatorTime saved by moving changeover steps from internal to external, capacity freed per week and the smaller batch it allows.
- Takt time calculatorThe pace a line must hit to meet customer demand, from shift time, breaks and daily demand.
- Cycle time calculatorCycle time against takt, units per hour, capacity per shift and the gap to daily demand.
- Line balancing calculatorLine efficiency, balance delay and the minimum number of stations from station times and takt.
- First pass yield (FPY) calculatorFirst pass yield at each step and rolled throughput yield (RTY) across the whole process.
- Cost of poor quality (COPQ) calculatorTotal COPQ and cost of quality, and each as a share of revenue, from the four quality cost categories.
- Process capability (Cp, Cpk) calculatorCp and Cpk against your specification limits, plus Pp and Ppk from pasted measurements, with a distribution chart.
- MTBF and MTTR calculatorMean time between failures, mean time to repair and availability from operating time, failures and repair time.
- Lead time calculatorManufacturing lead time from WIP and throughput (Little's Law), and the share of it that adds value.
- Manufacturing ROI calculatorAnswer a few questions about your shop floor, shifts and downtime to estimate your potential ROI with LeanSuite.