

Free training deck
Updated · About 45 minutes
SPC and Cpk training presentation
Statistical process control (SPC) is the use of control charts and capability indices to watch a process, tell normal variation from a real change, and judge whether the process can hold the specification. This free deck teaches it to operators, technicians and engineers in about 45 minutes. Its 19 editable slides cover common and special cause variation, which chart to use, how to build an X-bar and R chart, the control chart constants, one worked example of the limits, how to read the signals, control limits against specification limits, Cp and Cpk with the same example worked through, what a Cpk value means, the common mistakes, a 15-minute chart-building activity and four check questions with answers. Every slide has speaker notes.
Free to use: print it, copy it and edit it for your team. Enter your name and work email once to download.
 The title SPC and Cpk, reading a control chart, on a navy background with the LeanSuite logo.
A look inside
What is in the 19 slides
For operators, technicians, quality technicians, process and quality engineers, supervisors. Widescreen, in plain language, with speaker notes on every slide.
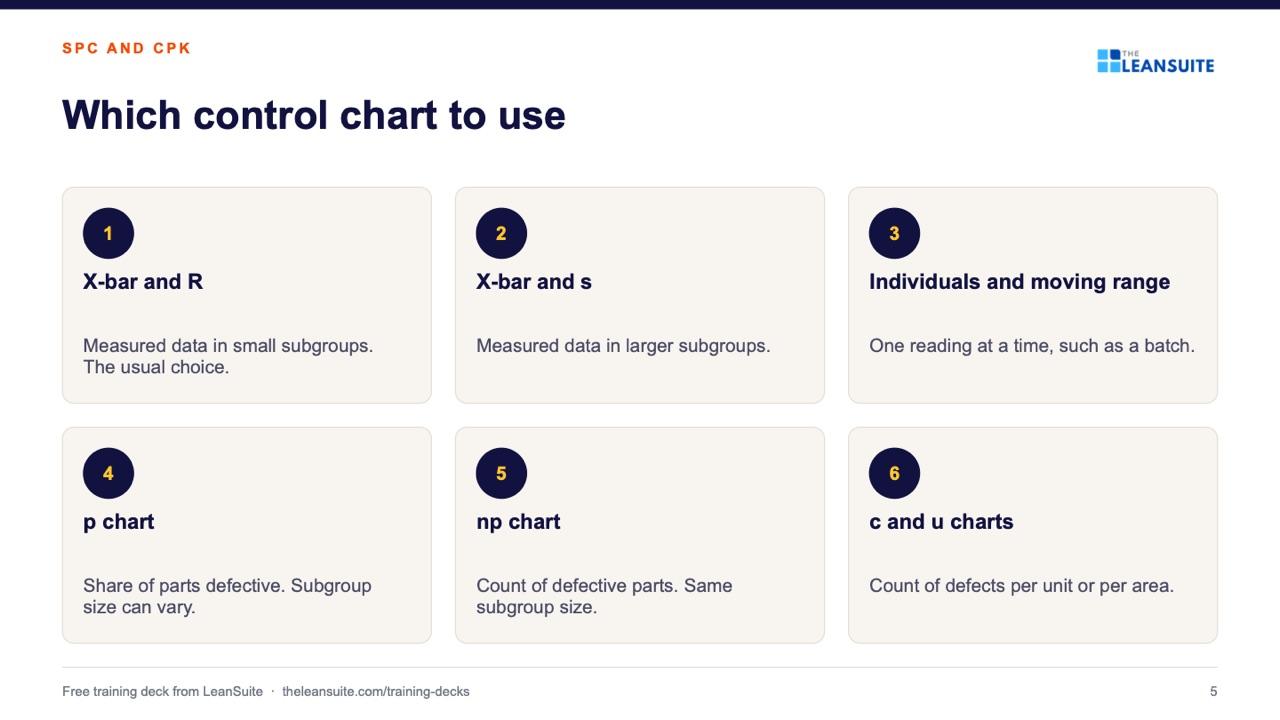
Slide 5: Which control chart to use 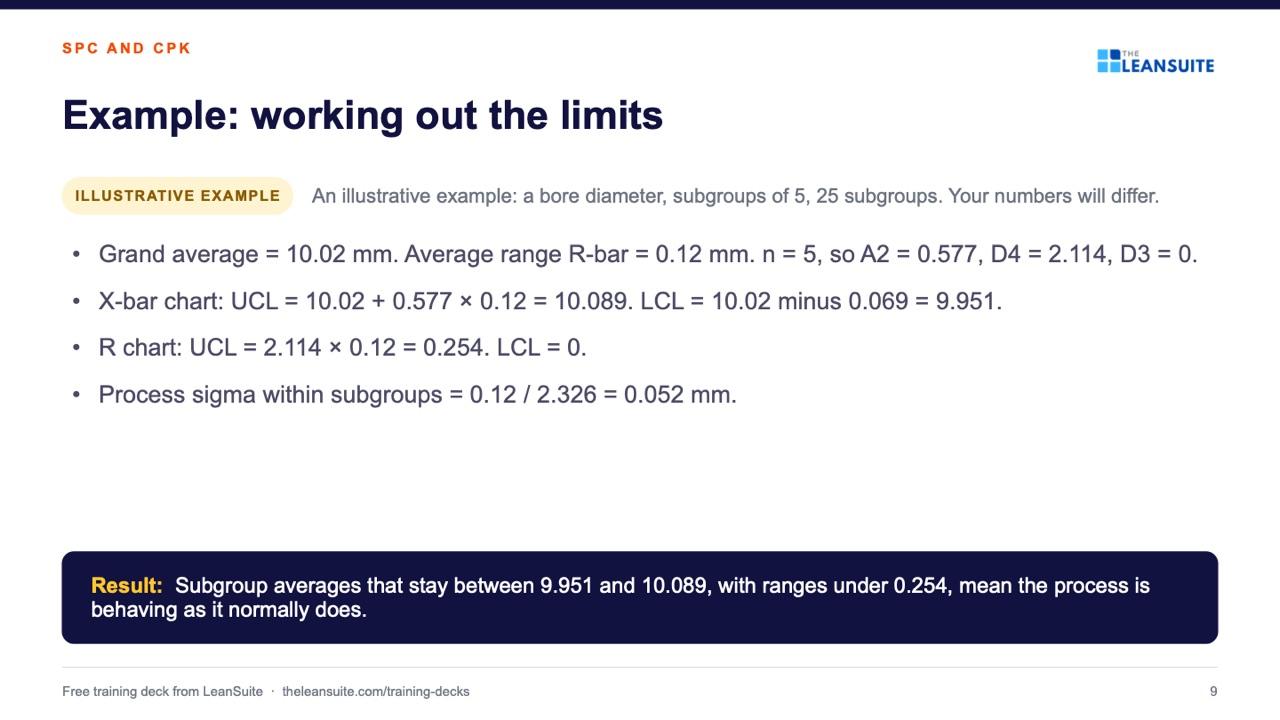
Slide 9: Example: working out the limits 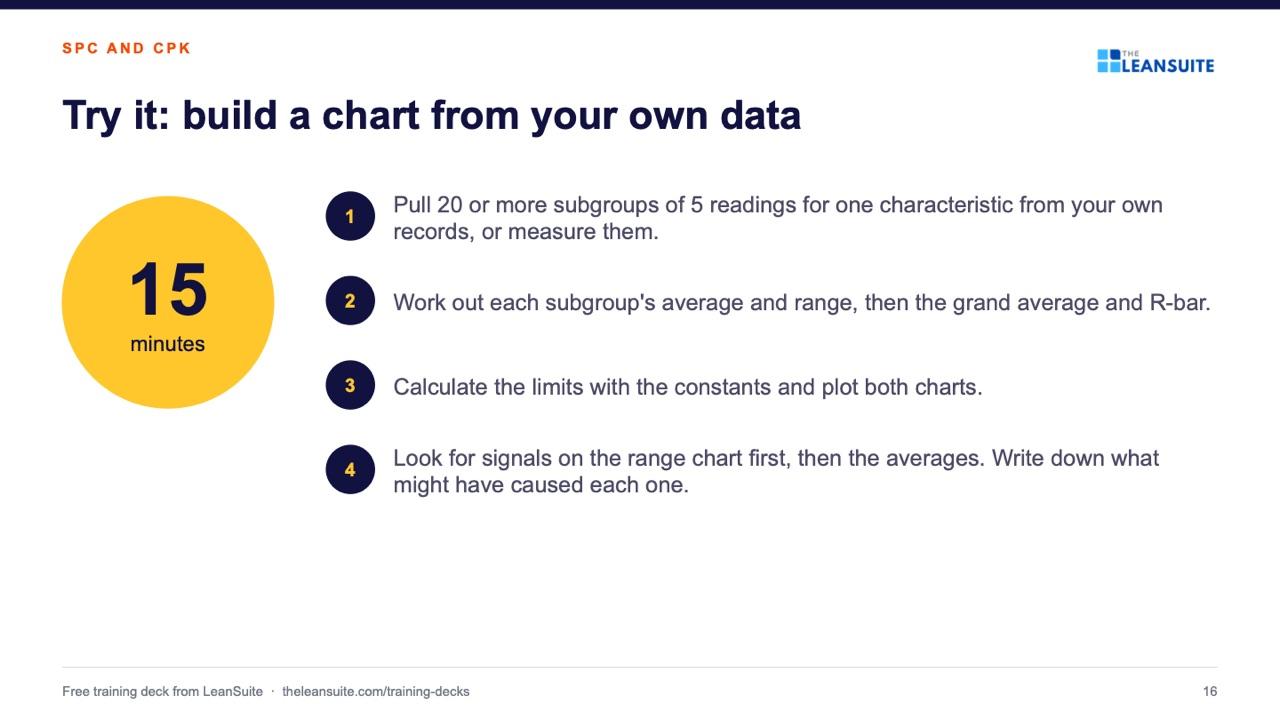
Slide 16: Try it: build a chart from your own data
- 1SPC and Cpk: reading a control chartCover
- 2AgendaVariation, and what SPC is for · Choosing a chart and building an X-bar and R chart · Reading the signals · Control limits, specifications, Cp and Cpk · Mistakes, activity and check questions
- 3What SPC is forSPC uses data from the process itself to tell a real change from normal wobble.
- 4Common cause and special cause variationThe whole method rests on this split.
- 5Which control chart to useX-bar and R, X-bar and s, Individuals and moving range, p chart, np chart, c and u charts
- 6Building an X-bar and R chartPick a characteristic that matters, one that is measured with a gauge you trust.
- 7The limit formulasConstants come from a table and depend only on the subgroup size, n.
- 8Control chart constantsStandard values for X-bar and R charts. Check them against your own reference table.
- 9Example: working out the limitsAn illustrative example: a bore diameter, subgroups of 5, 25 subgroups. Your numbers will differ.
- 10Reading the signalsCheck the range chart first, then the averages.
- 11Control limits are not specification limitsThey answer different questions and come from different places.
- 12Capability: Cp and CpkCapability asks whether a stable process fits inside the specification.
- 13Example: Cp and Cpk worked outSame illustrative bore: specification 10.00 plus or minus 0.15 mm, so LSL 9.85 and USL 10.15.
- 14What a Cpk value tells youCpk of 1.00 means the nearer spec limit is 3 sigma from the average.
- 15Common mistakesCalculating Cpk on a process that is out of control.
- 16Try it: build a chart from your own dataA 15-minute team activity
- 17Check your understanding4 check questions
- 18AnswersThe answers, to discuss
- 19Key points and next stepsNext: build one chart for one characteristic in your own area.
The 45-minute session, slide by slide
- Slides, about: 30 minutes
- Activity (slide 16): 15 minutes
Present · 15 slides
- 1SPC and Cpk: reading a control chart
- 2Agenda
- 3What SPC is for
- 4Common cause and special cause variation
- 5Which control chart to use
- 6Building an X-bar and R chart
- 7The limit formulas
- 8Control chart constants
- 9Example: working out the limits
- 10Reading the signals
- 11Control limits are not specification limits
- 12Capability: Cp and Cpk
- 13Example: Cp and Cpk worked out
- 14What a Cpk value tells you
- 15Common mistakes
Do the activity · 1 slide
- 16Try it: build a chart from your own data
Check and follow up · 3 slides
- 17Check your understanding
- 18Answers
- 19Key points and next steps
About 30 minutes of slides and 15 minutes of activity. Present: slides 1 to 15 (SPC and Cpk: reading a control chart; Agenda; What SPC is for; Common cause and special cause variation; Which control chart to use; Building an X-bar and R chart; The limit formulas; Control chart constants; Example: working out the limits; Reading the signals; Control limits are not specification limits; Capability: Cp and Cpk; Example: Cp and Cpk worked out; What a Cpk value tells you; Common mistakes). Do the activity: slide 16 (Try it: build a chart from your own data). Check and follow up: slides 17 to 19 (Check your understanding; Answers; Key points and next steps).
How to run it
Running the session
- 1
Prepare
Read the speaker notes once and swap the illustrative example for one from your own area if you have it. Print the PDF if people like a handout.
- 2
Present
The slides take about 30 minutes. Every slide has notes, so you can talk from them rather than read the slide.
- 3
Do the activity
Pull 20 or more subgroups of 5 readings for one characteristic from your own records, or measure them. The activity slide takes the team through it step by step; allow 15 minutes.
- 4
Check and follow up
Ask the check questions before showing the answers, then agree one next step with an owner and a date before people leave.
The check questions
- 1. What is the difference between common cause and special cause variation?
- Common cause is built into the process and shows up inside the control limits. Special cause is a specific change that shows up as a signal on the chart.
- 2. Why are control limits not the same as specification limits?
- Control limits are calculated from the process's own data and describe how it behaves. Specification limits come from the customer or design and describe what is needed.
- 3. A process has Cp of 1.50 and Cpk of 0.90. What does that tell you?
- The spread would fit the specification but the process is badly off center. Centering it is the first thing to try.
- 4. Which should you read first on an X-bar and R chart?
- The range chart. If the spread is not stable, the averages cannot be trusted.
Templates and guides to go with it
- X-bar and R control chart template25 subgroups with means and ranges, control limits from A2, D3 and D4, signal flags, both charts and a reaction log.
- Process capability (Cpk) study sheet25 subgroups of readings with Cp, Cpk, Pp and Ppk worked out, control limits to check stability, and a histogram.
- Attribute control chart template (p, np, c and u charts)p, np, c and u charts in one workbook: a chart selector, a sample size check, limits for each subgroup, signal flags and four worked examples.
- Topic: Quality managementEvery guide we have on the subject, sorted.
Read more
After the session
Put it on the wall
Free printable poster on the same subject, so the team sees it every day: a PNG to download now, and print-ready PDFs from Letter to 24 x 36 in.
FAQ
SPC and Cpk training presentation: common questions
Statistical process control. It uses control charts and statistics on data from the process to tell normal variation from real change, so people act when they should and leave the process alone when they should.
About 45 minutes: roughly 30 minutes of slides, a 15-minute chart-building activity and the check questions.
Cp compares the width of the specification with the width of the process spread and ignores centering. Cpk also looks at how close the process average is to the nearer specification limit, so it is never larger than Cp.
The method follows the AIAG Statistical Process Control reference manual, second edition, and the control chart constants are the standard published values. Your customer's requirements and your control plan set the sample sizes and acceptance values, and they take priority.
Yes. The PowerPoint file is fully editable, including the speaker notes. Many teams replace the illustrative bore example with a characteristic from their own plant.
More free training decks
- 5S training presentationSort, set in order, shine, standardize and sustain in 16 slides, with a 15-minute sort activity and a quiz.View deck
- Kaizen training presentationWhat kaizen is, its principles, PDCA and four steps to a first improvement in 17 slides, with an activity and a quiz.View deck
- Autonomous maintenance training presentation: the 7 stepsThe 7 steps of jishu hozen, who does what and how step audits work, in 19 slides with notes and a quiz.View deck
- 8 wastes of lean training presentationValue vs waste, the 8 wastes (TIMWOODS) with examples, muda, mura and muri and a waste walk, in 17 slides.View deck
- Gemba walk training presentationGo see, ask why, show respect: how to plan, run and follow up a gemba walk, in 16 slides with a practice walk.View deck
- Root cause analysis training presentation: 5 whys and fishboneDefine, contain, the 5 whys, the fishbone diagram and verifying the cause, in 18 slides with a team activity.View deck
- TPM training presentation: the 8 pillarsWhat TPM is, the six big losses, OEE and the 8 pillars, in 19 slides with a loss-spotting activity.View deck
- Manufacturing excellence pillars training presentationThe 20 pillars, cost deployment, the 7-step approach, model areas and audits, in 17 slides.View deck
- Obeya room training presentationWhat an obeya is, what goes on its walls and how to run the meetings, in 15 slides with a design activity.View deck
- DMAIC training presentationDefine, measure, analyze, improve and control, with the main tools of each phase, in 16 slides.View deck
- SMED training presentationInternal and external setup, the four SMED stages and how to halve a changeover, in 16 slides.View deck
- FMEA training presentationDFMEA and PFMEA, severity, occurrence and detection, RPN and action priority, in 16 slides.View deck
- Kanban training presentationPull instead of push: how a kanban loop works, the card types, the rules and how to size it, in 16 slides.View deck
- Lockout tagout (LOTO) training presentationHazardous energy, lockout versus tagout and the six steps in order, with a walk-round activity, in 17 slides.View deck
- Quality management system (QMS) training presentationWhat a quality management system is, the ISO 9001 clauses, procedures and records, corrective action and audits, in 18 slides.View deck
- MSA and Gage R&R training presentationThe five measurement properties, how a gage R&R study works, %GRR and ndc with worked numbers, and attribute gauges, in 19 slides.View deck
- PPAP and APQP training presentationThe five APQP phases, gates, the 18 PPAP elements, the five submission levels and the capability criteria, in 19 slides.View deck
- OEE training presentationHow to calculate OEE and read the six big losses in 19 slides, with one worked shift, a 20-minute exercise and a quiz.View deck
- Leader standard work training presentationWhat leader standard work is, the routine at each level, five steps to build it and how to keep it going, in 19 slides with an exercise and a quiz.View deck
- Daily management and tier meetings training presentationTier meetings, boards, huddles and escalation in 19 slides, with a worked example, a 20-minute huddle exercise and a quiz.View deck
- 5 Whys training presentationOhno's machine example, how to ask good whys, when to stop and where the method falls short, in 20 slides with a team exercise.View deck
- A3 problem solving training presentationThe seven boxes, the three kinds of A3, how to write and coach one, with two worked example slides and a 30-minute exercise, in 20 slides.View deck
- Poka-yoke (mistake-proofing) training presentationMistakes versus defects, the contact, fixed-value and motion-step methods, control and warning devices and how to design and test one, in 18 slides.View deck
- Layered process audit (LPA) training presentationWhat a layered process audit is, the layers, how to write and ask good questions, handle a no and read the results, in 19 slides.View deck
- Standard work training presentationTakt time, work sequence and standard WIP, how to write a standard with the operators and how to keep it alive, in 18 slides.View deck
- Value stream mapping (VSM) training presentationHow to map the current state, read lead time, design the future state with the eight questions and turn it into a plan, in 19 slides.View deck
- TWI job instruction training presentationThe four steps of TWI job instruction and the job breakdown sheet, from the original wartime card, with a worked example and a practice session.View deck
- 8D problem solving training presentationD0 to D8, containment, the root cause and the escape point, proving a fix and preventing repeats, in 20 slides with a team exercise.View deck
- Forklift safety training presentationOperator training rules, stability and load center, travel and dock rules and the daily exam, each tied to 29 CFR 1910.178, in 20 slides.View deck
- Hazard communication (HazCom, GHS) training presentationLabels, the eight GHS pictograms, the 16 SDS sections, employee training and the 2026 and 2028 dates, each tied to 29 CFR 1910.1200, in 20 slides.View deck
- New-hire safety orientation training presentationA day-one safety orientation for plants and warehouses: reporting, emergencies, PPE, chemicals, machines and trucks, with the OSHA paragraph behind each, in 17 slides.View deck
- 4M change management training presentationMan, machine, material and method changes, rating the risk, extra checks, the change point board and closing a change, in 19 slides.View deck
Training is the start. Keeping it going is the hard part.
See how plants run their audits, improvements and follow-ups in LeanSuite, on a call built around your own problem.
Book a 45-minute demo