

Lean playbook · Food and beverage
Lean playbook for food and beverage plants
Short answer
Start lean in a food or beverage plant on one line, with the losses you can count: changeover time, short stops on filling and packaging, giveaway on fill weights and quality holds. SMED shortens allergen and product changeovers, a daily operator care routine and short-stop tally lift OEE, control charts cut giveaway, and job instruction gets seasonal operators to standard. Any change to cleaning, sanitation or allergen steps goes through your food safety team first.
Last updated:
7 problems on the floor, and the lean methods for each
Each problem says what it looks like, which methods address it, the first moves to make and the number to watch. Pick the one or two that cost your plant most; you do not need all of them at once.
Where a food or beverage filling and packaging line loses time and quality
Capping and labelling
Case packing
Hold and ship
Across the whole line
Long allergen and product changeovers
The line stands still for the clean-down, line clearance and sign-off between products, and the time depends on which crew is on. Parts, cleaning kits and the next run's packaging are often fetched after the line has stopped.
In LeanSuite
Run each changeover as a visual checklist in Lean Creator and require a photo on the steps that matter most.
First moves
- Film one changeover and list every step, marking which ones need the line stopped.
- Stage cleaning kits, change parts and the next run's materials before the current run ends.
- Put the line clearance and allergen sign-off on a checklist, with a photo of the cleared line, so it is done the same way on every shift.
- Agree the new sequence with the food safety team, then write it down as the standard.
Number to watch: Changeover time, from the last good unit of one run to the first good unit of the next.
Sanitation and pre-op checks that vary by crew
Sanitation and pre-operational checks happen every shift, often at night and by different people. A tick on a paper sheet cannot show whether a check was done properly, on time or at all.
In LeanSuite
Schedule sanitation, pre-op and equipment care checklists every shift, weekly or after a changeover, with pictures and videos for each step.
First moves
- Write a one-page standard for each piece of equipment: what to clean, inspect and check, with a photo of the clean condition.
- Make the pre-op check a signed step before start-up, with the line lead's sign-off.
- Audit a sample of completed checks each week against the standard, on the floor.
Number to watch: Pre-op and sanitation checks completed on time and passed first time.
Short stops on filling and packaging lines
Fillers, cappers, labellers and case packers stop for a few seconds or minutes at a time for jams, misfeeds and sensor faults. Each stop is too short for the downtime log, but together they decide the line's output.
In LeanSuite
Operators log each minor stop as it happens, with category, duration and contributing factor.
First moves
- Tally every short stop by cause for one week on the machine that sets the line's pace.
- Pick the top one or two causes and fix them with the operators and a technician.
- Add a daily clean, inspect, lubricate and retighten routine for that machine.
- Work out OEE every shift from the same data, so the gain shows.
Number to watch: OEE and short stops per shift on the pacing machine.
Giveaway on fill weights
To stay safely above the declared weight, fill targets are set high and adjusted by feel. Every gram above the target is product given away, and one drifting filler head can force the whole target up.
In LeanSuite
Control charts handle giveaway, and no LeanSuite page covers them yet. Chart fill weights by head on the free template on this card.
What LeanSuite tracks around it
LeanSuite's KPI dashboards for manufacturing track every KPI against its target, with RAG ranges, KPI trees and live huddle boards, so operators and the plant manager act on the same numbers.
First moves
- Chart fill weights by head or lane on a control chart and find the heads that drift.
- Fix the drifting heads before touching the target.
- Study capability once the process is stable, and only then lower the target, within your legal and customer requirements for net content.
Number to watch: Average overfill against the target, and Cpk for fill weight.
Quality holds and repeat defects
A seal failure, a wrong label or date code or a foreign-material find means holding product, sorting it and finding the cause. When that lives in email, the same defects come back on the next shift.
In LeanSuite
Each non-conformance is captured with photos and routed to quality and engineering.
First moves
- Agree a containment routine (stop, hold, sort, count) that runs before anyone looks for the cause.
- Check label and date code at start-up and after every label change, against a reference.
- Run a 5 Whys with the people on the line for any defect that returns, and record the action in one log.
- Where you can, change the equipment or the part so the error cannot happen, instead of adding a check.
Number to watch: Holds per month and first pass yield.
Training seasonal and new operators
Peaks bring a stream of new and temporary operators who must learn hygiene rules and line procedures fast. Shadowing takes experienced people off the line and teaches each new hire a slightly different method.
In LeanSuite
Film the job once and LeanSuite drafts the work instruction with numbered steps, photos and safety notes.
First moves
- Write job breakdown sheets for the tasks where mistakes cost most: allergen steps, start-up checks, label changes.
- Train with the four-step job instruction method and sign each person off before they work alone.
- Keep a skills matrix per line so supervisors see who is cleared for which position.
Number to watch: Positions covered by at least two signed-off people on every shift.
Audit evidence spread across binders
Customer, certification and internal audits ask for proof that each check was done, by whom and when, and that every finding was closed. Pulling that from binders takes days, and open findings are easy to lose.
In LeanSuite
Build your own GMP inspections and HACCP verification checks in Lean Creator and complete them on a phone or tablet with photos.
First moves
- Keep every check and audit record for a line in one place, with dates and names.
- Turn every failed item into an action with an owner and a due date, in one log.
- Run short internal audits of the critical steps each week, so the formal audit finds nothing new.
Number to watch: Overdue actions from audits and checks.
More small fixes in the production, quality and maintenance sections of the kaizen idea bank.
A 90-day starting plan
One line or product family, two problems, measured before and after. The point of the first 90 days is a result the plant believes and a method it can repeat, not a plant-wide program.
The 90 days, with the gate that ends each stage
- Days 1 to 30See the losses on one lineDone when: You have baseline numbers on the board and two problems with an owner each.
- Days 31 to 60Fix the top two lossesDone when: Each fix has a written standard and a before-and-after number.
- Days 61 to 90Make it stick, then spread itDone when: The gains have held for a month and the next line has its baseline.
Days 1 to 30
See the losses on one line
Pick one line and get a true baseline before changing anything.
- Choose the line with the most changeovers or the most lost time, and name a line lead and a sponsor.
- Measure for two weeks: OEE, changeover times, short stops by cause, fill weight overfill and holds.
- Start a 15-minute meeting at a board by the line at the start of each shift.
- Walk the line with operators, sanitation and maintenance, and list what slows them down.
- Choose the two biggest losses to work on first.
Days 31 to 60
Fix the top two losses
Run focused improvements on the two problems and check them against the baseline.
- Run a SMED workshop on the most frequent changeover, with the food safety team in the room.
- Start the daily operator care routine and the short-stop tally on the pacing machine.
- Put fill weights on a control chart and fix the drifting heads.
- Write each new method down as standard work or a one-point lesson as soon as it works.
Days 61 to 90
Make it stick, then spread it
Check the new standards hold on every shift, then copy them to the next line.
- Audit the new standards on every shift with short layered audits.
- Train every operator on the changes and update the skills matrix.
- Compare the line's numbers with the baseline and share the result with the plant.
- Pick the next line, copy what worked and start again at day one.
The KPIs to track
Track them per line and shift, on a board the team sees every day. Set targets from your own baseline, not from someone else's plant.
| KPI | What it tells you | How to measure it | Free help |
|---|---|---|---|
| OEE | How much of the planned time made good product at full speed, and which of availability, performance or quality is losing most. | Availability times performance times quality, per shift, on the pacing machine. | OEE calculator |
| Changeover time | How long the line is down between products, and whether the new standard is followed. | Last good unit to first good unit, for every changeover, by product pair. | SMED changeover calculatorChangeover checklist |
| Short stops per shift | The hidden losses on filling and packaging that never reach the downtime report. | Tally by cause on a check sheet or from the machine counter, on the pacing machine. | Equipment downtime log (MTTR and MTBF) |
| Average overfill | Product given away above the target weight. | Mean fill weight minus target, by head or lane, from routine checkweigher or sample data. | X-bar and R control chart template |
| First pass yield | The share of product made right first time, without rework, sorting or holds. | Good units first time divided by units started, per line and shift. | First pass yield (FPY) calculator |
| Holds per month | Whether quality problems are being fixed at the cause or just contained. | Count of holds by cause, with the quantity held. | Non-conformance report (NCR) form |
| Skills coverage | Whether every position can be run by a trained person when people are off or new. | Positions with at least two signed-off people per shift, from the skills matrix. | Skills matrix template |
By the numbers
Public figures for this industry or for the wider sector it belongs to, each linked to the report or government table it comes from and checked against it on October 3, 2026. More in our lean manufacturing statistics and benchmark charts.
3.3
Food manufacturing recorded 3.3 injury and illness cases per 100 full-time workers in 2024, and beverage and tobacco manufacturing 3.7, against 2.7 for all manufacturing and 2.3 for all private industry.
Total recordable cases per 100 full-time workers, U.S. private industry, 2024 data from the Survey of Occupational Injuries and Illnesses.
Source: U.S. Bureau of Labor Statistics, Table 1. Incidence rates of nonfatal occupational injuries and illnesses by industry and case types, 2024 (2024 data, table updated January 22, 2026)
$36,000
In fast-moving consumer goods, the Siemens sector closest to packaged food and beverage, an hour of unplanned downtime at a large plant costs about $36,000.
Siemens survey of 181 maintenance, engineering and IT staff at large plants in four sectors, April 2019 to March 2023.
Source: Siemens, The True Cost of Downtime 2024 (Senseye Predictive Maintenance) (2024)
2×
The yearly cost of unplanned downtime at a large fast-moving consumer goods plant has doubled since 2019, to just over $10 million, and it is the only sector in the Siemens survey where hours lost to downtime have gone up.
Same Siemens survey. Siemens suggests the sector has invested less in predictive maintenance because each hour costs less.
Source: Siemens, The True Cost of Downtime 2024 (Senseye Predictive Maintenance) (2024)
Injury and illness rate by industry, 2024
- Motor vehicles5.6
- Beverage and tobacco3.7This industry
- Furniture3.5
- Food3.3This industry
- Primary metals3.3
- Nonmetallic mineral products, incl. glass3.3
- Fabricated metal products3.2
- Transportation equipment3.2
- Motor vehicle parts2.9
- Plastics and rubber products2.8
- HVAC and refrigeration2.4
- Paper2.4
- Machinery2.3
- All private industry2.3
- Electrical equipment and appliances2.0
- Printing1.6
- Chemicals1.6
Total recordable cases per 100 full-time workers, 2024: Motor vehicles 5.6, Beverage and tobacco 3.7, Furniture 3.5, Food 3.3, Primary metals 3.3, Nonmetallic mineral products, incl. glass 3.3, Fabricated metal products 3.2, Transportation equipment 3.2, Motor vehicle parts 2.9, Plastics and rubber products 2.8, All manufacturing 2.7, HVAC and refrigeration 2.4, Paper 2.4, Machinery 2.3, All private industry 2.3, Electrical equipment and appliances 2, Printing 1.6, Chemicals 1.6.
Free templates, calculators and buyer's guides
Templates (24)
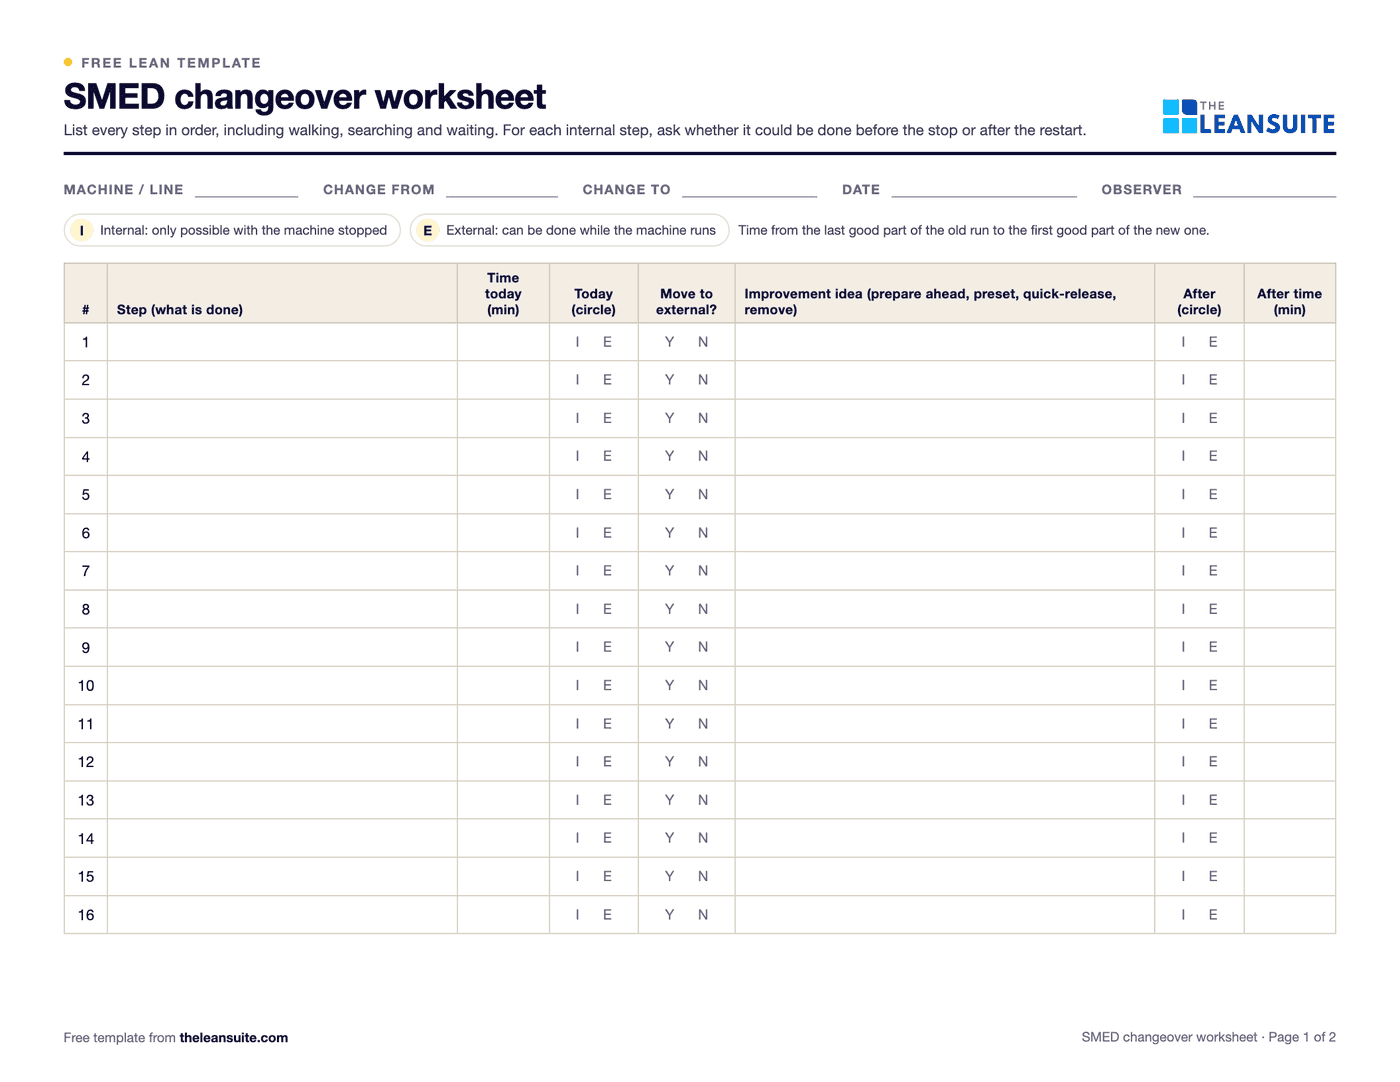 PDF and ExcelSMED changeover worksheetChangeover steps with times, internal or external, what can move, ideas and before/after totals.
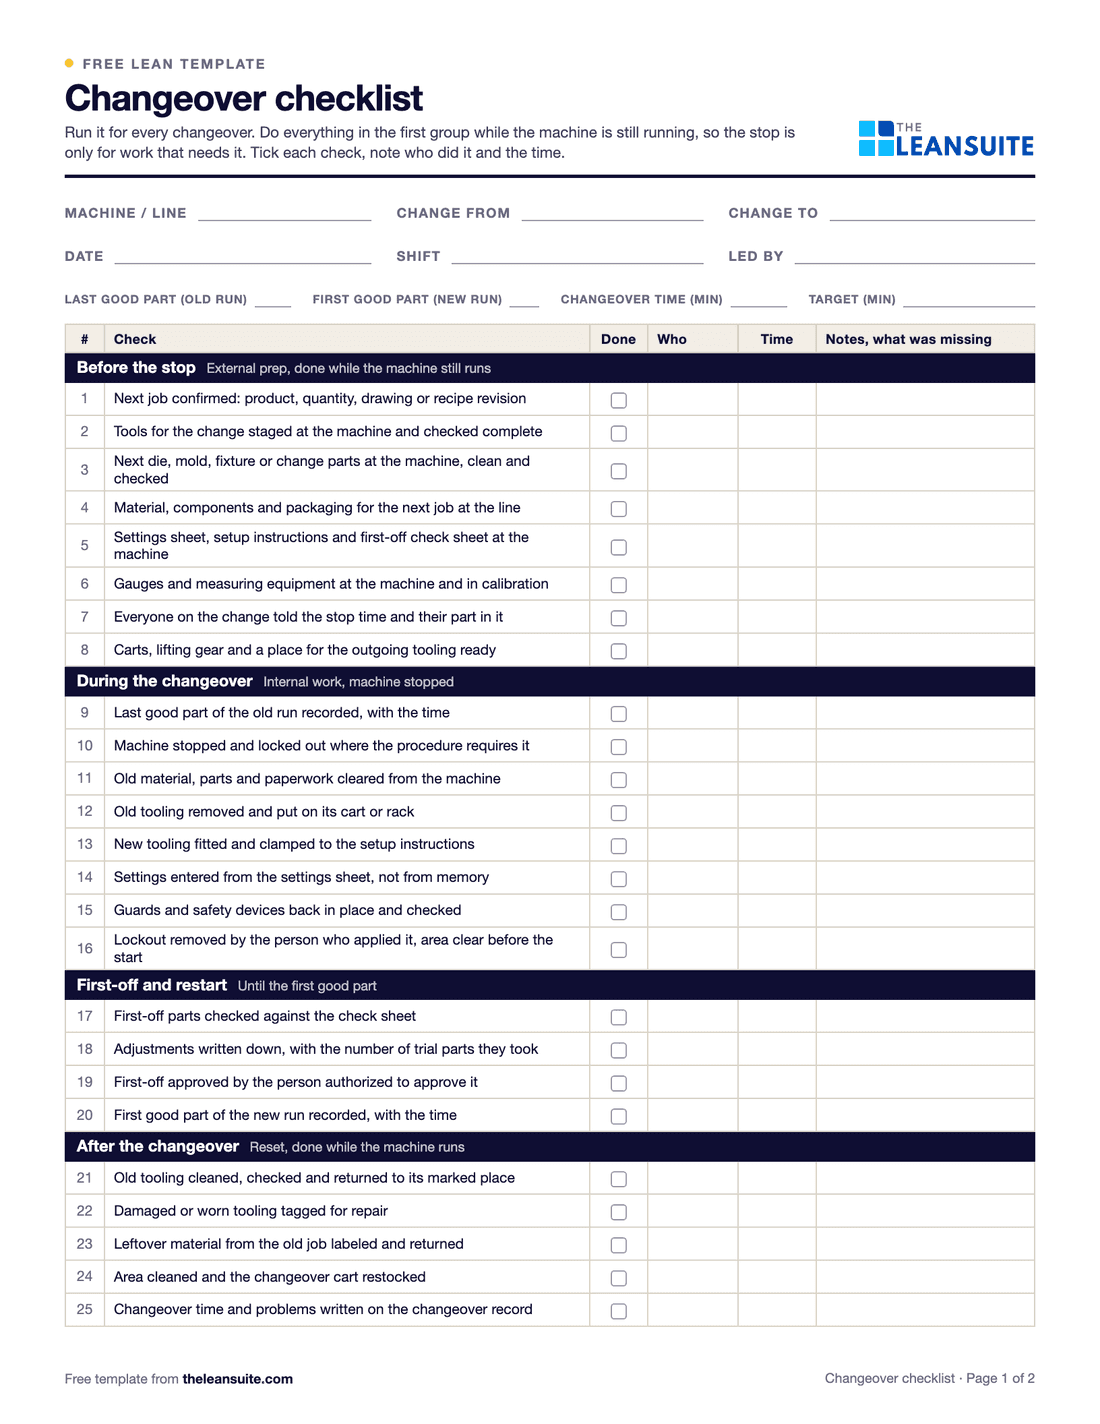 PDF and ExcelChangeover checklist25 checks for every changeover, a record of planned and actual times, and a log of changeover time against target.
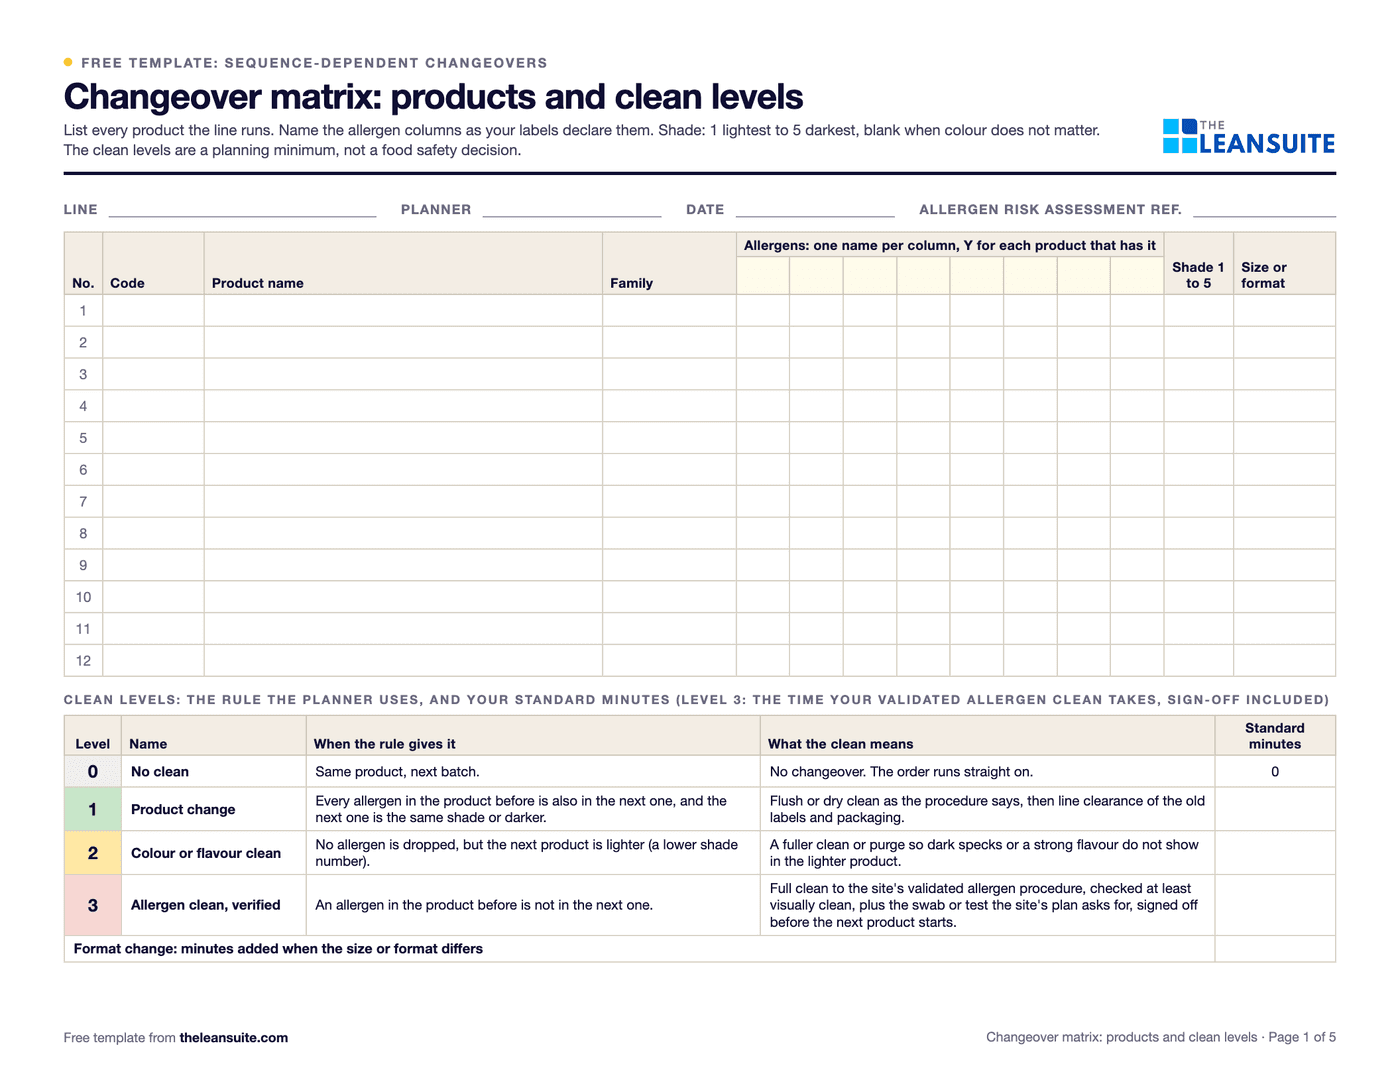 PDF and ExcelChangeover matrix templateA from-to matrix of changeover minutes with the clean each transition needs (allergen, colour, format), and a weekly planner that totals the order and suggests a shorter one.
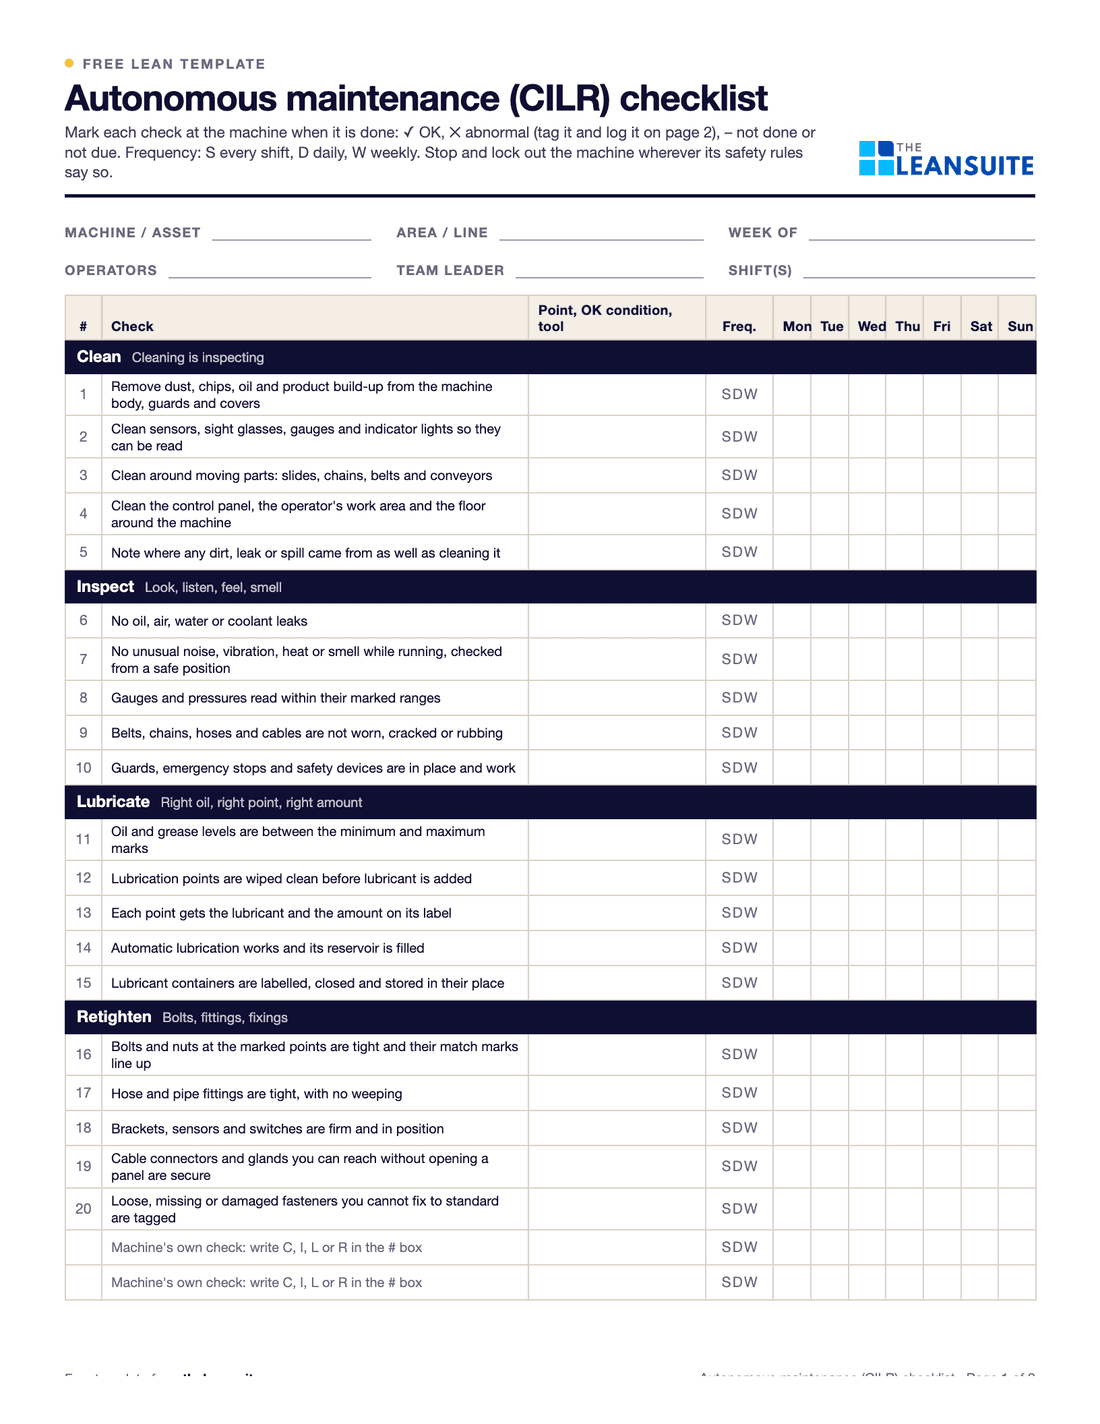 PDF and ExcelAutonomous maintenance (CILR) checklist20 clean, inspect, lubricate and retighten checks with a box per day, an abnormality log and sign-off.
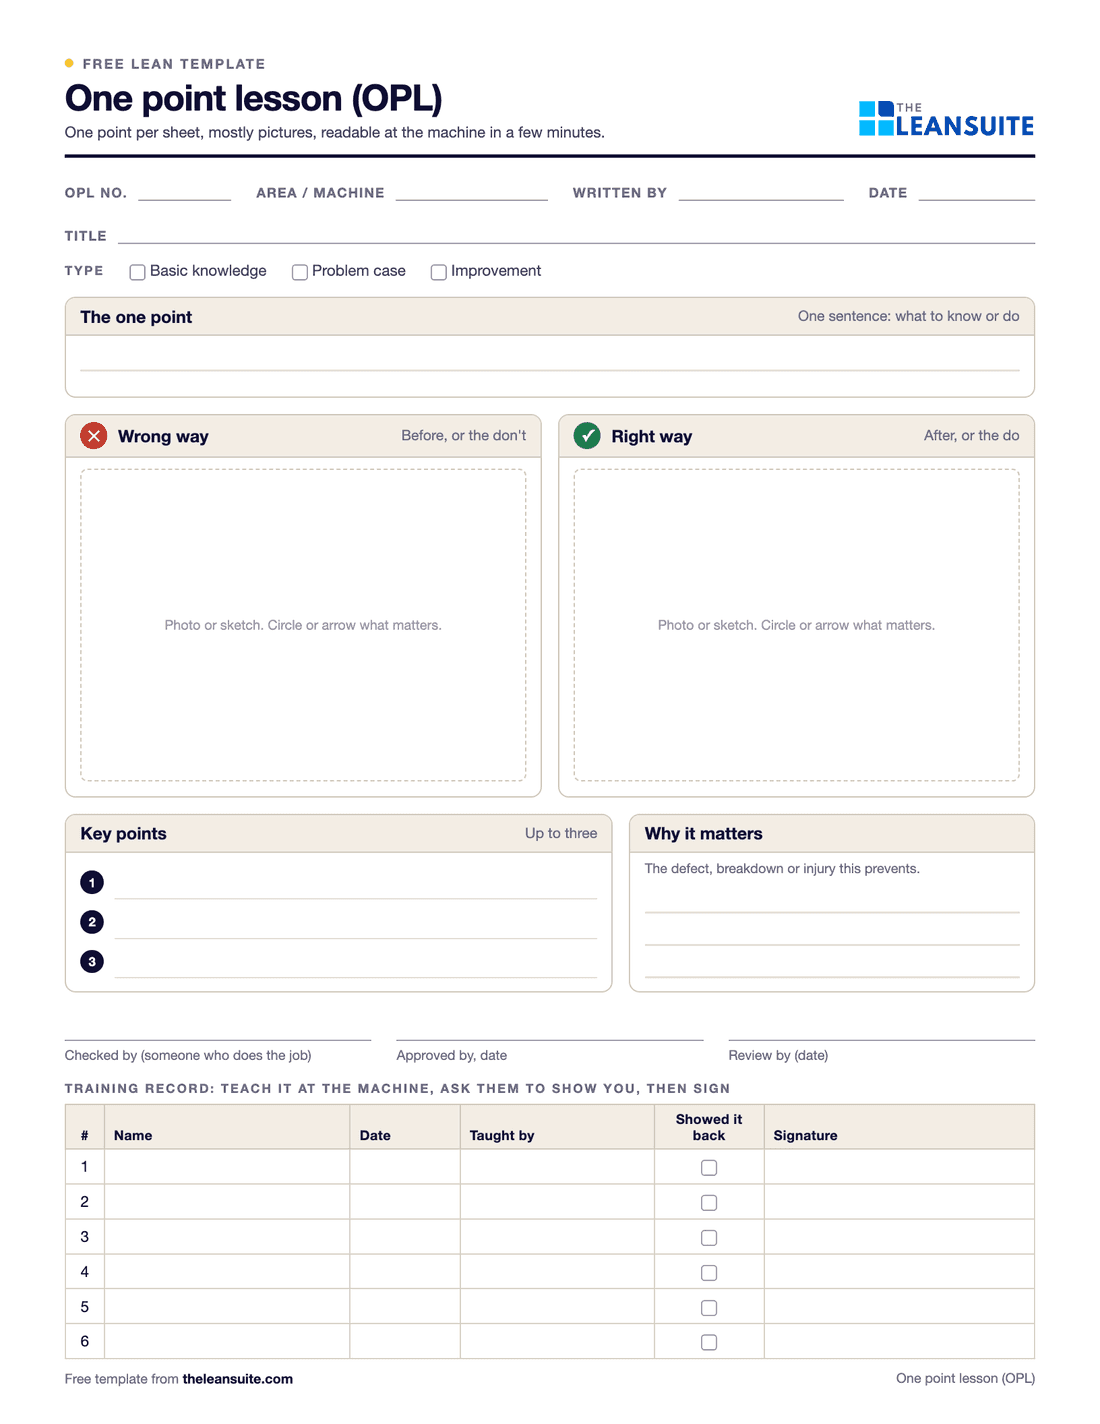 PDF and Excel and WordOne point lesson (OPL) templateOne topic on one page: wrong way and right way pictures, checkable key points, the standard it belongs to and a sign-off record.
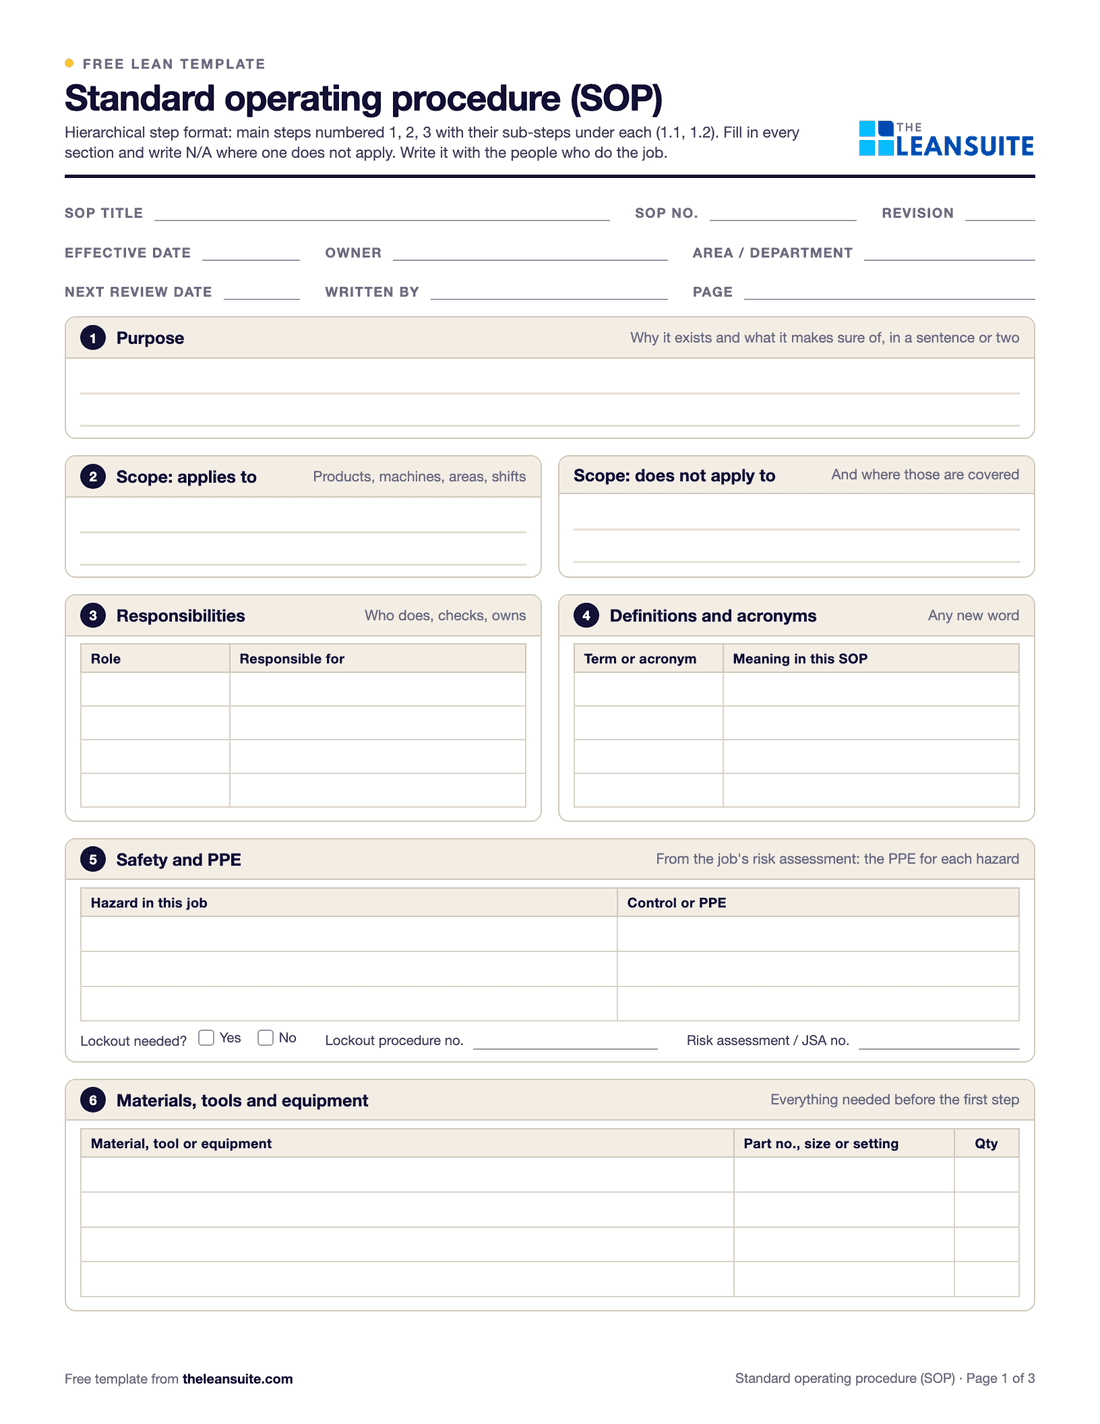 PDF and Excel and WordStandard operating procedure (SOP) templateA full SOP in the hierarchical step format, from purpose and scope to the steps, records, revision history and approvals, with review checks and an SOP register.
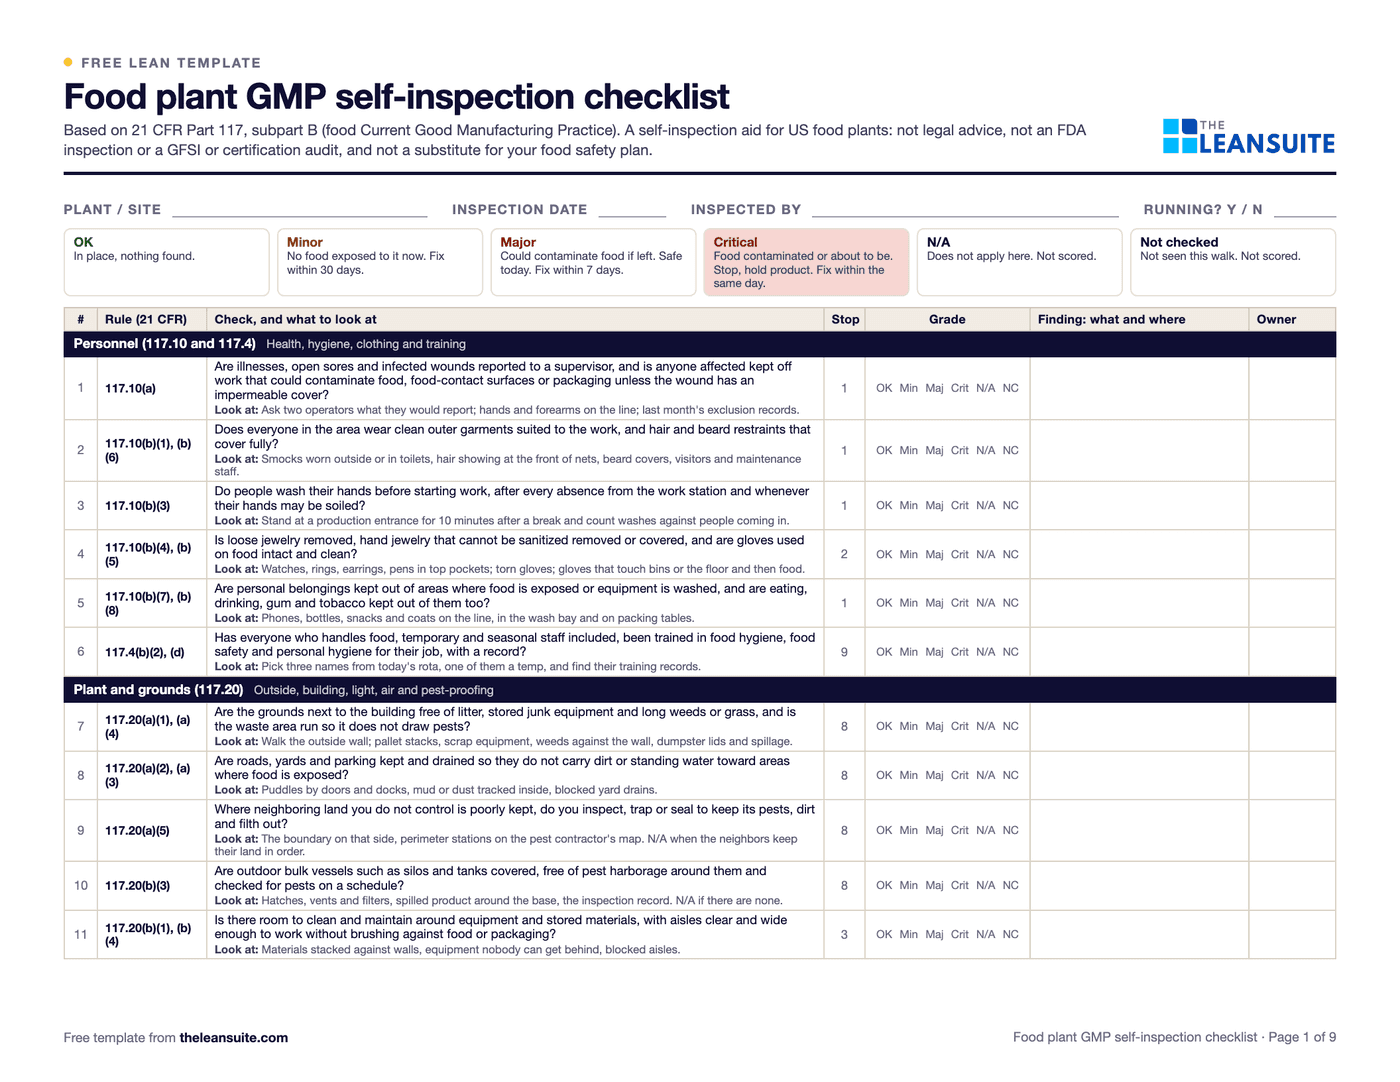 PDF and ExcelFood plant GMP inspection checklist (21 CFR 117 subpart B)55 checks in the order of 21 CFR 117 subpart B, each citing its paragraph and saying what to look at, with a grade, finding, owner and due date; results by section and grade, a walk route and a bakery example.
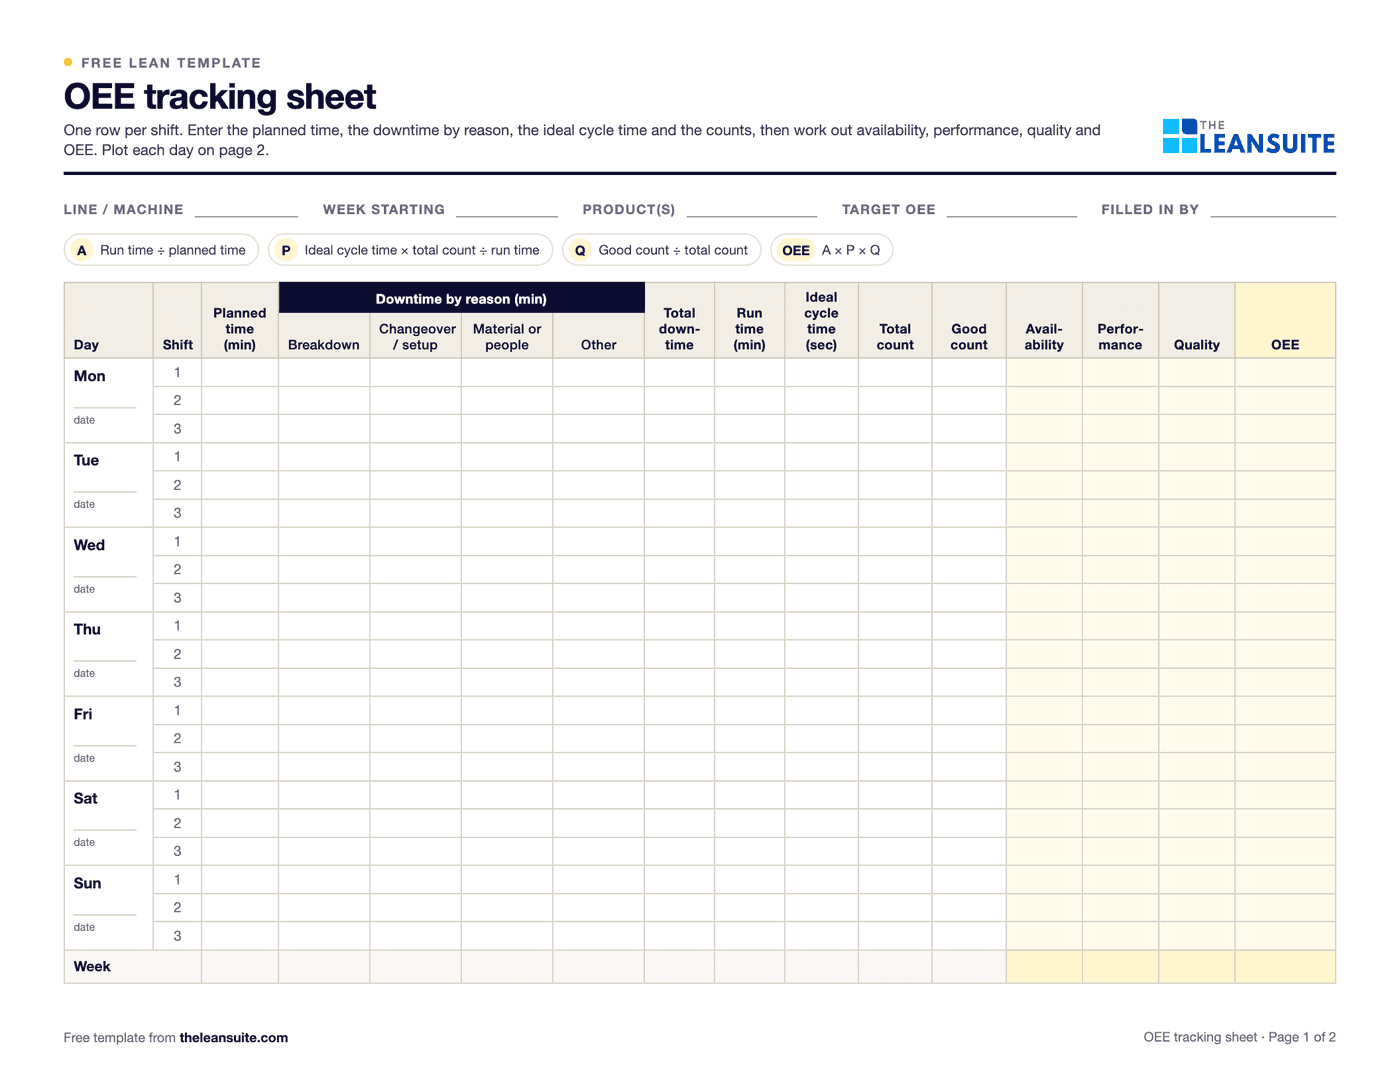 PDF and ExcelOEE tracking sheetOne row per shift for a week. The Excel version works out availability, performance, quality and OEE and charts the week.
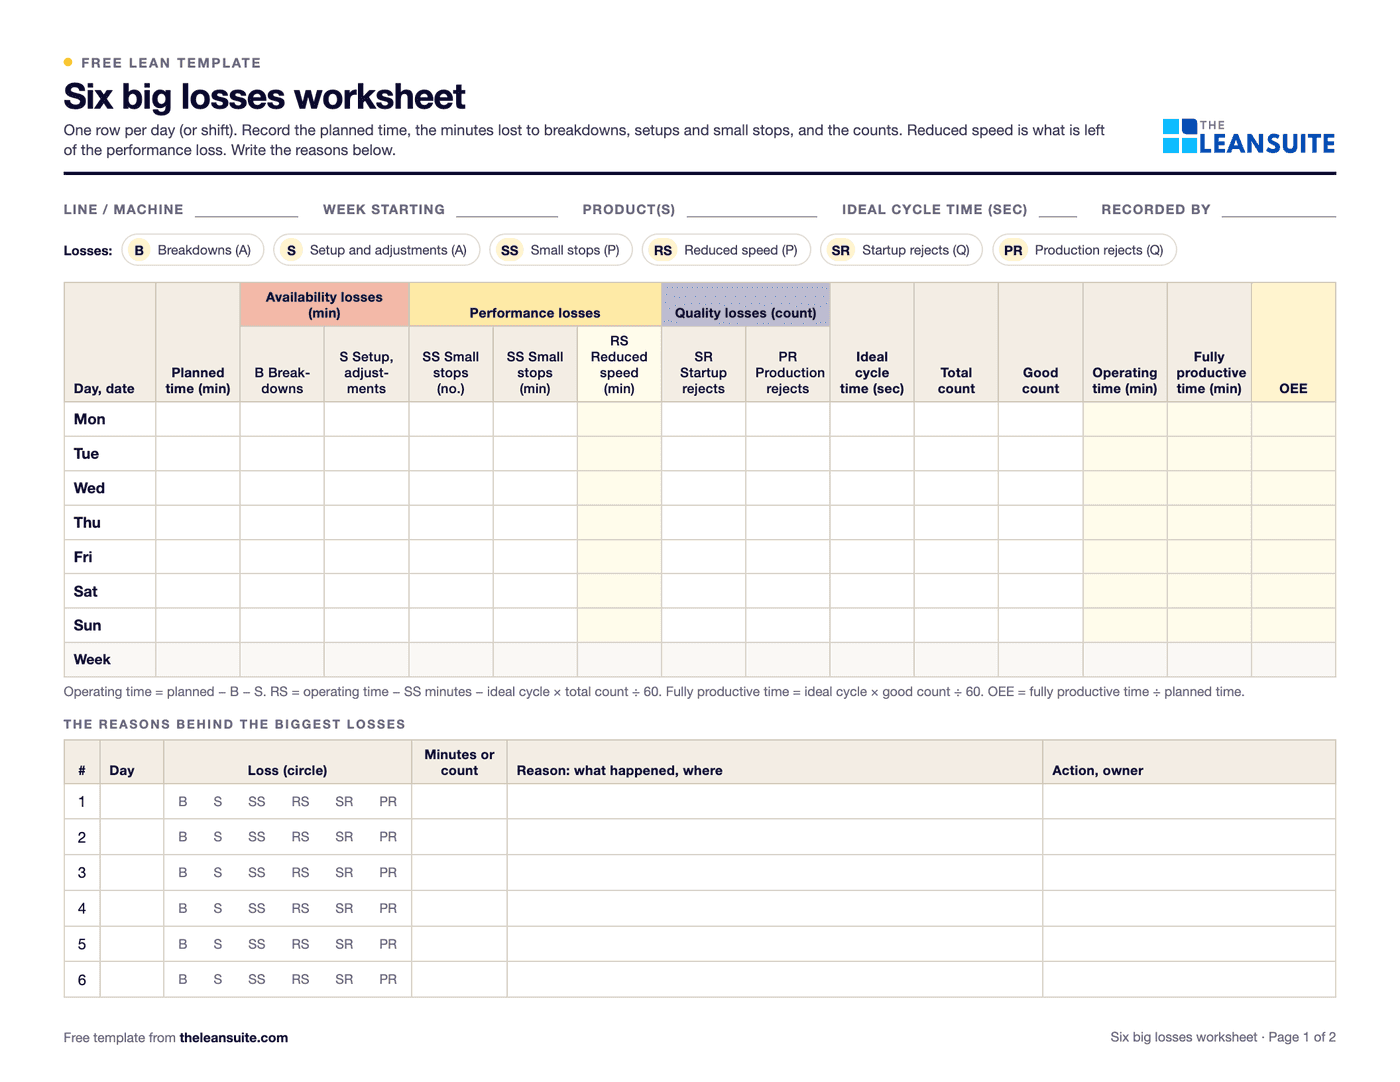 PDF and ExcelSix big losses worksheetWhere a machine's planned time goes: the six big losses in minutes, ranked, with A, P, Q and OEE worked out.
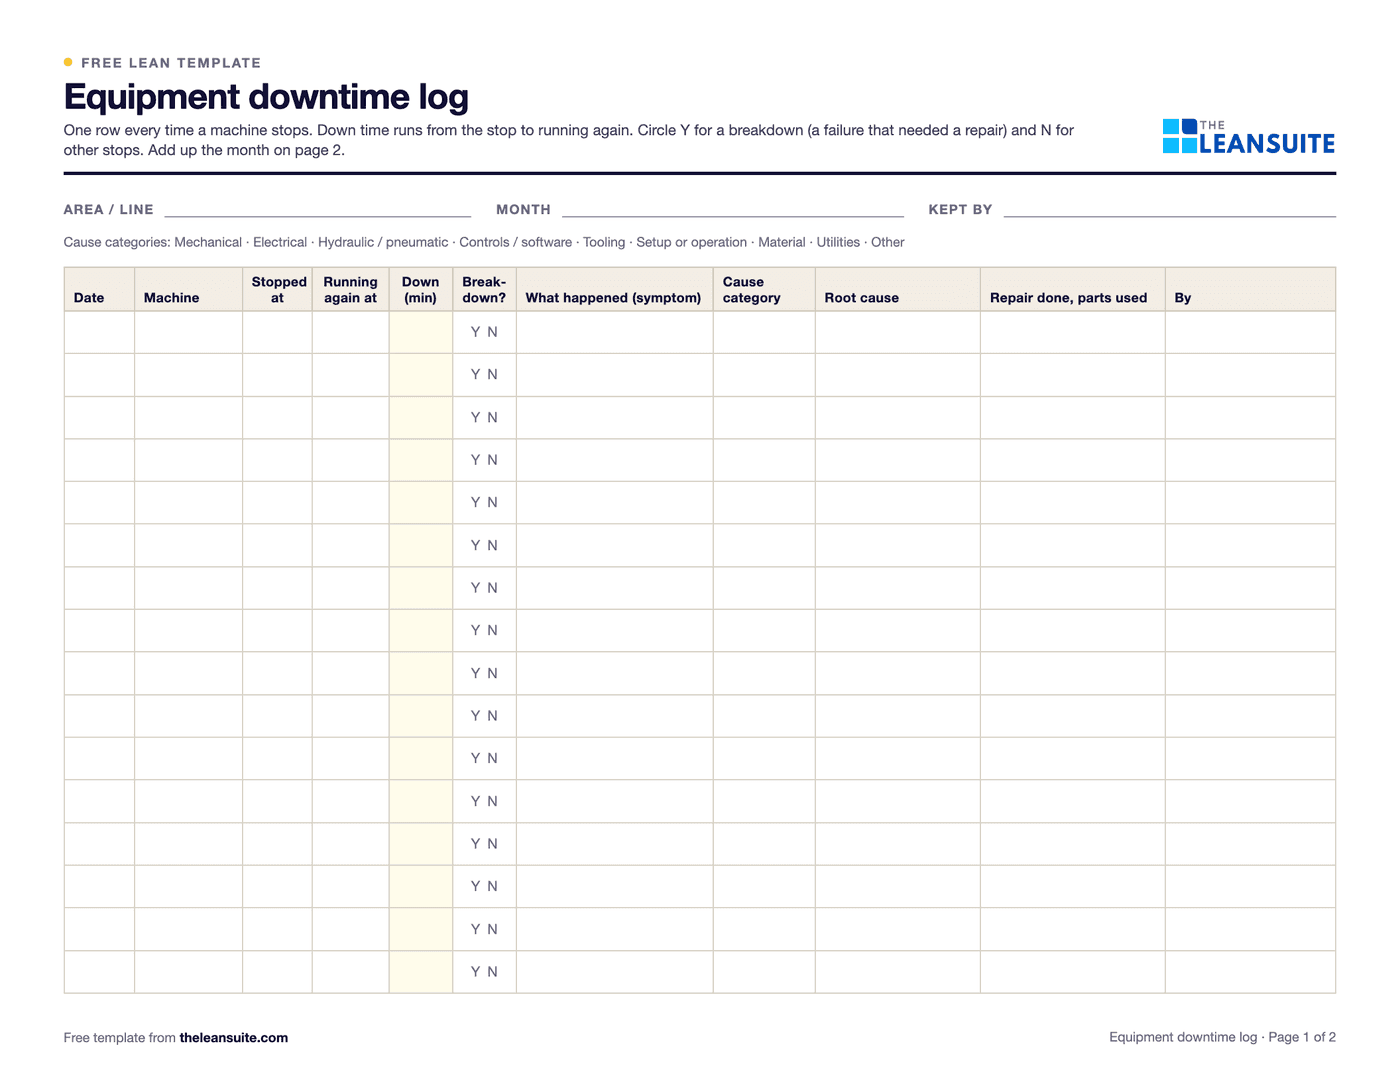 PDF and ExcelEquipment downtime log (MTTR and MTBF)A breakdown and downtime log, with MTTR, MTBF and downtime by machine and cause worked out in Excel.
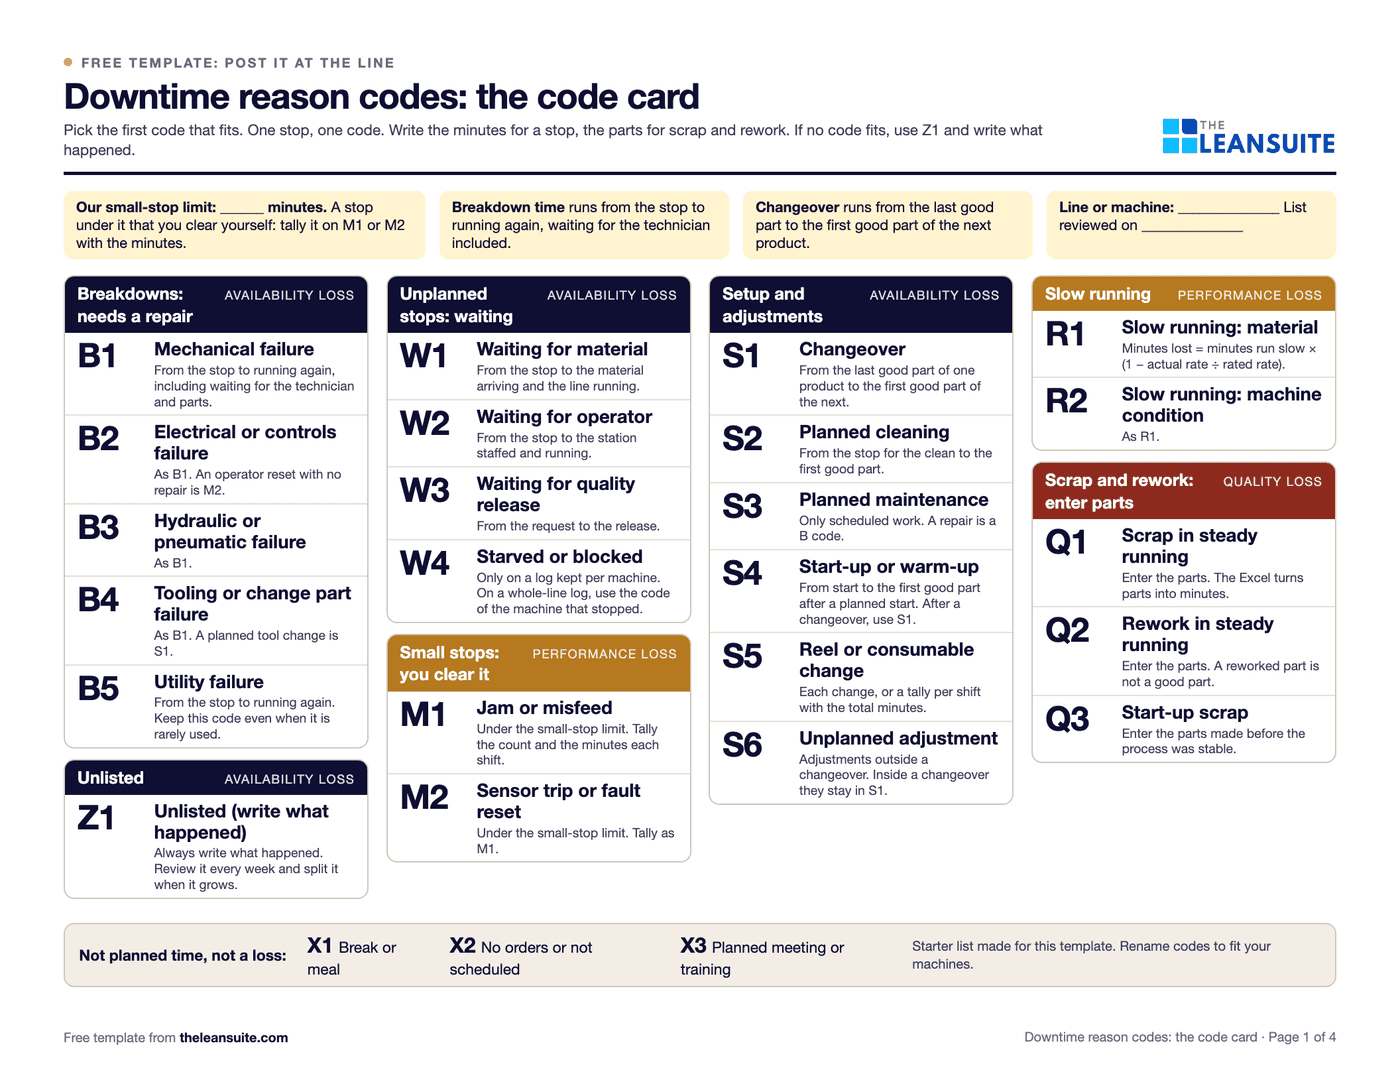 PDF and ExcelDowntime reason codes template26 starter codes mapped to the six big losses, a log with drop-downs, a Pareto by code and by loss, and a code card for the line.
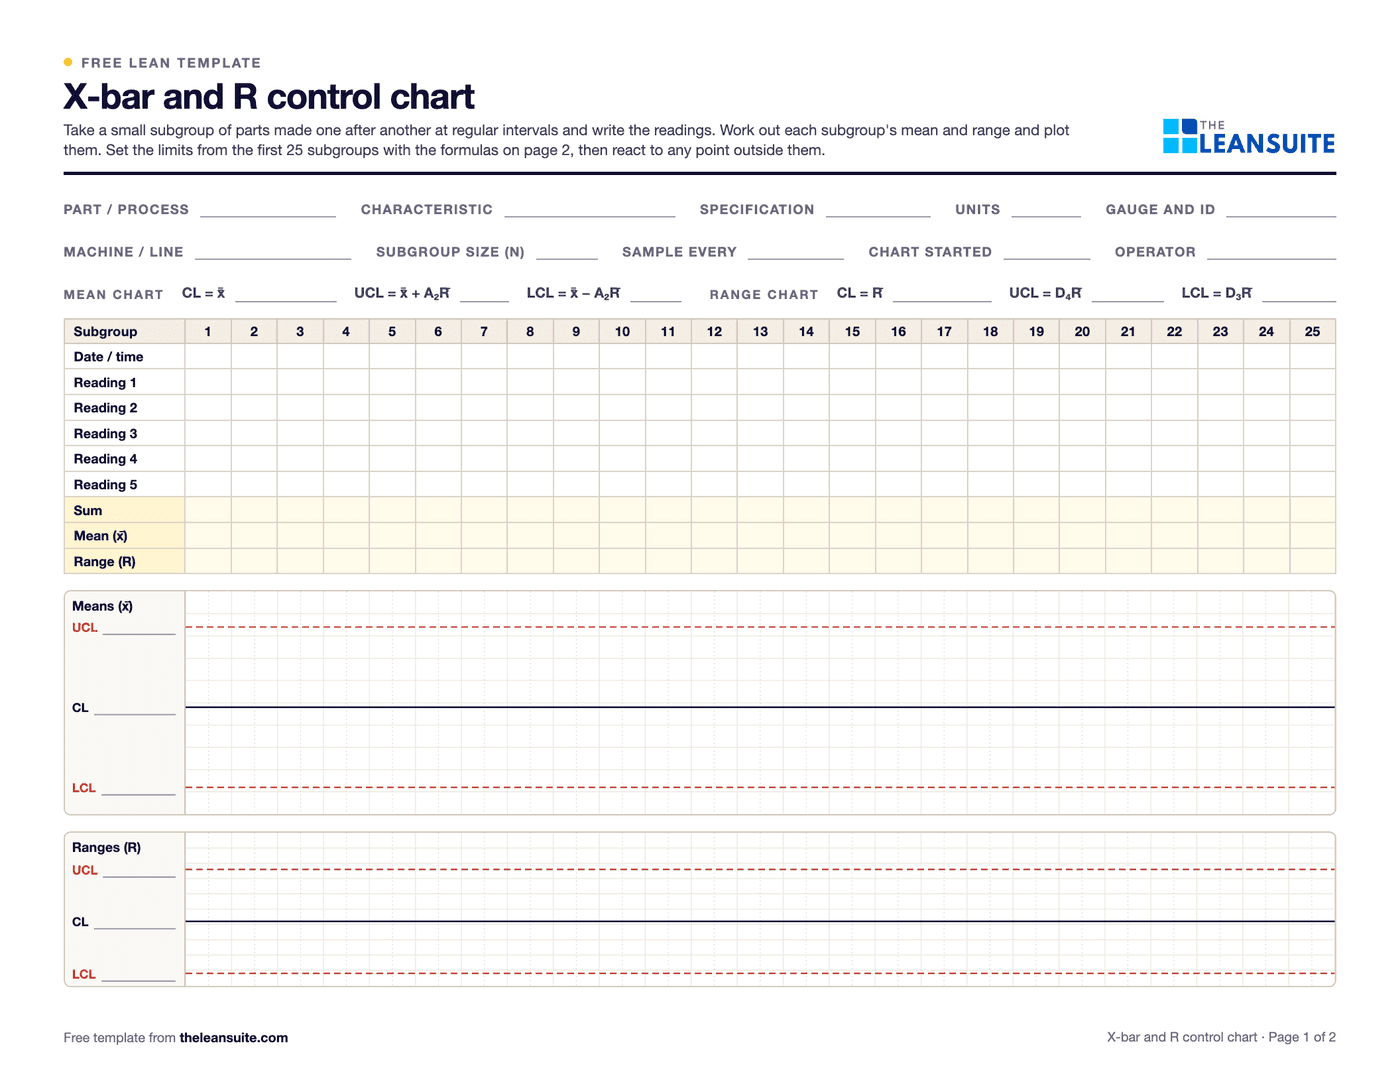 PDF and ExcelX-bar and R control chart template25 subgroups with means and ranges, control limits from A2, D3 and D4, signal flags, both charts and a reaction log.
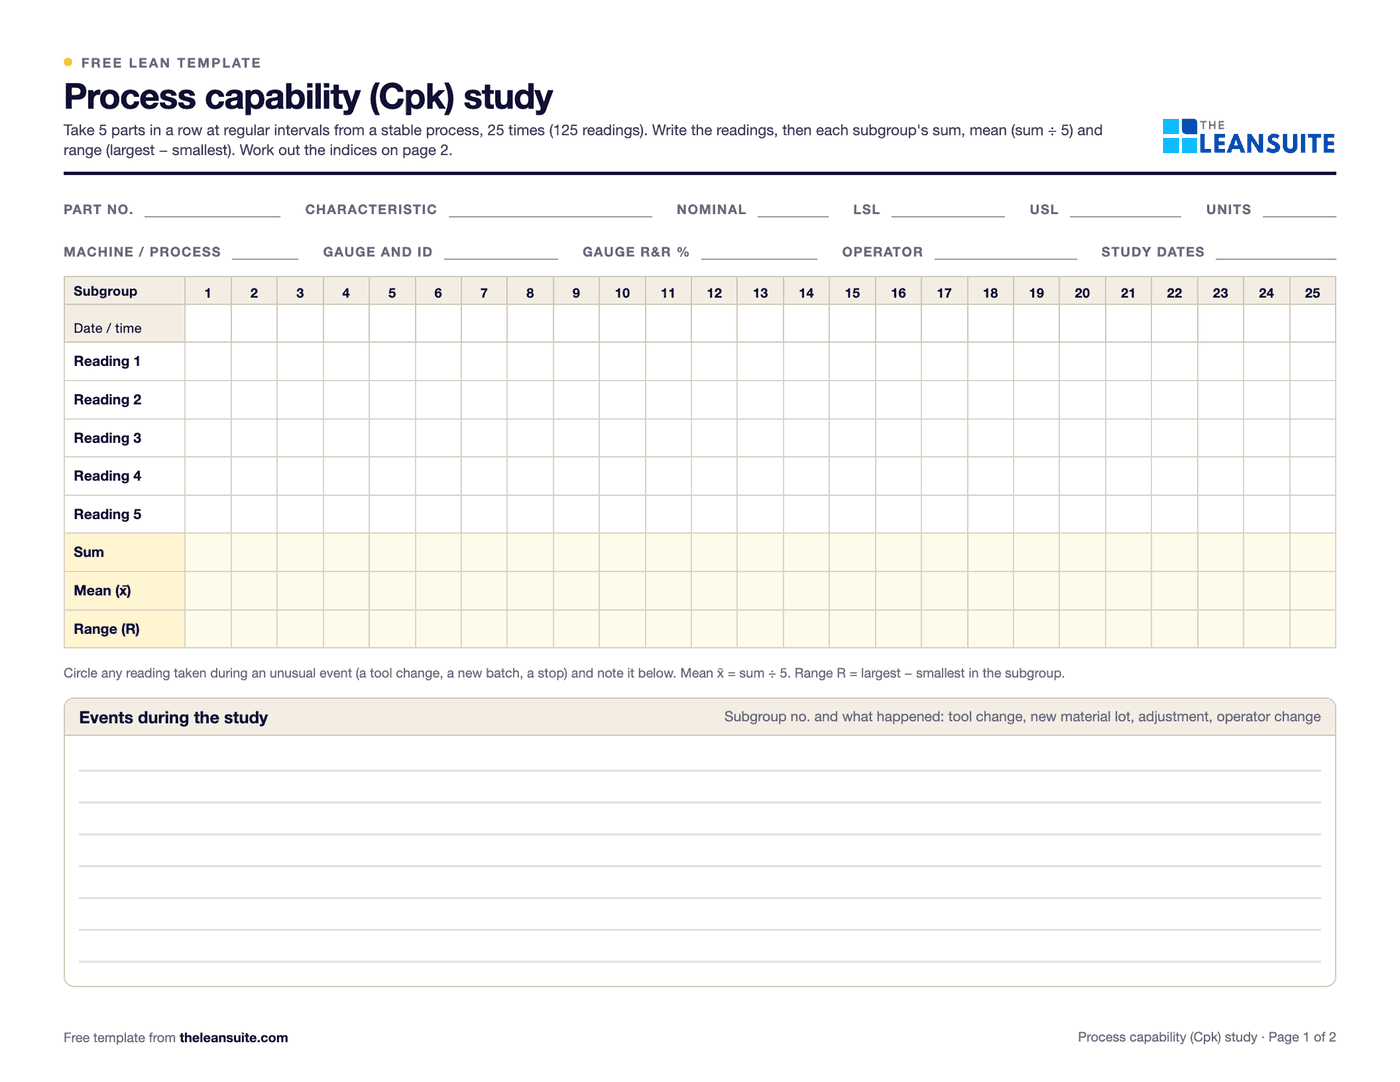 PDF and ExcelProcess capability (Cpk) study sheet25 subgroups of readings with Cp, Cpk, Pp and Ppk worked out, control limits to check stability, and a histogram.
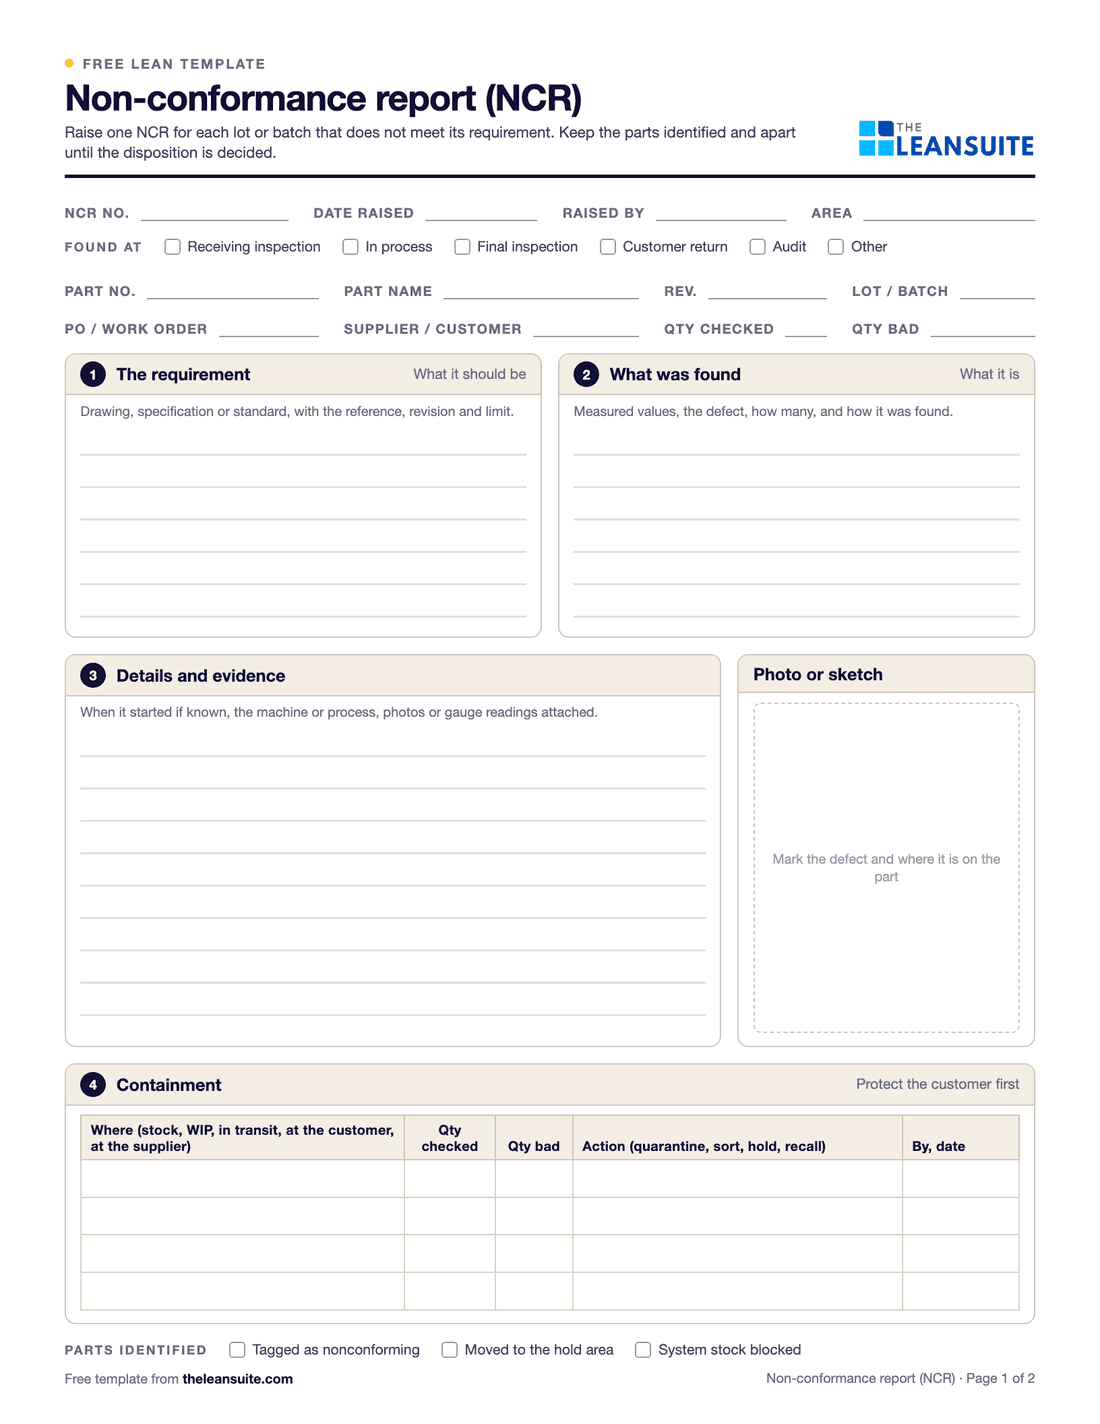 PDF and Excel and WordNon-conformance report (NCR) formA two-page NCR from the requirement against what was found to disposition and closure, and an Excel NCR log.
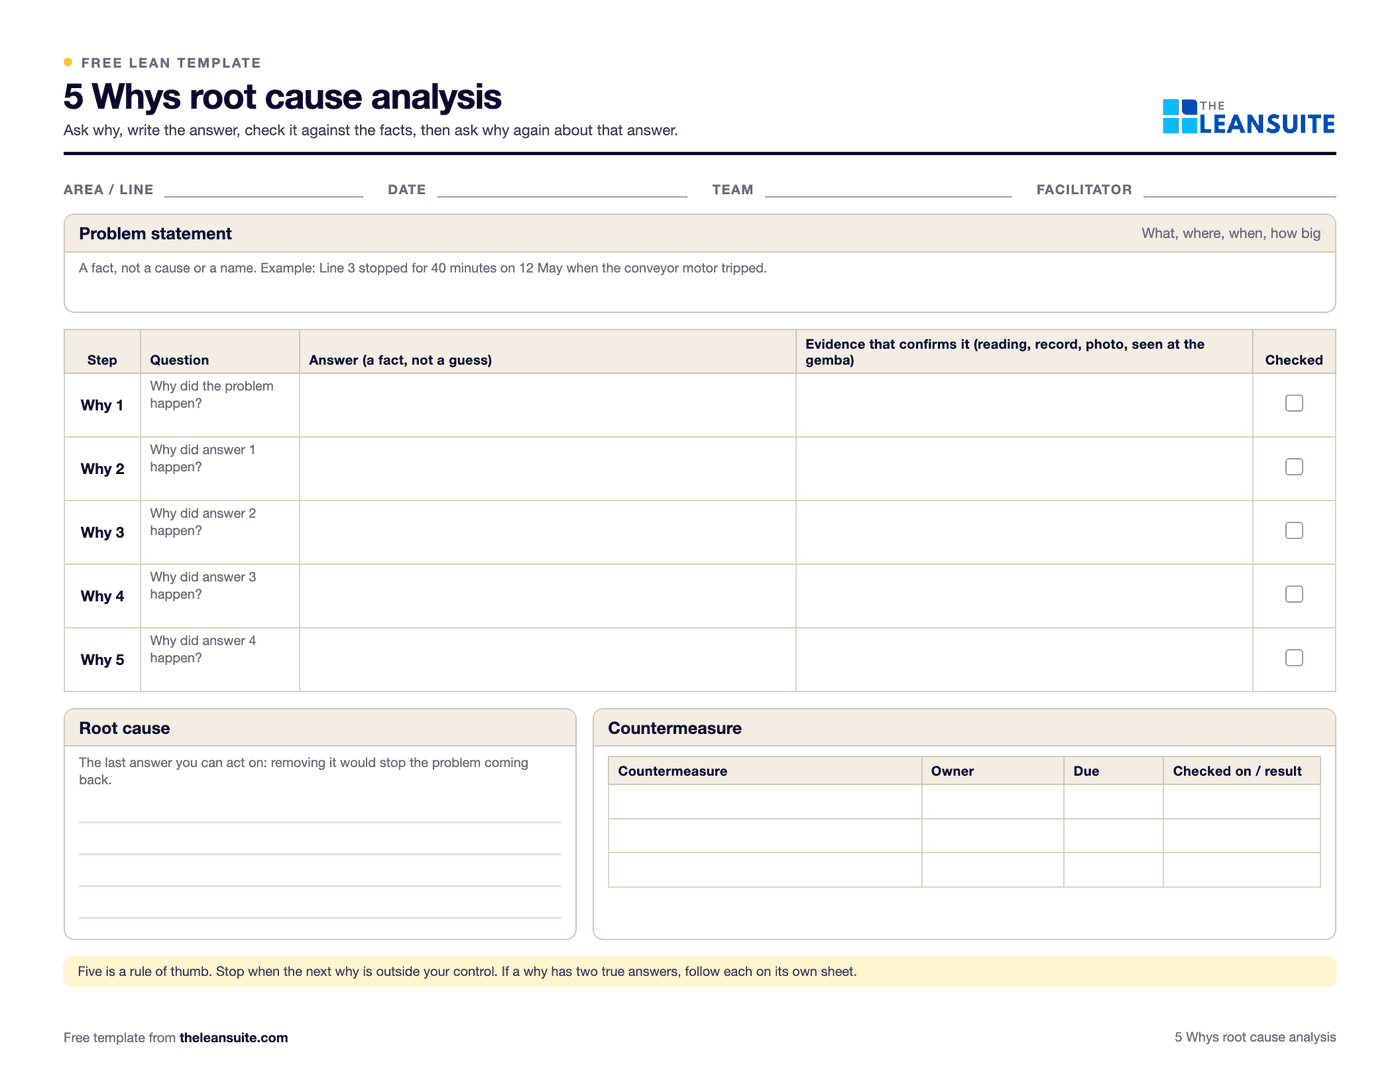 PDF and Excel and Word5 Whys templateA problem statement, a why chain that can branch, evidence for every answer, root causes and countermeasures that are checked.
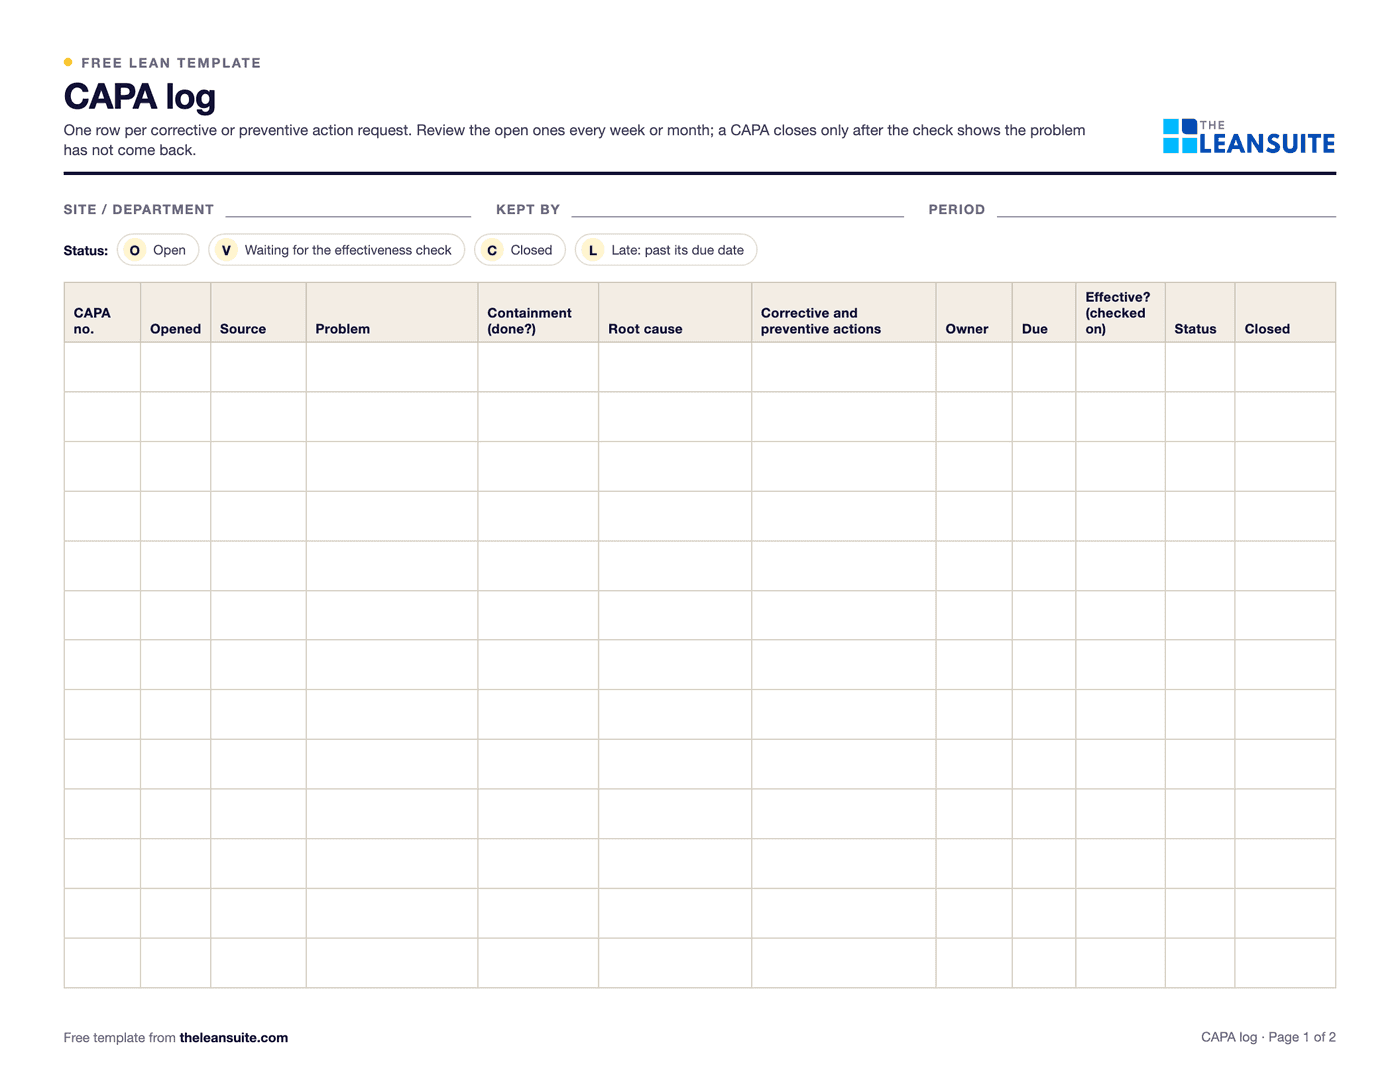 PDF and Excel and WordCAPA log templateAn Excel CAPA tracker with status, days open, late flags and counts by source, plus a printable log and monthly review.
 PDF and ExcelTWI job breakdown sheetThe TWI Job Instruction breakdown of a job into important steps, key points and reasons, with a worked example and the four steps.
 PDF and ExcelSkills matrix templatePeople by tasks on a 0 to 4 scale, coverage and gaps per task and shift, and a training plan that closes them.
 PDF and ExcelTraining sign-off sheetAn attendance and sign-off record where each person signs they understood, with a competence check and an Excel log.
 PDF and ExcelTraining matrix template with expiry datesPeople by required trainings with expiry dates, OK, due, expired and missing flags, compliance by person and area, cover per training and a renewal list.
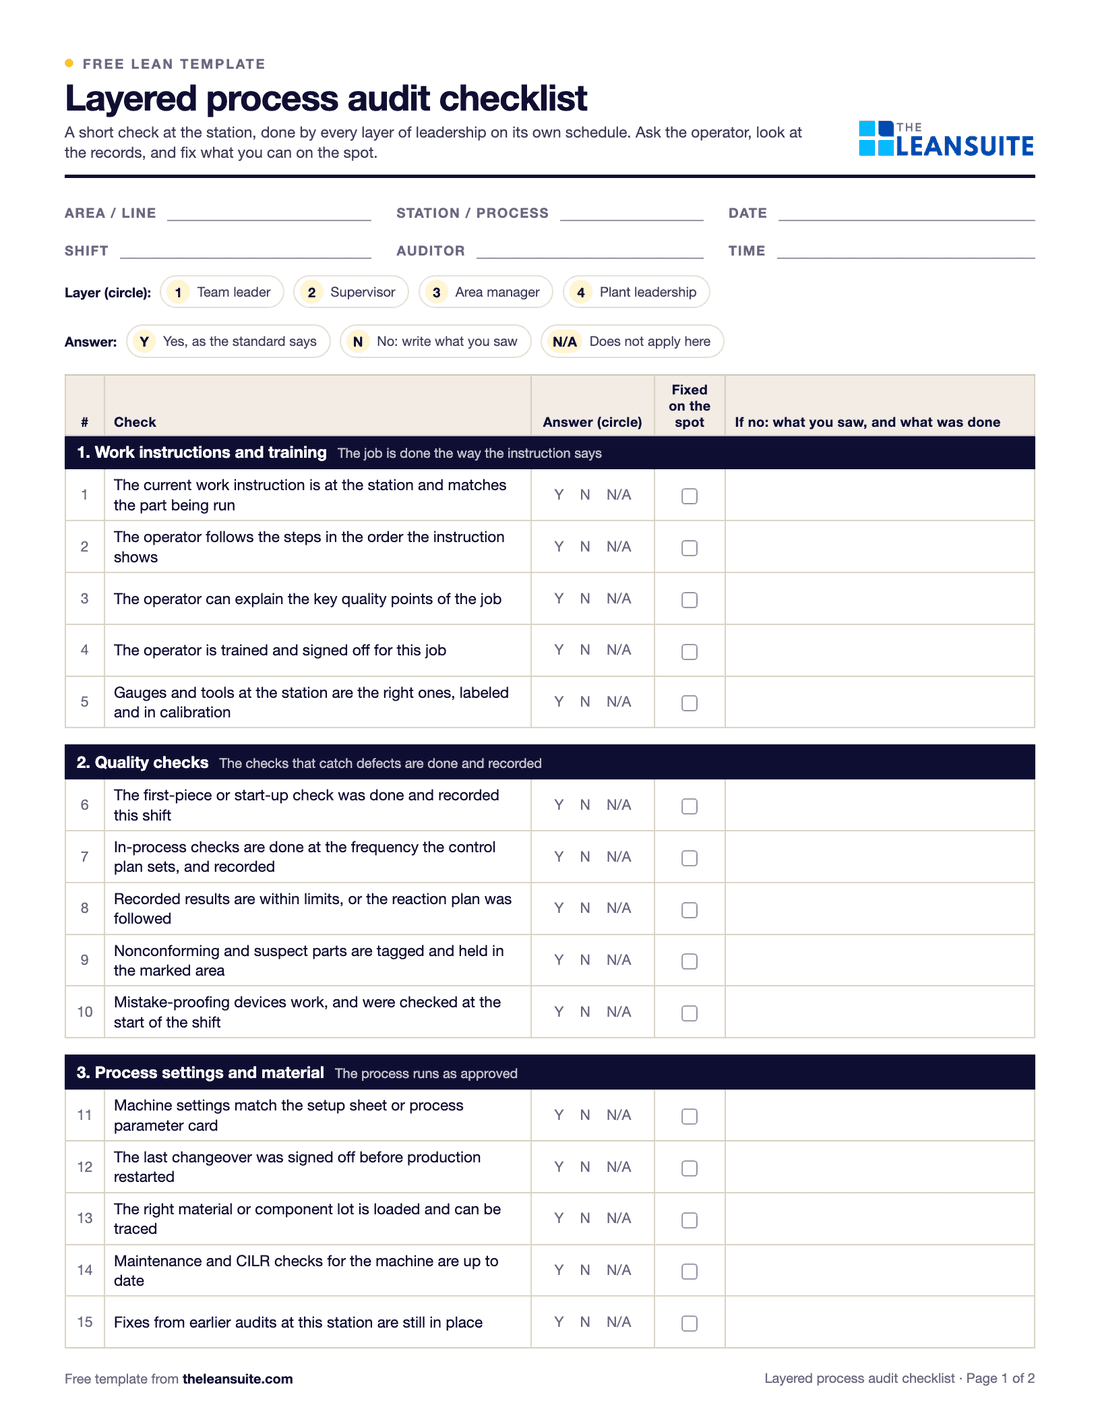 PDF and Excel and WordLayered process audit (LPA) checklist20 yes, no or N/A checks at the station, a layer and frequency matrix, question banks for four processes and a findings table.
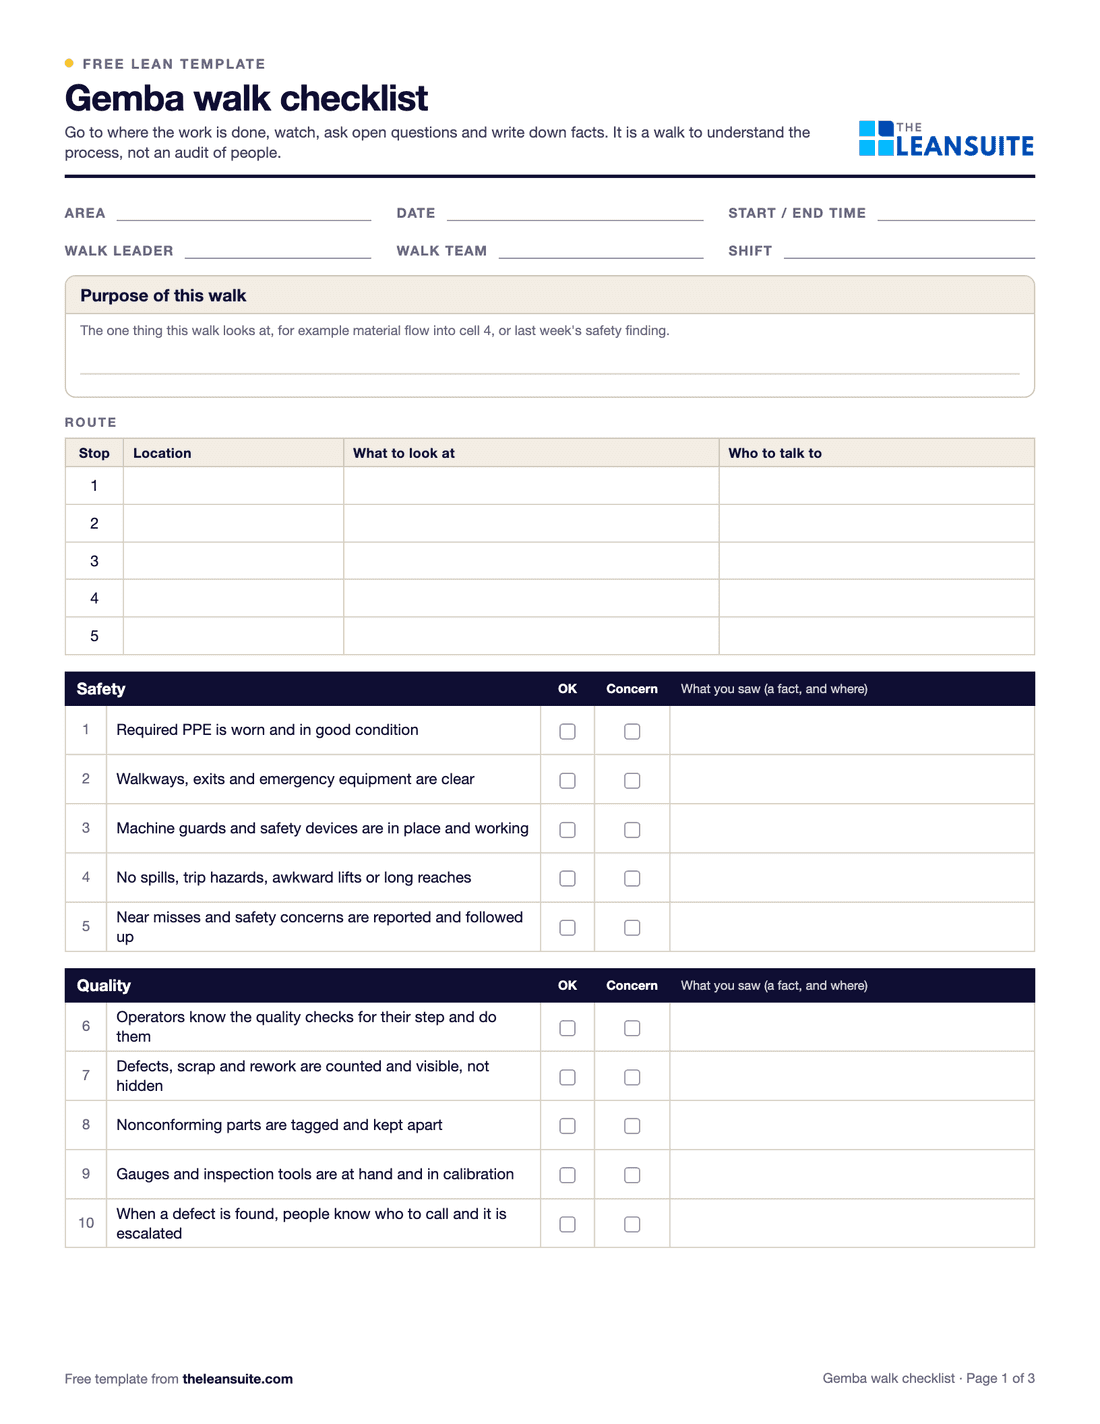 PDF and Excel and WordGemba walk checklistA walk plan and route, 30 prompts in six groups and a findings table with owners and due dates.
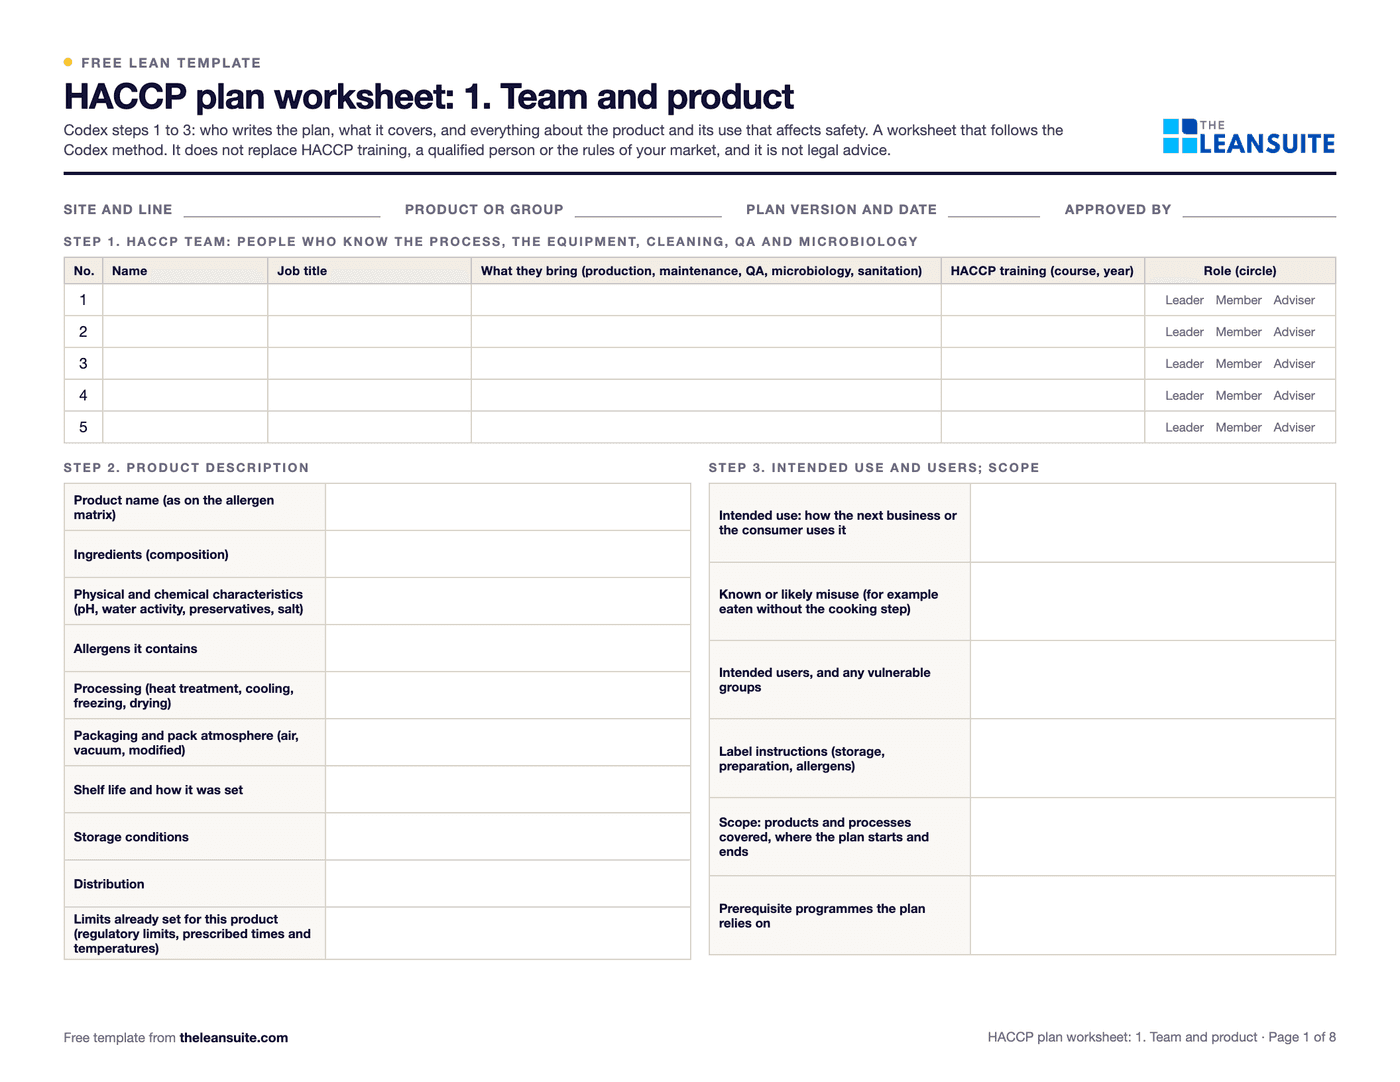 PDF and ExcelHACCP plan template: hazard analysis and CCP worksheetThe Codex 12 steps in one workbook: team and product, process steps checked on site, hazard analysis with the CCP decision tree, the CCP table with completeness checks, an allergen matrix and a verification schedule.
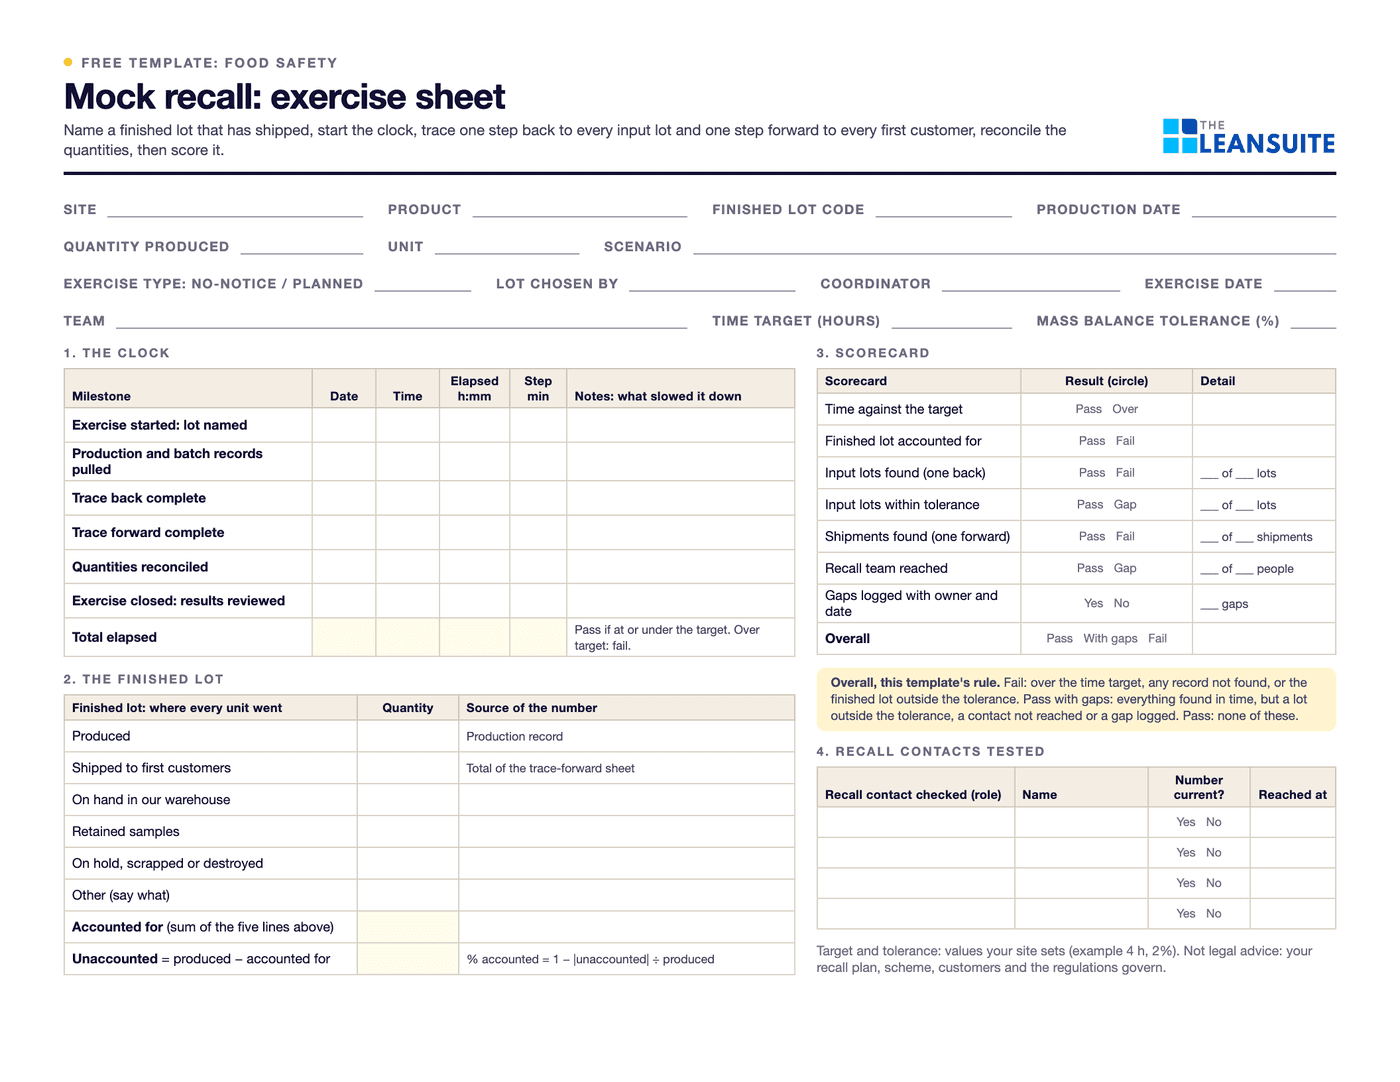 PDF and ExcelMock recall template: traceability exercise worksheetTrace a finished lot back to every input lot and forward to every first customer, reconcile the quantities against a tolerance and time it against your target.
Calculators (6)
- Free calculatorSMED changeover calculatorTime saved by moving changeover steps from internal to external, capacity freed per week and the smaller batch it allows.
- Free calculatorOEE calculatorOverall equipment effectiveness from shift time, downtime, ideal cycle time and part counts.
- Free calculatorDowntime cost calculatorWhat an hour, an event and a year of unplanned downtime cost, from lost output, idle labour, scrap and overtime.
- Free calculatorProcess capability (Cp, Cpk) calculatorCp and Cpk against your specification limits, plus Pp and Ppk from pasted measurements, with a distribution chart.
- Free calculatorFirst pass yield (FPY) calculatorFirst pass yield at each step and rolled throughput yield (RTY) across the whole process.
- Free calculatorCost of poor quality (COPQ) calculatorTotal COPQ and cost of quality, and each as a share of revenue, from the four quality cost categories.
Buyer's guides
LeanSuite pages for these problems
- SMED
- AI SMED changeover analysis
- CILR Checklists
- Checklists
- Audit Management
- Audit Readiness
- Digital Work Instructions
- Trainings (LMS)
- On-the-Job Training
- Micro-stops
- Loss & Cost Management
- KPI Dashboards
- Non-Conformance (NCR)
- Cost of Poor Quality
How LeanSuite handles each of these is on the page for food and beverage plants.
FAQ
Lean in food and beverage plants: common questions
On one line, with the loss you can count most easily. For most food lines that is changeover time, short stops on filling and packaging or giveaway on fill weights. Measure it for two weeks, fix the biggest cause with the people who run the line, write the new method down and only then move to the next line.
SMED for allergen and product changeovers, autonomous maintenance (a daily clean, inspect, lubricate and retighten routine) for short stops, control charts for fill weights, TWI job instruction for seasonal operators, and 5S and visual standards for hygiene areas. Root cause analysis and error-proofing deal with repeat holds.
It should not, but every change to cleaning, sanitation, allergen control or line clearance must be reviewed by your food safety team against your food safety plan before it is made. Lean removes waiting and searching around those steps; it does not skip the steps themselves.
OEE on the pacing machine, changeover time, short stops per shift, average overfill and first pass yield. Add holds per month and skills coverage once those are in place. Track them per line and shift, on a board the team sees every day.
See LeanSuite on your changeovers and sanitation checks
Bring the routine you want to fix first. We will show you how LeanSuite handles it and what a 90-day pilot would cover.