

Lean playbook · Industrial and HVAC equipment
Lean playbook for industrial and HVAC equipment makers
Short answer
Lean works in high-mix, low-volume equipment plants when it starts with flow and first-time quality instead of speed. Map one product family to see where lead time goes, limit work in progress, write job breakdowns for complex builds, cross-train the stations only one person can run, and move checks upstream so leaks and wiring faults are caught before final test. Shortage logs and kitting stop the line waiting for parts.
Last updated:
7 problems on the floor, and the lean methods for each
Each problem says what it looks like, which methods address it, the first moves to make and the number to watch. Pick the one or two that cost your plant most; you do not need all of them at once.
Where a high-mix equipment assembly floor loses time and quality
Order release
Receiving, stores and kitting
Welding and brazing
Sub-assembly and final assembly
Final run and pressure test
Across the whole line
Long lead times in high-mix production
Many models and options in small batches mean units wait between operations far longer than they are worked on. Work in progress fills the floor and due dates are met by expediting.
In LeanSuite
AI value stream mapping from video: LeanSuite turns phone footage of each process step into a current-state value stream map with measured cycle times, counted inventory, the lead-time ladder and process cycle efficiency, then branches it into future-state scenarios you can compare and export.
First moves
- Map the value stream for one product family, from order to shipping, with the waiting time at each step.
- Set a limit on work in progress between the main operations and release work to the floor only when there is room.
- Level the mix of models released each day instead of building in large runs of one model.
Number to watch: Lead time from order release to shipping, and work in progress.
Complex assembly that lives in a few heads
A unit can take hundreds of steps, torque values and wiring checks. The real method lives with a few experienced assemblers, and instructions, if they exist, lag behind engineering changes.
In LeanSuite
Film the job once and LeanSuite drafts the work instruction with numbered steps, photos, tools, PPE and warnings from the video.
First moves
- Write job breakdown sheets for the builds with the most errors, with key points and the reasons for them.
- Add photos, torque values and test limits to each instruction and update it with every engineering change.
- Capture expert tips as one-point lessons and review them at shift start.
Number to watch: Build errors found at test, by station.
Stations only one person can run
Skilled assemblers, welders and test technicians take years to develop. When one is off or retires, a station stands idle or work goes to someone who has never done it.
Lean methods
In LeanSuite
The skills matrix shows jobs only one person can do, so you can schedule cross-training before that person is out.
First moves
- Build a skills matrix by station and mark every job fewer than three people can do.
- Plan cross-training for those jobs first, with sign-off by the expert.
- Review the matrix monthly and before planned absences and retirements.
Number to watch: Jobs with fewer than three trained people.
Rework after final test
Leaks, wiring faults and failed run tests at the end of the line send units back for rework, after panels are closed and more work has been added. The same failures repeat because the cause is not traced back to the station.
In LeanSuite
Each non-conformance is captured with photos and routed to quality and engineering.
First moves
- Pareto test failures by cause and by the station where the fault was made.
- Test sub-assemblies, such as refrigerant circuits or wiring harnesses, before they are closed in.
- Error-proof the top causes, for example connectors that only fit one way, and run root-cause analysis on the rest.
Number to watch: First pass yield at final test, and rework hours.
Quality of bought-in parts
Castings, motors, compressors, controls and sheet metal come from many suppliers. A bad lot found at final test costs far more than one caught at receiving.
Lean methods
In LeanSuite
Lean Creator runs inbound inspections with photos and pass/fail logic at the dock.
First moves
- Inspect the parts with the worst history at receiving, with a sampling plan.
- Send each key supplier a monthly scorecard on quality, delivery and response time.
- Raise a SCAR for repeat problems and track the supplier's response.
Number to watch: Supplier defects per million, and defects found at receiving against defects found later.
Assembly waiting for parts
A unit is started, then parked because one part is missing. Assemblers search the stores, and half-built units take up floor space.
Lean methods
In LeanSuite
Log lost production by cause, from breakdowns and changeovers to material shortages, and use it to fix maintenance and scheduling.
First moves
- Log every shortage with the part, the unit affected and the cause, and review it weekly with planning and purchasing.
- Kit the parts for each unit before it is released, so a shortage shows before work starts.
- Use two-bin kanban for hardware and consumables at the stations.
Number to watch: Line stops and parked units caused by missing parts.
Heavy lifts, welding and pressure testing
Heavy lifts, welding, brazing, pressure testing and machine servicing all carry serious risk. Near misses go unreported when reporting is a hassle, and lockout procedures go out of date.
In LeanSuite
Anyone can report a near miss by scanning a station QR code with their phone, anonymously if you allow it, and each hazard becomes a corrective action with a due date.
First moves
- Write a job safety analysis for lifting, pressure testing and other high-risk tasks, with the crew.
- Write machine-specific lockout procedures with a photo of every isolation point.
- Make near-miss reporting quick, and tell people what changed after each report.
Number to watch: Near misses reported and closed, and the recordable injury rate.
More small fixes in the production, quality and warehouse and logistics sections of the kaizen idea bank.
A 90-day starting plan
One line or product family, two problems, measured before and after. The point of the first 90 days is a result the plant believes and a method it can repeat, not a plant-wide program.
The 90 days, with the gate that ends each stage
- Days 1 to 30Map one product familyDone when: You have a current-state map, baseline numbers and two problems with owners.
- Days 31 to 60Fix flow and first-time qualityDone when: Each change has a before-and-after number and a written standard.
- Days 61 to 90Protect the skills and spread the methodDone when: The gains have held for a month and the next family has its map.
Days 1 to 30
Map one product family
See where lead time and quality are lost for one family of products.
- Choose the product family with the most late orders or the most rework, and name an owner.
- Map its value stream with the people who build it, with waiting time and inventory at each step.
- Measure for two weeks: lead time, work in progress, first pass yield at test and shortages.
- Start a short daily meeting at a board in the assembly area.
- Choose the two biggest losses to work on first.
Days 31 to 60
Fix flow and first-time quality
Attack the two problems and prove the change with numbers.
- Set a work-in-progress limit and release work only when there is room.
- Pareto test failures, move the top check upstream and error-proof one cause.
- Start the shortage log and kit the parts for the next units released.
- Write job breakdowns for the most error-prone build steps.
Days 61 to 90
Protect the skills and spread the method
Keep the gains, close single-person skills gaps and start the next family.
- Build the skills matrix and start cross-training on the jobs only one person can do.
- Audit the new standards and instructions on every shift.
- Draw the future-state map and agree the next steps with planning and purchasing.
- Share the results and start the next product family.
The KPIs to track
Track them per line and shift, on a board the team sees every day. Set targets from your own baseline, not from someone else's plant.
| KPI | What it tells you | How to measure it | Free help |
|---|---|---|---|
| Lead time | How long an order takes from release to shipping, and where it waits. | Date shipped minus date released, per unit, and the waiting time at each step from the value stream map. | Lead time calculatorLead time worksheet |
| Work in progress | How much is started but not finished, which drives lead time. | Count of units or kits between release and shipping, at the same time each day. | - |
| First pass yield at final test | The share of units that pass final test without rework. | Units passing first time divided by units tested, per model. | First pass yield (FPY) calculator |
| Cost of poor quality | What rework, scrap, warranty and extra testing cost. | Monthly total of rework hours, scrap, returns and extra inspection, costed. | Cost of poor quality (COPQ) calculatorCost of poor quality (COPQ) worksheet |
| On-time delivery | Whether customers get units when promised. | Orders shipped on or before the promised date divided by orders shipped. | - |
| Single-person skills | Where the plant depends on one person. | Jobs with fewer than three trained people, from the skills matrix. | Skills matrix template |
By the numbers
Public figures for this industry or for the wider sector it belongs to, each linked to the report or government table it comes from and checked against it on October 3, 2026. More in our lean manufacturing statistics and benchmark charts.
2.3
Machinery manufacturing recorded 2.3 injury and illness cases per 100 full-time workers in 2024, and ventilation, heating, air-conditioning and commercial refrigeration equipment manufacturing 2.4, against 2.7 for all manufacturing.
Total recordable cases per 100 full-time workers, U.S. private industry, 2024 data from the Survey of Occupational Injuries and Illnesses.
Source: U.S. Bureau of Labor Statistics, Table 1. Incidence rates of nonfatal occupational injuries and illnesses by industry and case types, 2024 (2024 data, table updated January 22, 2026)
16×
Plants in the top quarter for relying on reactive maintenance had 3.3 times more downtime and 16 times more defects than plants in the bottom quarter.
Same NIST survey. NIST notes the link is an association, not proof of cause.
Source: NIST, Economics of Manufacturing Machinery Maintenance: A Survey and Analysis of U.S. Costs and Benefits (NIST AMS 100-34) (June 2020)
Injury and illness rate by industry, 2024
- Motor vehicles5.6
- Beverage and tobacco3.7
- Furniture3.5
- Food3.3
- Primary metals3.3
- Nonmetallic mineral products, incl. glass3.3
- Fabricated metal products3.2
- Transportation equipment3.2
- Motor vehicle parts2.9
- Plastics and rubber products2.8
- HVAC and refrigeration2.4This industry
- Paper2.4
- Machinery2.3This industry
- All private industry2.3
- Electrical equipment and appliances2.0
- Printing1.6
- Chemicals1.6
Total recordable cases per 100 full-time workers, 2024: Motor vehicles 5.6, Beverage and tobacco 3.7, Furniture 3.5, Food 3.3, Primary metals 3.3, Nonmetallic mineral products, incl. glass 3.3, Fabricated metal products 3.2, Transportation equipment 3.2, Motor vehicle parts 2.9, Plastics and rubber products 2.8, All manufacturing 2.7, HVAC and refrigeration 2.4, Paper 2.4, Machinery 2.3, All private industry 2.3, Electrical equipment and appliances 2, Printing 1.6, Chemicals 1.6.
Free templates, calculators and buyer's guides
Templates (25)
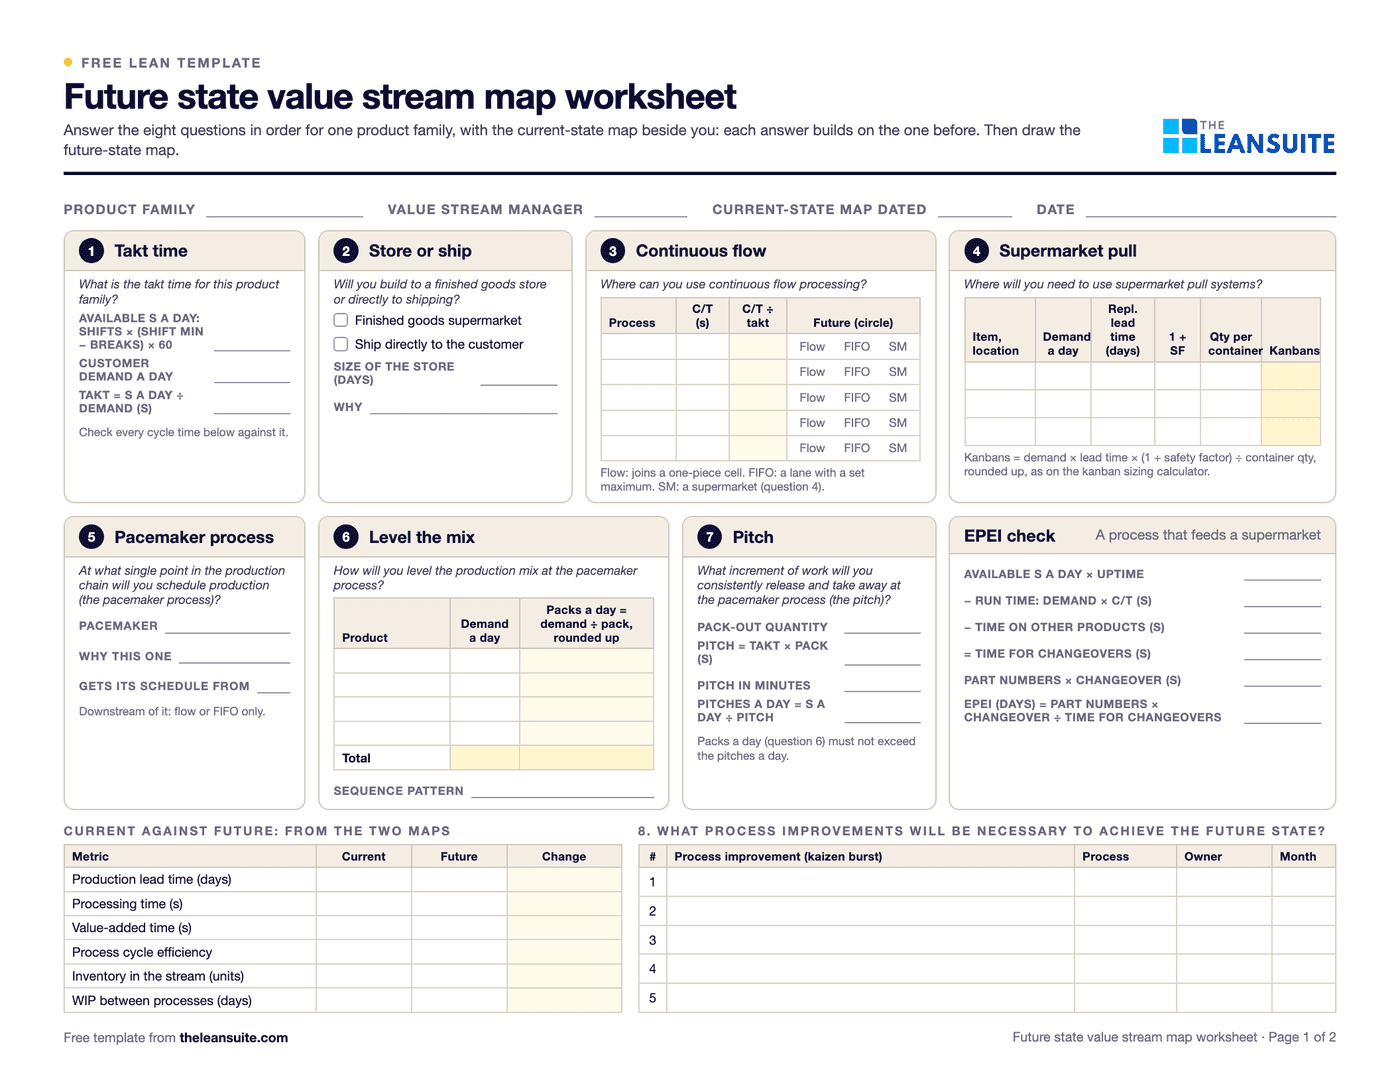 PDF and ExcelFuture state value stream map worksheetThe eight future-state questions worked through in order: takt, pitch, flow, supermarkets, the pacemaker and the mix, with an EPEI check and current against future lead time.
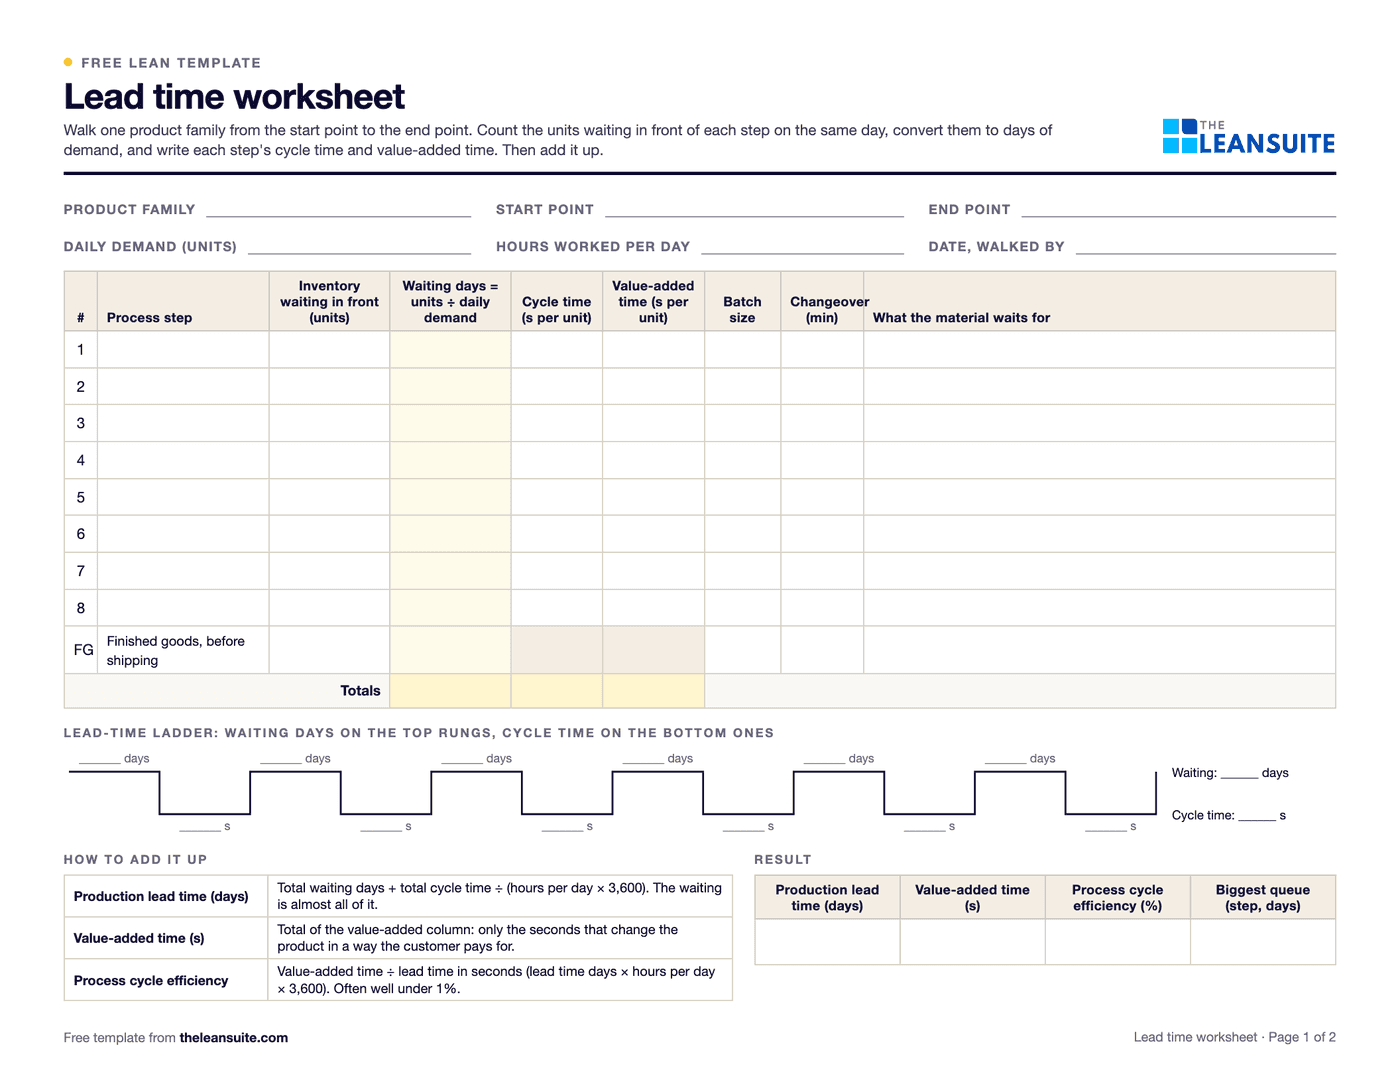 PDF and ExcelLead time worksheetProduction lead time from the inventory waiting at each step, value-added time and process cycle efficiency, plus an order traced from order to delivery.
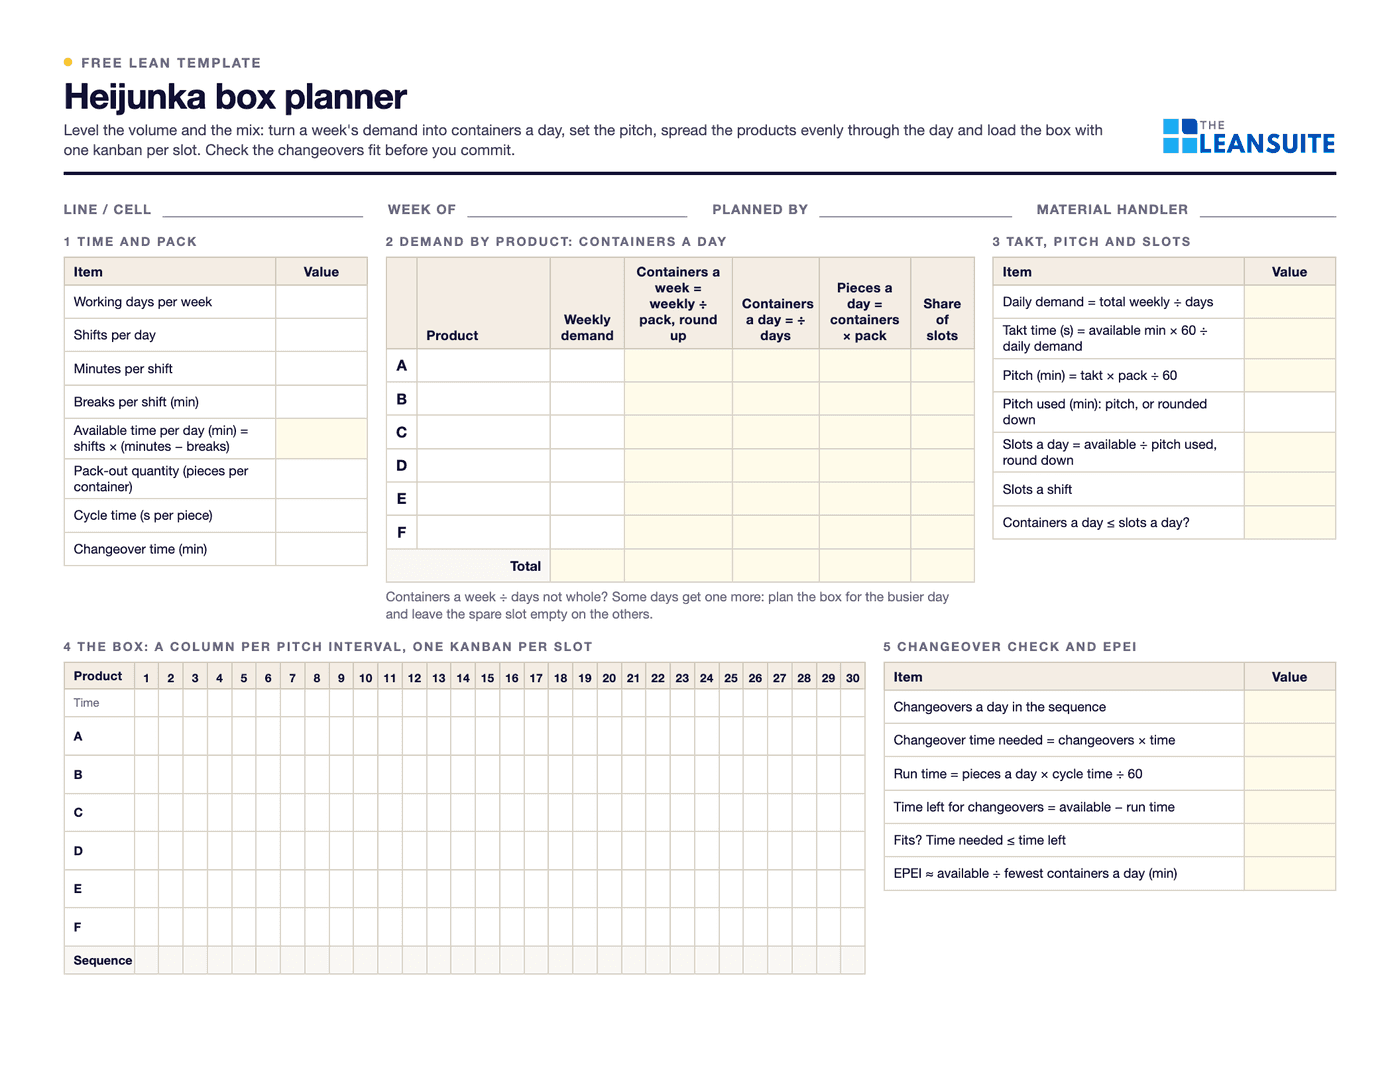 PDF and ExcelHeijunka box planner (production leveling)Weekly demand turned into containers a day, takt, pitch and slots, a leveled sequence of products and the heijunka box, with a check that the changeovers fit.
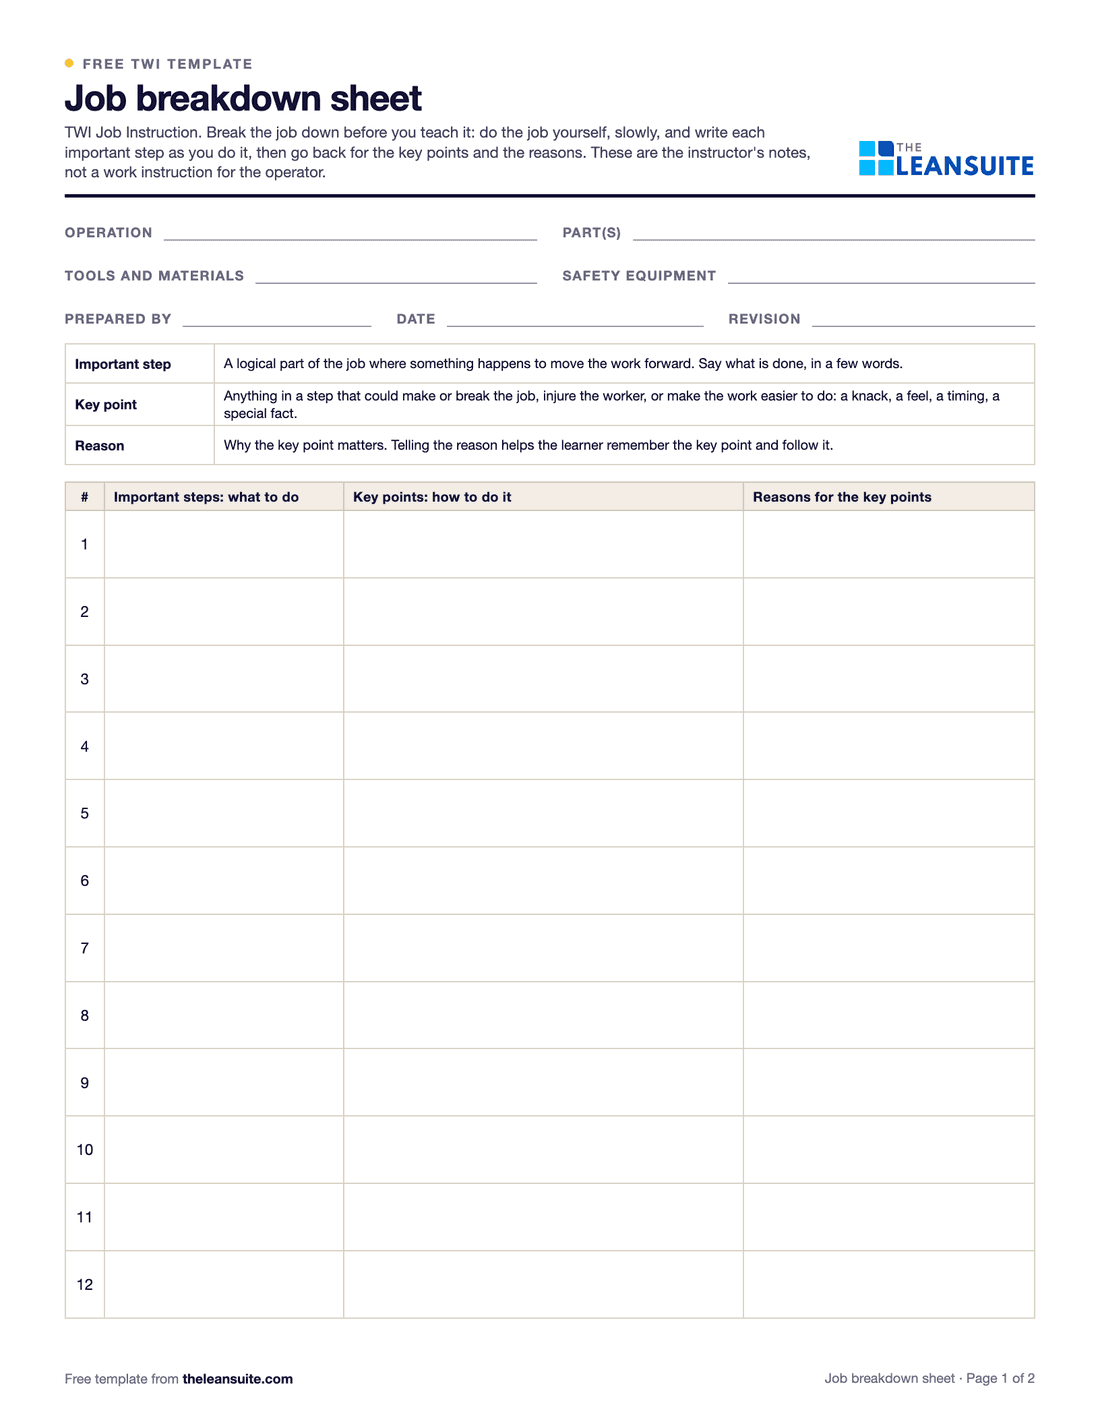 PDF and ExcelTWI job breakdown sheetThe TWI Job Instruction breakdown of a job into important steps, key points and reasons, with a worked example and the four steps.
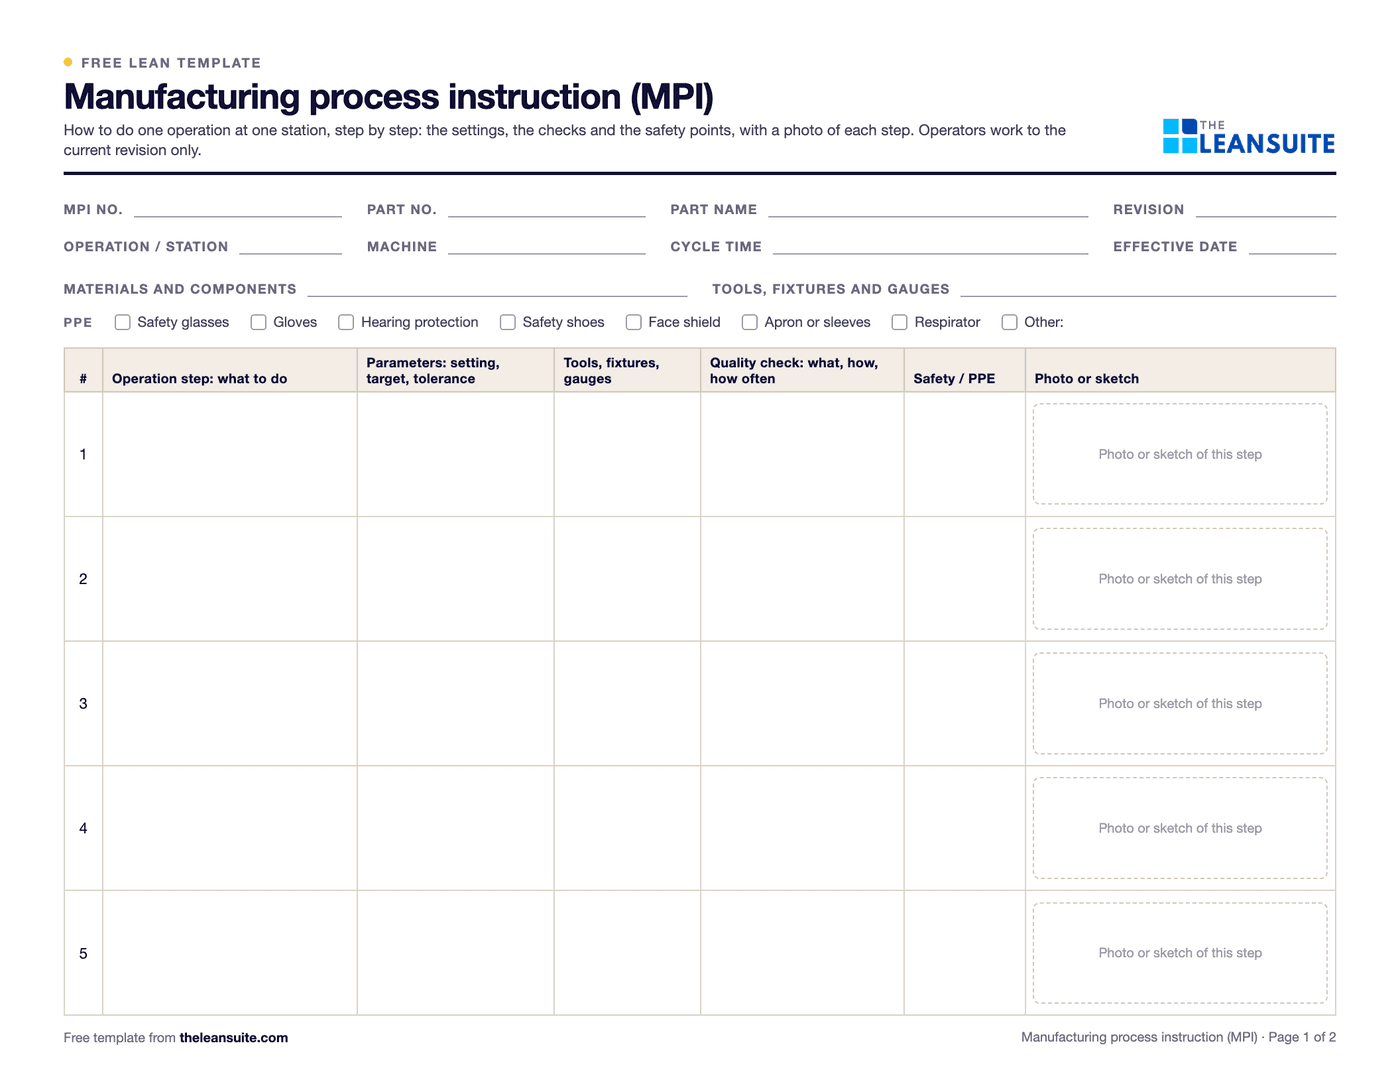 PDF and ExcelManufacturing process instruction (MPI) templateOperation steps with parameters, tools, quality checks, safety and a photo each, plus revision history and approval.
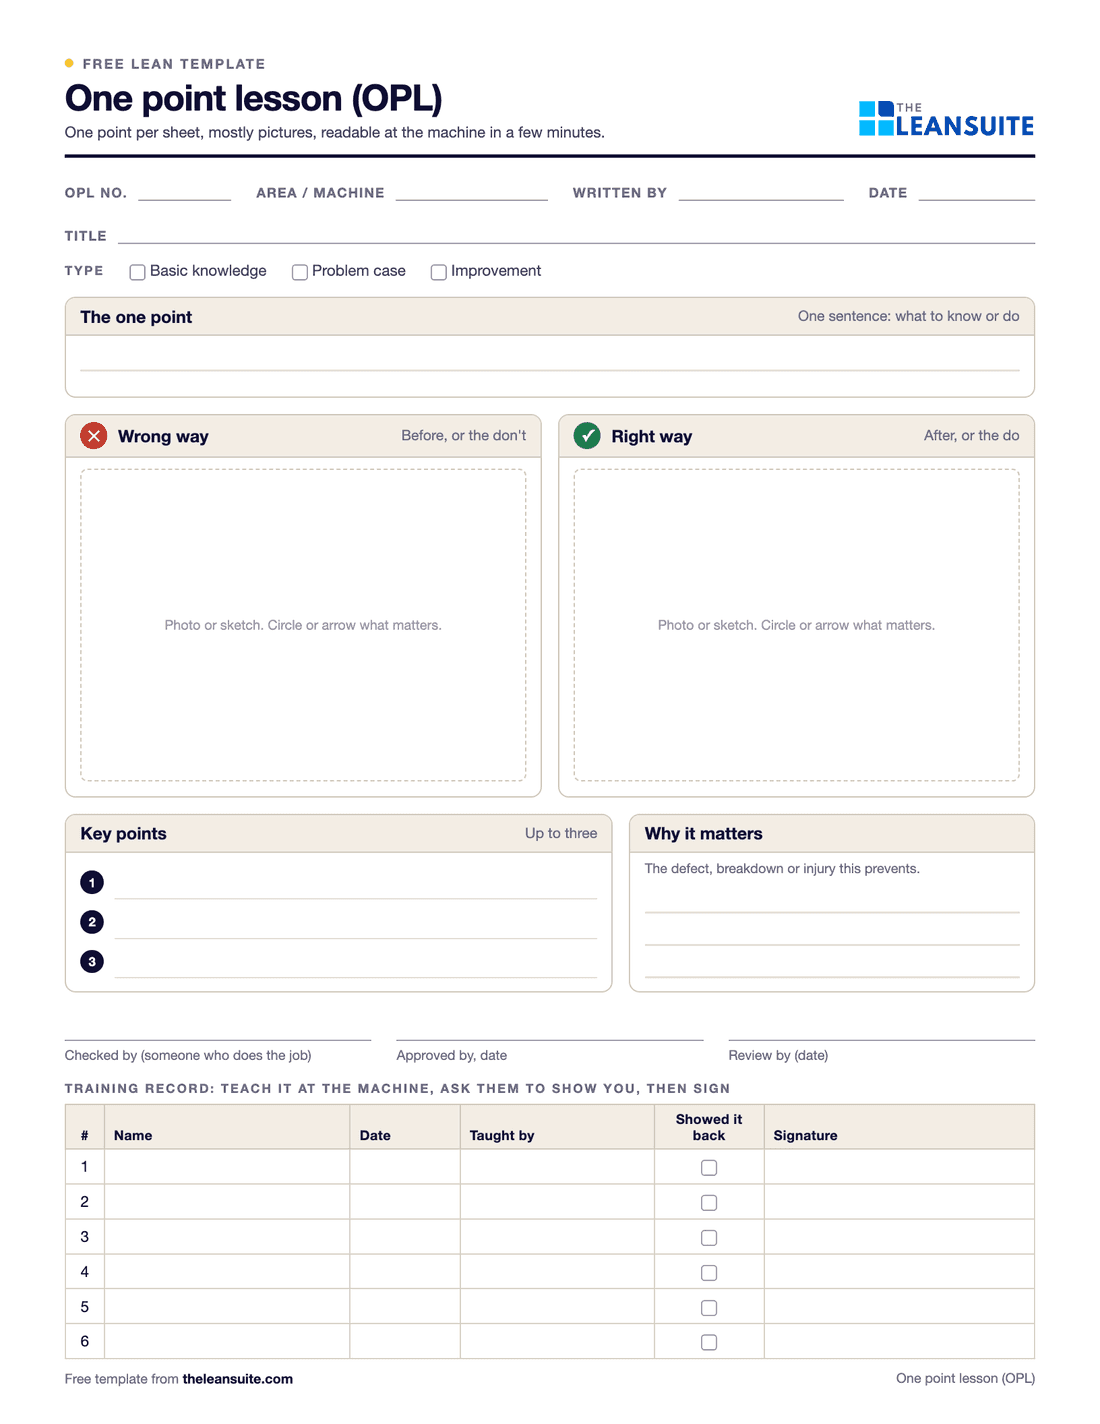 PDF and Excel and WordOne point lesson (OPL) templateOne topic on one page: wrong way and right way pictures, checkable key points, the standard it belongs to and a sign-off record.
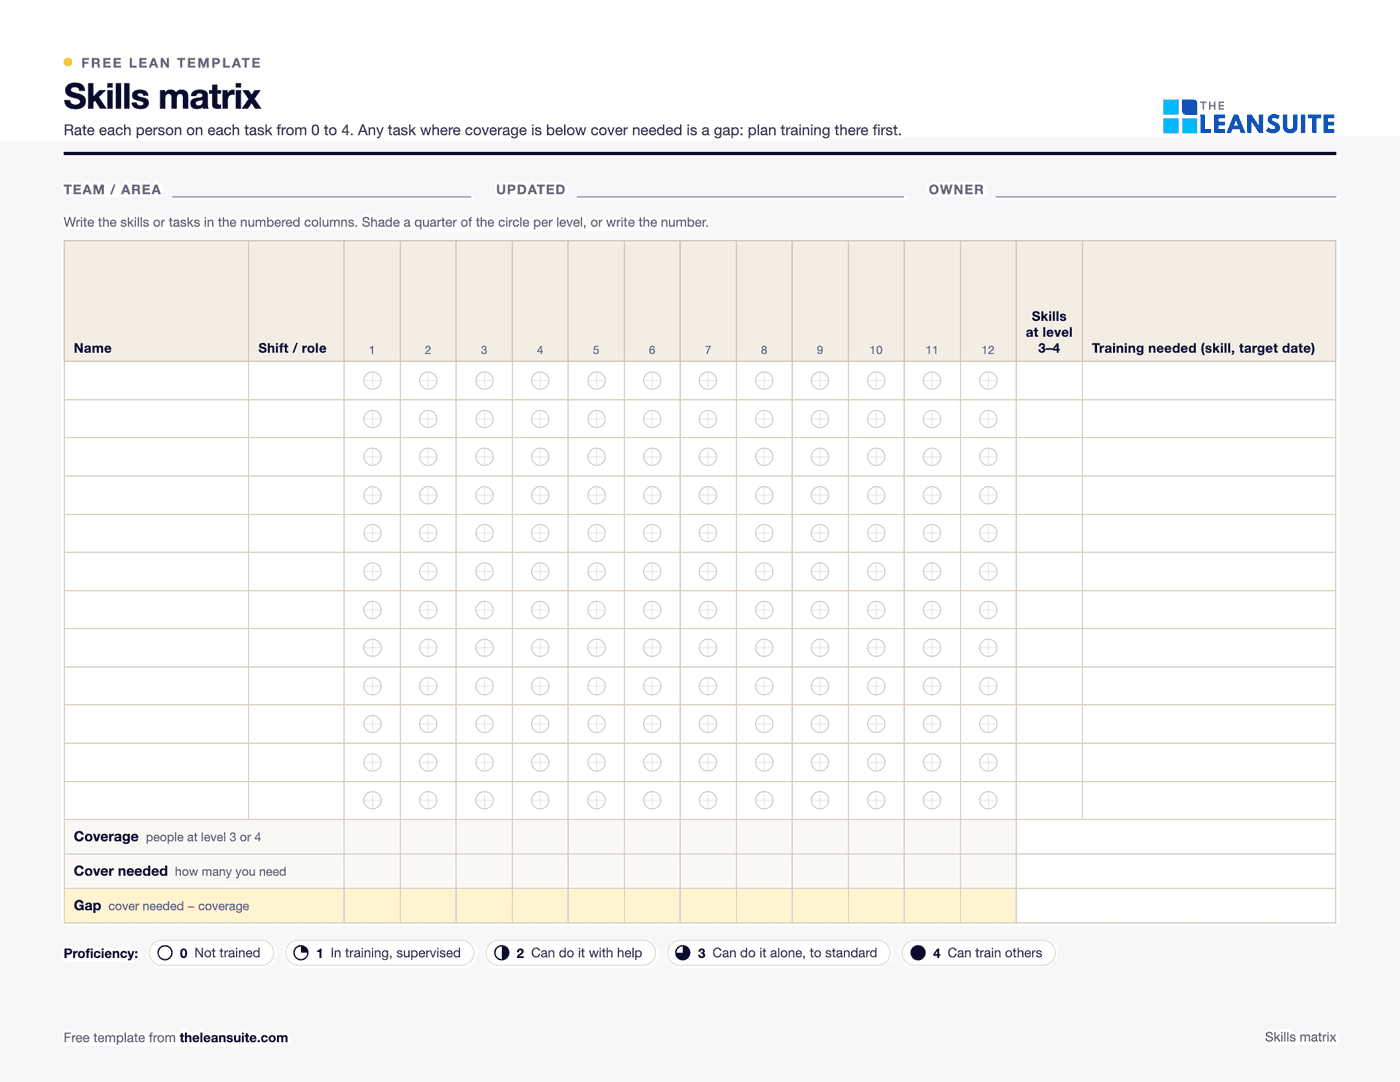 PDF and ExcelSkills matrix templatePeople by tasks on a 0 to 4 scale, coverage and gaps per task and shift, and a training plan that closes them.
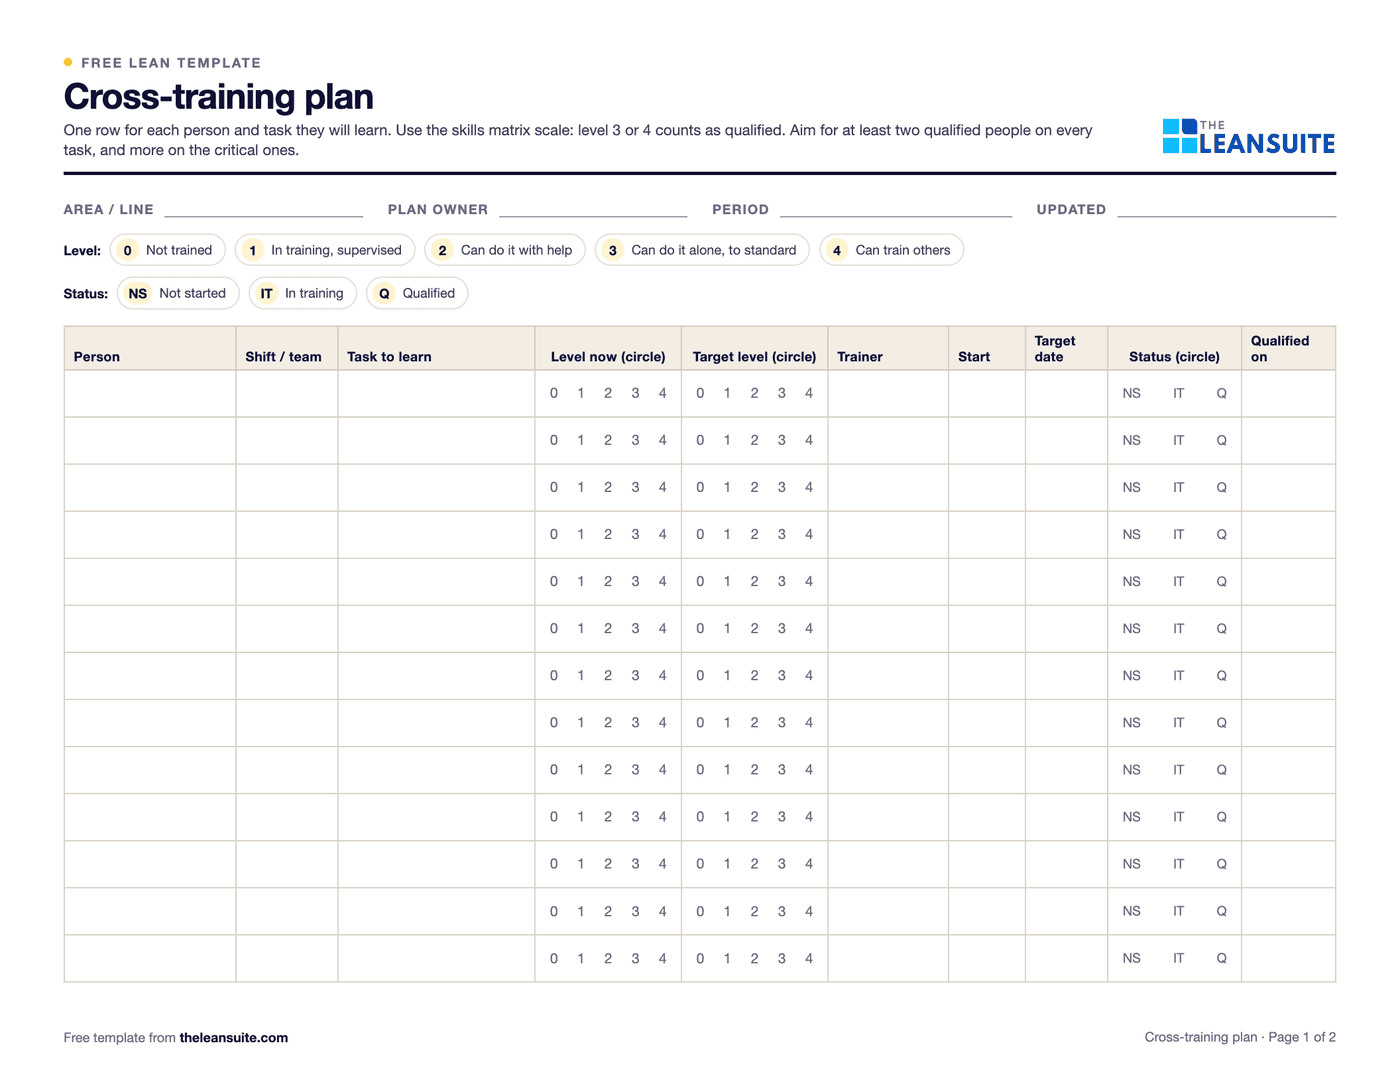 PDF and ExcelCross-training plan templateWho is learning which task, from and to which level, by when, and how many are qualified on each task.
 PDF and ExcelCompetency assessment formThe one-person assessment behind a skills matrix rating: each task rated 0 to 4 from evidence, checked, with a training plan for every gap.
 PDF and ExcelTraining matrix template with expiry datesPeople by required trainings with expiry dates, OK, due, expired and missing flags, compliance by person and area, cover per training and a renewal list.
 PDF and ExcelPareto chart templateA tally sheet, the Pareto by count and by cost with the cumulative line and the 80 percent threshold, and a before and after comparison. Excel sorts and draws it.
 PDF and ExcelDefect check sheetTally defects by type and day, with units inspected, defect rates, a location sheet and the week's Pareto.
 PDF and ExcelPoka-yoke worksheetEach step's errors and what they cost, the device (approach, function, method), payback, and a log that proves each device works.
 PDF and ExcelRoot cause analysis templateOne report from problem statement to proof: containment, evidence, analysis, verified causes, actions and the effectiveness check.
 PDF and ExcelDefect catalogue template with boundary samplesEvery defect with a definition, a class and the reason for it, measured accept and reject limits by zone, boundary samples, a defect log with DPU and Pareto, and an inspector agreement check.
 PDF and ExcelIncoming inspection checklistReceiving inspection checks from paperwork to sample, the sampling plan, the decision, and an Excel log by supplier.
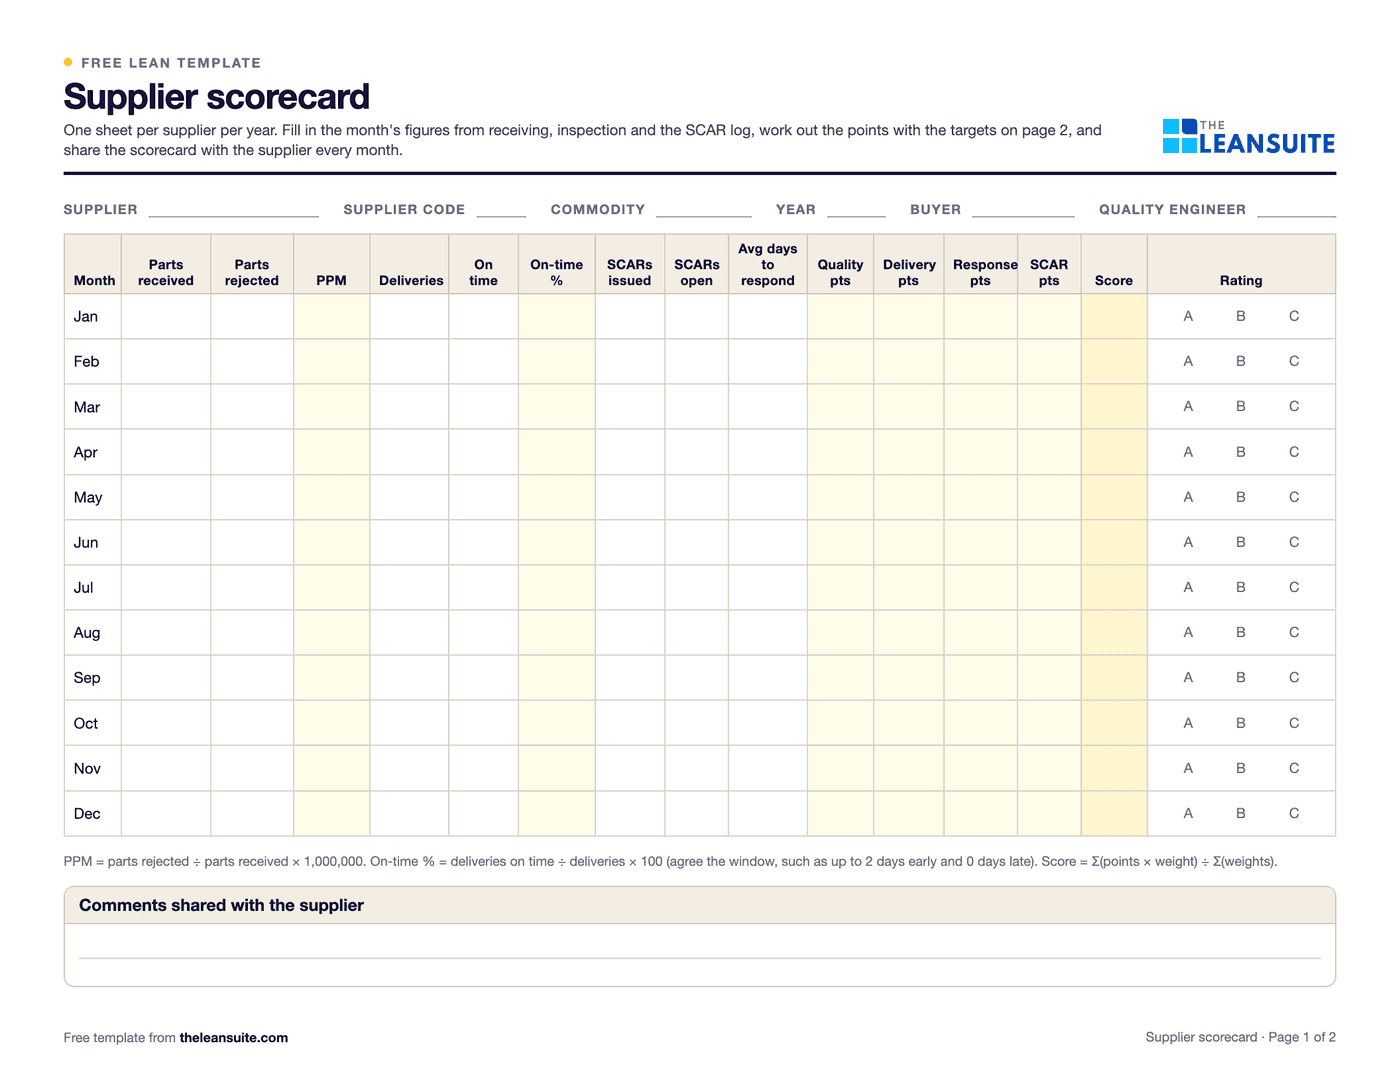 PDF and ExcelSupplier scorecardMonthly PPM, on-time delivery and SCAR measures turned into points, a weighted score and a rating per supplier.
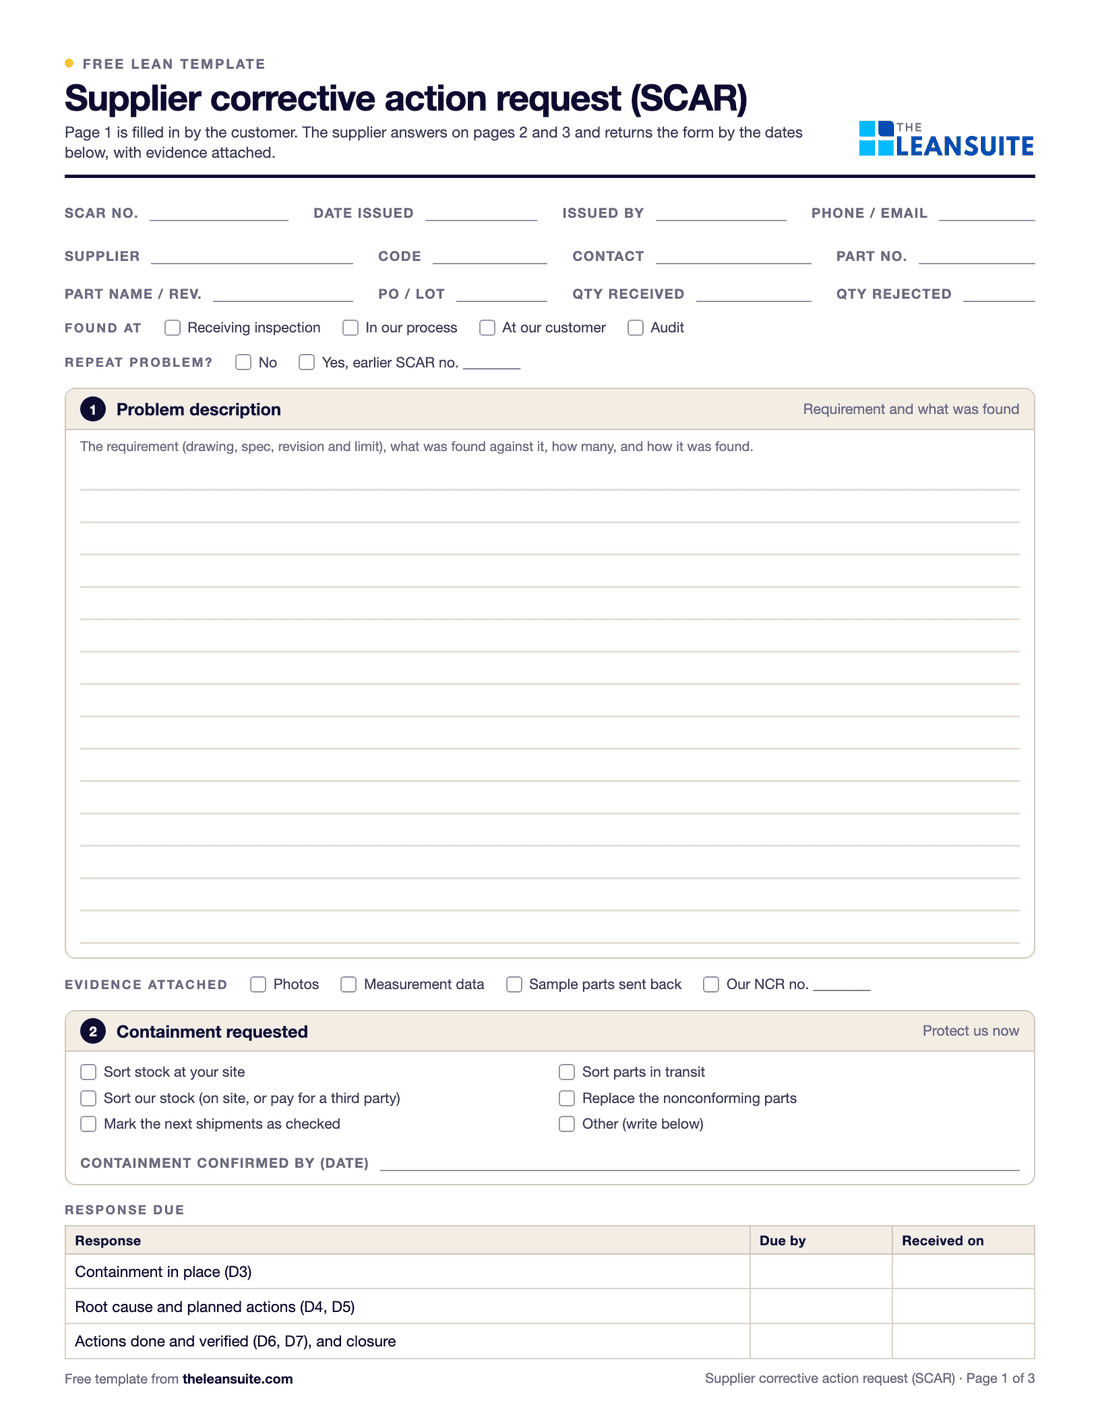 PDF and WordSupplier corrective action request (SCAR) formA SCAR from the problem and containment asked for to the supplier's 8D-style response, verification and closure, with a filled-in example.
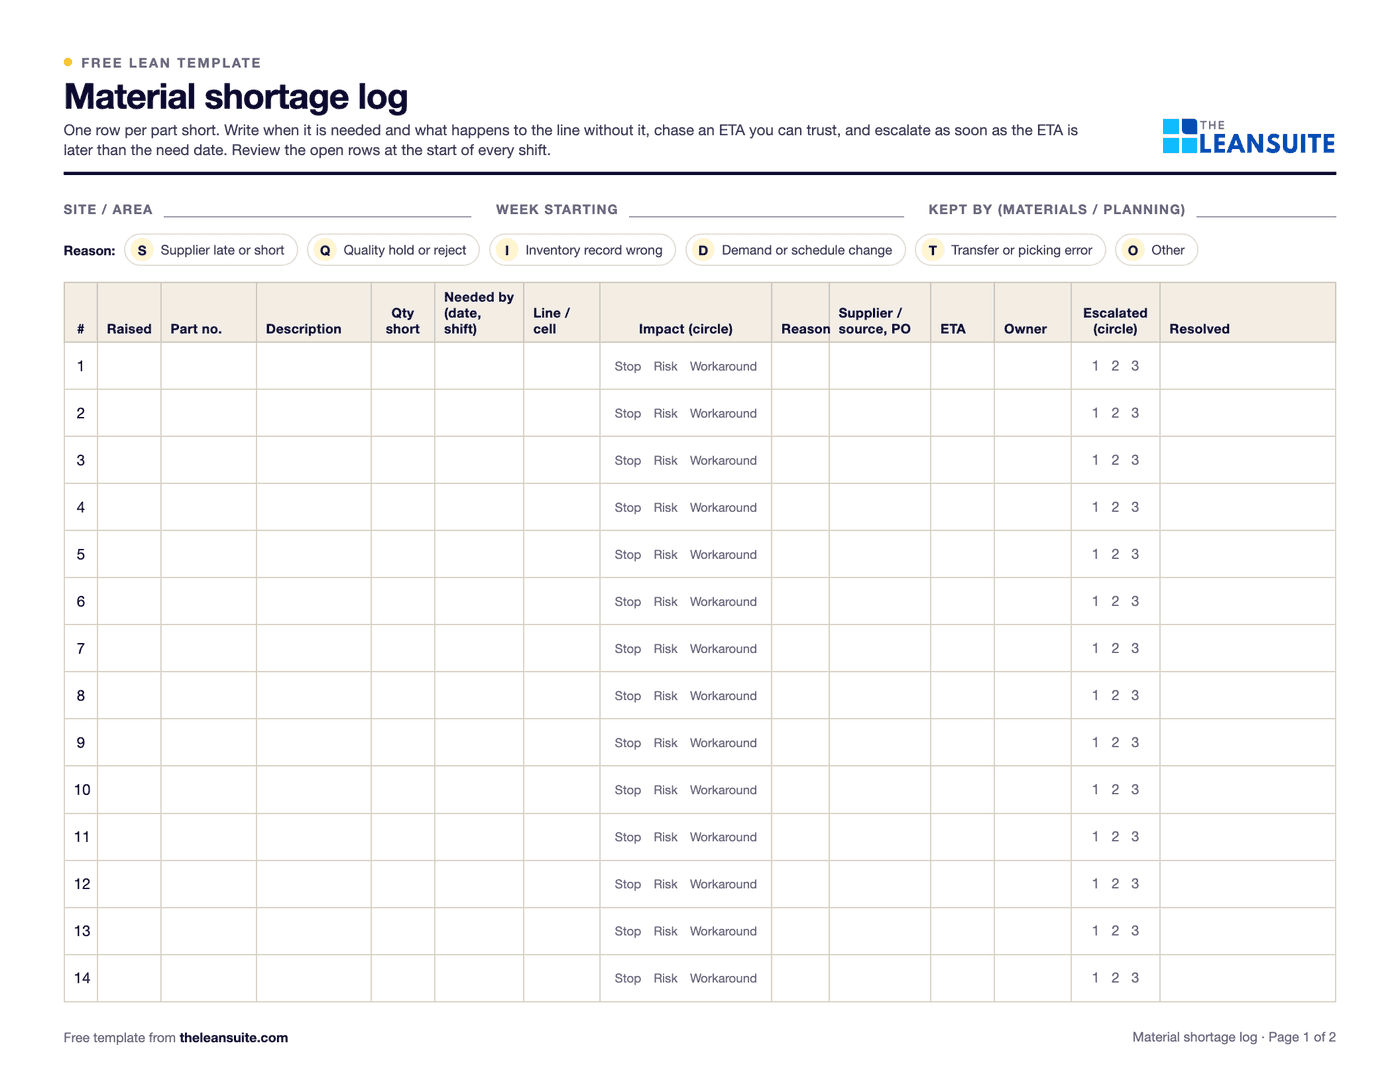 PDF and ExcelMaterial shortage logEvery part short with its need date, line impact, ETA and escalation, and counts by reason and supplier.
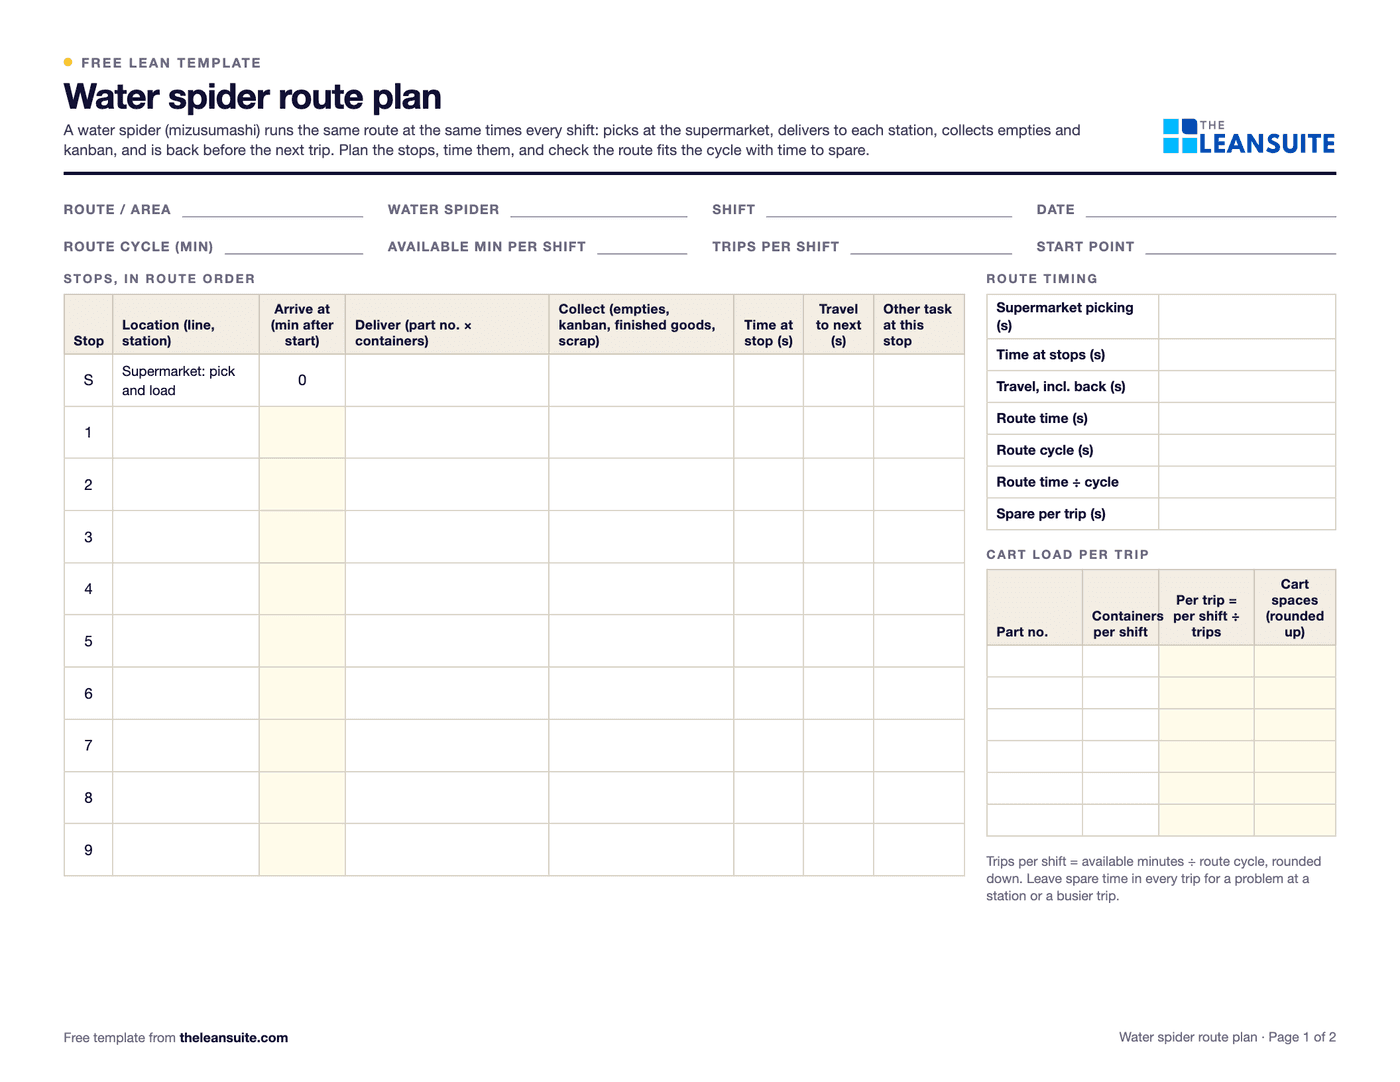 PDF and ExcelWater spider route plan (mizusumashi)A water spider's fixed route: stops with arrival times, what is delivered and collected, route time against the cycle, cart load and a trip log.
 PDFKanban card templateSix production and six withdrawal kanban cards to print and cut out, with loop sizing and a card register.
 PDF and Excel and WordJob safety analysis (JSA) templateJob steps, hazards, risk scored before and after the controls, the hierarchy of controls, PPE and sign-off.
 PDF and ExcelLockout/tagout (LOTO) procedure templateA machine-specific LOTO procedure: energy sources and isolation points, the steps from shutdown to restart, and the annual review.
 PDF and ExcelNear miss report formA two-page near miss report from the first report to closure, and an Excel log with status and days open.
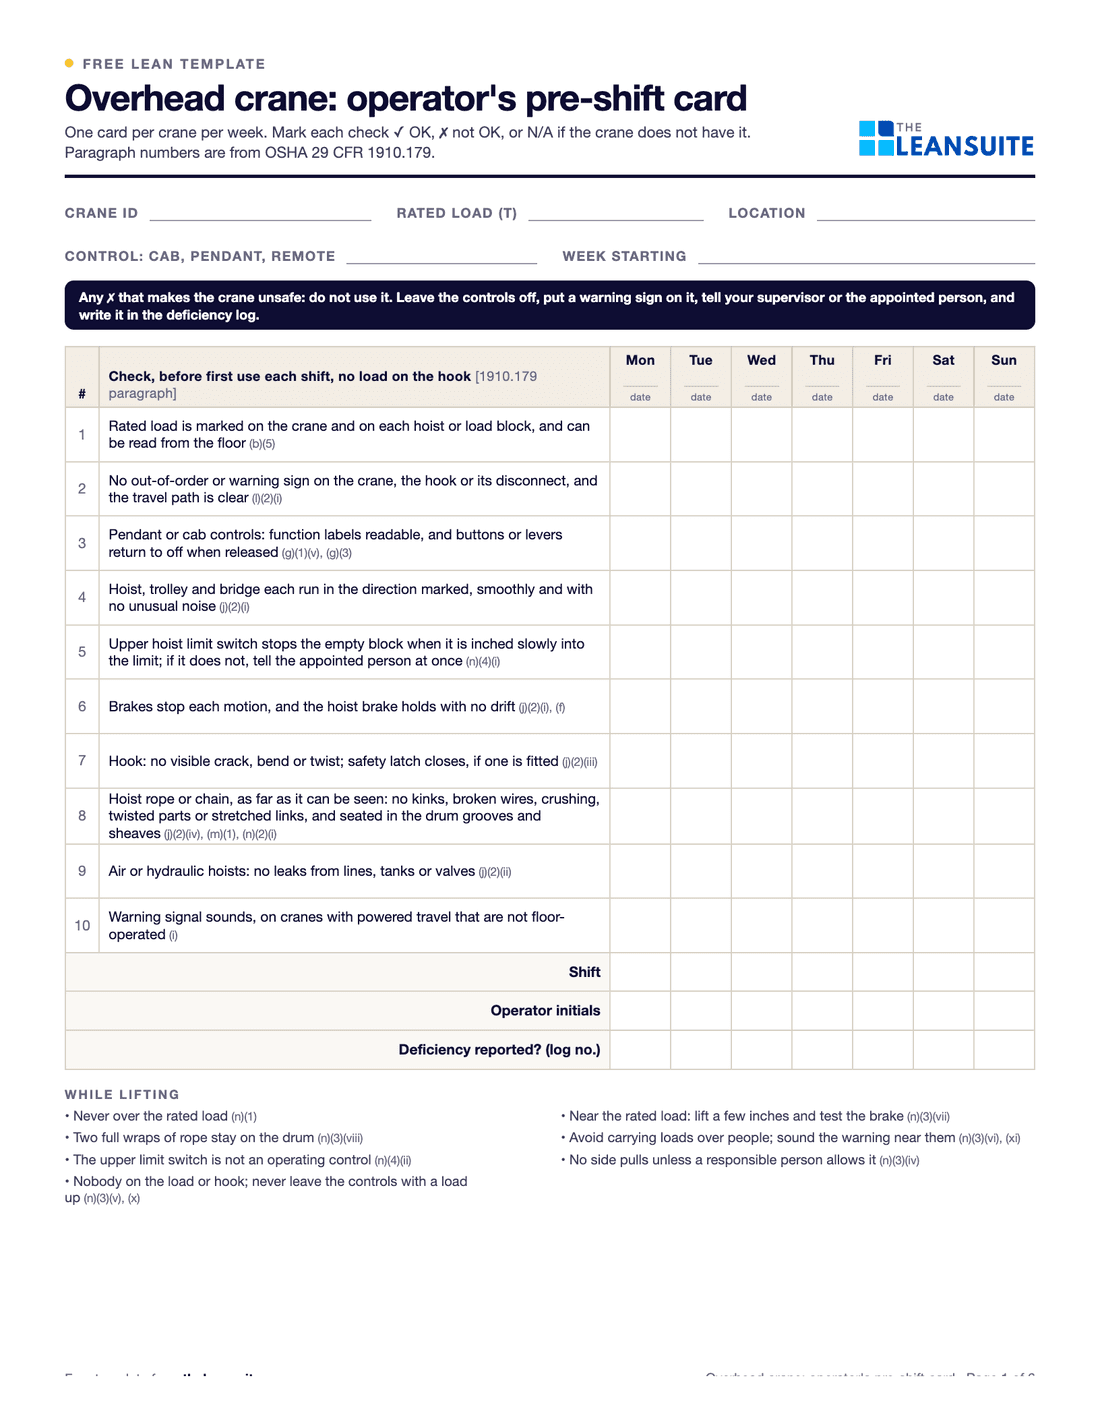 PDF and ExcelOverhead crane inspection checklist: frequent and periodic34 crane checks tied to OSHA 1910.179: an operator's pre-shift card, frequent and periodic inspections with signed records, a deficiency and tag-out log, and a register of next due dates.
Calculators (4)
- Free calculatorLead time calculatorManufacturing lead time from WIP and throughput (Little's Law), and the share of it that adds value.
- Free calculatorThroughput time calculatorThroughput time from process, inspection, move and wait time, the share of it that adds value, and units per hour.
- Free calculatorFirst pass yield (FPY) calculatorFirst pass yield at each step and rolled throughput yield (RTY) across the whole process.
- Free calculatorCost of poor quality (COPQ) calculatorTotal COPQ and cost of quality, and each as a share of revenue, from the four quality cost categories.
Buyer's guides
LeanSuite pages for these problems
- Document Builder
- SMED
- Digital Work Instructions
- AI SOPs
- AI OPL
- Cross Training
- Competency Management
- Job Cover Matrix
- Supplier Quality
- Non-Conformance (NCR)
- AI Root Cause Analysis
- Near Miss Reporting
- Lockout/Tagout (LOTO)
How LeanSuite handles each of these is on the page for industrial and HVAC equipment plants.
FAQ
Lean in industrial and HVAC equipment plants: common questions
Yes, but the focus shifts from takt and speed to flow, lead time and first-time quality. Map one product family, limit work in progress, level the mix you release, standardize the build steps that cause most errors and catch faults before final test.
With one product family that is often late or often reworked. Map its value stream with the people who build it, measure lead time, work in progress and first pass yield at test for two weeks, and fix the two biggest losses before moving on.
Write job breakdown sheets with them for the critical and error-prone steps, including the reasons behind each key point, add photos and torque values, and use a skills matrix to plan cross-training on every job fewer than three people can do.
Lead time, work in progress, first pass yield at final test, cost of poor quality and on-time delivery, plus the number of jobs only one or two people can do. Track them per product family.
See LeanSuite on your assembly floor
Bring the routine you want to fix first. We will show you how LeanSuite handles it and what a 90-day pilot would cover.