

Free template
Updated
SSOP template: sanitation standard operating procedure
A sanitation standard operating procedure (SSOP) is the written method for cleaning and sanitizing one area or machine in a food plant. It says what is done in what order, with which chemical, strength and contact time, by whom and how often, and how the result is checked before start-up. In the US, meat and poultry plants inspected by USDA FSIS must keep written Sanitation SOPs under 9 CFR 416.11 to 416.17. FDA requires an SSOP of juice processors (21 CFR 120.6) and recommends one to seafood processors (21 CFR 123.11). Other FDA plants write them as the procedures behind the sanitary operations of 21 CFR 117.35, and behind the sanitation controls of 117.135(c)(3) where the food safety plan needs them. This template has three parts: one SSOP sheet per area or machine (the eleven cleaning steps, chemicals, PPE, lockout points, owner and time allowed), a 23-check pre-op inspection, and a verification log for visual, ATP, allergen and micro checks with the correction for every fail. The worked example is a beverage filler that passes its visual check and fails one ATP swab. A master sanitation schedule says when each task is done; the SSOP says how. It is a working aid, not legal advice, and it does not replace your validated chemical instructions or your food safety plan.
Free to use: print it, copy it and edit it for your team. Enter your name and work email once to download.
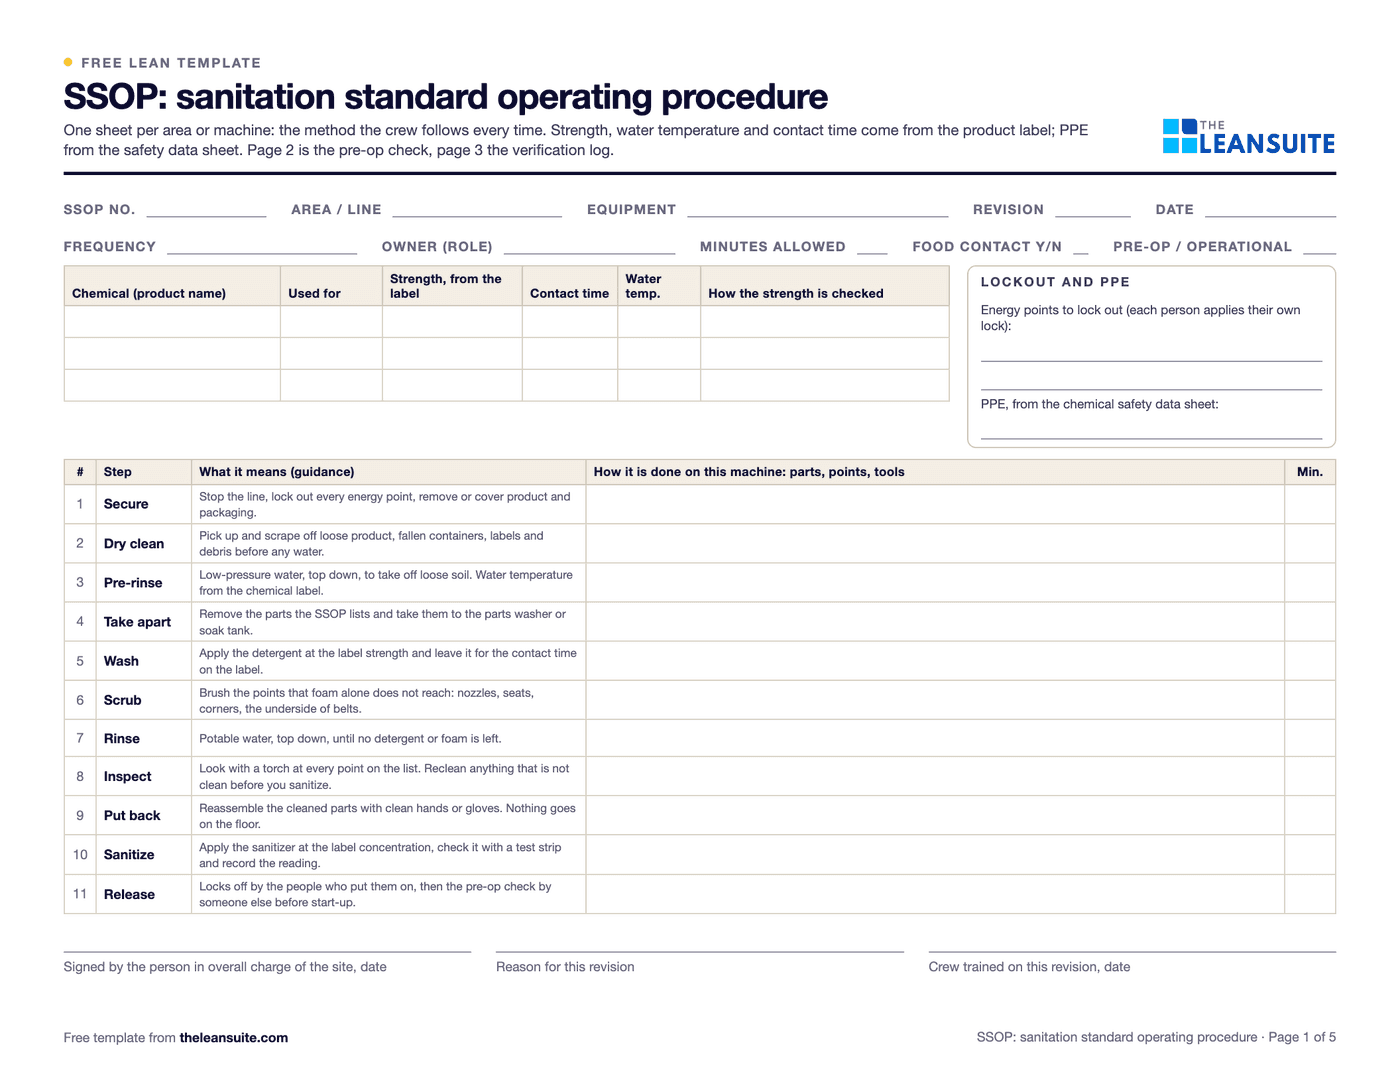 SSOP number, area and equipment, frequency, owner and sign-off fields, a lockout and PPE box, a chemicals table and the eleven cleaning steps from secure to release with space for how each is done on this machine.
When to use it
When to use an SSOP template
- When you write or rewrite the cleaning method for a machine or area, so every crew on every shift cleans it the same way.
- When a USDA-inspected meat or poultry plant needs written Sanitation SOPs under 9 CFR 416, or an FDA plant needs written sanitation procedures behind its food safety plan.
- Every production day, for the pre-op inspection that releases a line after cleaning.
- After a failed swab, a positive environmental result or an allergen incident, to find the step that did not work and change it.
- Not as the plan of what is cleaned when: that is the master sanitation schedule, which points to an SSOP number for each task.
How to fill it in
- 1
Write one SSOP per area or machine
A filler, a slicer, a mixer room. One sheet the crew can follow at the machine beats one plant-wide procedure nobody can. Give each an SSOP number and say whether it is a pre-op or an operational procedure.
- 2
Fill in the sequence with your own details
The sheet lists the eleven steps from secure to release. For each, write what is done on this machine: the parts to take off, the points that need a brush. Take the chemical, its strength, water temperature and contact time from the product label, and the PPE from its safety data sheet.
- 3
Put lockout in the procedure
Name every energy point to lock out, and say that each person working on the machine applies their own lock. OSHA's lockout rule (29 CFR 1910.147) counts cleaning as servicing.
- 4
Name who and how often, then sign it
A role, not a department, the frequency and the time allowed. In an FSIS plant the person in overall charge signs and dates the SSOP when it is first used and after every change (9 CFR 416.12). Doing the same in an FDA plant costs nothing.
- 5
Inspect before every start-up
Someone other than the person who cleaned works through the 23 pre-op checks with a torch, then takes the swabs the plan calls for. Nothing runs until every failed point is recleaned and passes.
- 6
Act on every fail, then fix the procedure
Write the correction, what happened to any product, and the recheck result. If the same point fails twice, the method is wrong: change the SSOP, sign the new revision and train the crew on it.
The cleaning sequence
Eleven steps from secure to release
Every SSOP sheet follows the same order. What changes from machine to machine is how each step is done: the parts to take off, the points to brush, the chemical and its strength.
- 1 to 3Secure, dry clean, pre-rinseLock out, take product and packaging away, remove loose soil before any water, then rinse top down.
- 4 to 7Take apart, wash, scrub, rinseParts to the soak tank, detergent at the label strength and contact time, brush what foam does not reach, rinse.
- 8 to 10Inspect, put back, sanitizeTorch on every listed point, reclean what fails, reassemble, sanitize and check the strength with a test strip.
- 11ReleaseLocks off by the people who put them on, then the pre-op check and swabs by someone who did not clean.
The rules, in plain words
What US rules ask of sanitation SOPs
Named and paraphrased from the eCFR (current as of 29 October 2026), never quoted. Check the rule that applies to your plant, and your state or country rules outside the US.
| Rule | Who it applies to | What it asks for |
|---|---|---|
| 9 CFR 416.11 to 416.17 (USDA FSIS) | Meat and poultry plants under federal inspection | Written SSOPs for the daily procedures before and during operations. Pre-op procedures marked as such, covering at least food-contact surfaces. Frequency and the person responsible named. Signed and dated by the person in overall charge at first use and after any change. Monitored daily, kept effective, corrective action that covers the product. Daily records initialled and dated, kept at least 6 months. |
| 21 CFR 120.6 (FDA) | Juice processors | An SSOP covering the eight key sanitation conditions before, during and after processing, monitored often enough, with records of the monitoring and corrections. |
| 21 CFR 123.11 (FDA) | Fish and fishery product processors | A written SSOP is recommended. Monitoring of the same eight conditions and records of monitoring and corrections are required. |
| 21 CFR 117.35 (FDA) | Food plants under the FDA food CGMP rule | Plant kept clean and in repair. Food-contact surfaces cleaned and sanitized as often as needed to prevent contamination and allergen cross-contact. Cleaning chemicals safe for the use and stored apart from food. |
| 21 CFR 117.135(c)(3), 117.145, 117.150(c) | Facilities whose food safety plan needs sanitation controls | Written sanitation controls for food-contact surfaces and for preventing cross-contact and cross-contamination, written monitoring at a set frequency, and timely corrections recorded. These controls do not need validation (117.160(c)). |
9 CFR 416.11 to 416.17 (USDA FSIS)
- Who it applies to
- Meat and poultry plants under federal inspection
- What it asks for
- Written SSOPs for the daily procedures before and during operations. Pre-op procedures marked as such, covering at least food-contact surfaces. Frequency and the person responsible named. Signed and dated by the person in overall charge at first use and after any change. Monitored daily, kept effective, corrective action that covers the product. Daily records initialled and dated, kept at least 6 months.
21 CFR 120.6 (FDA)
- Who it applies to
- Juice processors
- What it asks for
- An SSOP covering the eight key sanitation conditions before, during and after processing, monitored often enough, with records of the monitoring and corrections.
21 CFR 123.11 (FDA)
- Who it applies to
- Fish and fishery product processors
- What it asks for
- A written SSOP is recommended. Monitoring of the same eight conditions and records of monitoring and corrections are required.
21 CFR 117.35 (FDA)
- Who it applies to
- Food plants under the FDA food CGMP rule
- What it asks for
- Plant kept clean and in repair. Food-contact surfaces cleaned and sanitized as often as needed to prevent contamination and allergen cross-contact. Cleaning chemicals safe for the use and stored apart from food.
21 CFR 117.135(c)(3), 117.145, 117.150(c)
- Who it applies to
- Facilities whose food safety plan needs sanitation controls
- What it asks for
- Written sanitation controls for food-contact surfaces and for preventing cross-contact and cross-contamination, written monitoring at a set frequency, and timely corrections recorded. These controls do not need validation (117.160(c)).
Food plant sanitation checklist
The 23 pre-op checks on the SSOP template
Five groups, from before cleaning starts to the release of the line. On the sheet each check is Pass, Fail or N/A, done by someone other than the person who cleaned; every fail gets a correction and a recheck before start-up.
Before cleaning starts
Done by the sanitation crew, checked at pre-op
- 1Product, ingredients and packaging are removed from the area or covered, so nothing is sprayed or splashed onto them.
- 2The equipment is locked out at every energy point named on the SSOP, and each person working on it has applied their own lock.
- 3Every chemical is in a labelled container, is the one the SSOP names for this job, and was diluted or dosed as the SSOP says.
- 4The crew wears the PPE the SSOP and the chemical's safety data sheet call for: eye protection, gloves, apron and boots as listed.
- 5Floor drains in the area are uncovered and running, so wash water does not pool under the equipment.
Food-contact surfaces
Look with a torch, at the hard-to-reach points first
- 6No visible soil, product residue, film, scale or rust on any food-contact surface.
- 7Gaskets, seals, O-rings and valve seats are clean, in place and not cracked or torn.
- 8The hard-to-reach points the SSOP lists (nozzles, under guards, inside chutes, hinge points) are clean.
- 9Belts, star wheels, guides and change parts are clean on both sides, including the underside of belts.
- 10Utensils, scrapers and hand tools are clean, sanitized and stored off the floor in their marked place.
- 11The sanitizer was applied to food-contact surfaces at the concentration the SSOP gives, checked with a test strip or kit and recorded.
Equipment and area
Non-food-contact surfaces, overhead and floor
- 12Frames, legs, guards, motor housings and control panels are clean, with no build-up that could drop onto product.
- 13No loose parts, tools, rags, tape, brushes, nuts or bolts are left on or in the equipment.
- 14Overhead structures over exposed product show no condensation, dripping, peeling paint or flaking.
- 15Floors and drains around the equipment are clean, with no standing water or debris.
- 16Hand-wash sinks and sanitizer stations in the area are stocked and working.
- 17No sign of pest activity in the area: droppings, insects, gnawing or nesting.
Changeover and allergens
Only where the last run had an allergen or the next run is allergen-free
- 18Where an allergen ran last, no visible residue on any surface in the product path, checked at the points the SSOP lists.
- 19Where the site uses an allergen swab or kit, it was taken at the listed points and the result is recorded.
Verification and release
By someone other than the person who cleaned
- 20Every swab the plan calls for today (ATP or other) is within the site's limit at the first check.
- 21Every guard and cover is back in place, and each lock was removed by the person who applied it.
- 22Any failed item was recleaned, rechecked and passed before the line was released, and the correction is written down.
- 23The pre-op record is initialled and dated by the person responsible, with the release time.
A filled-in example
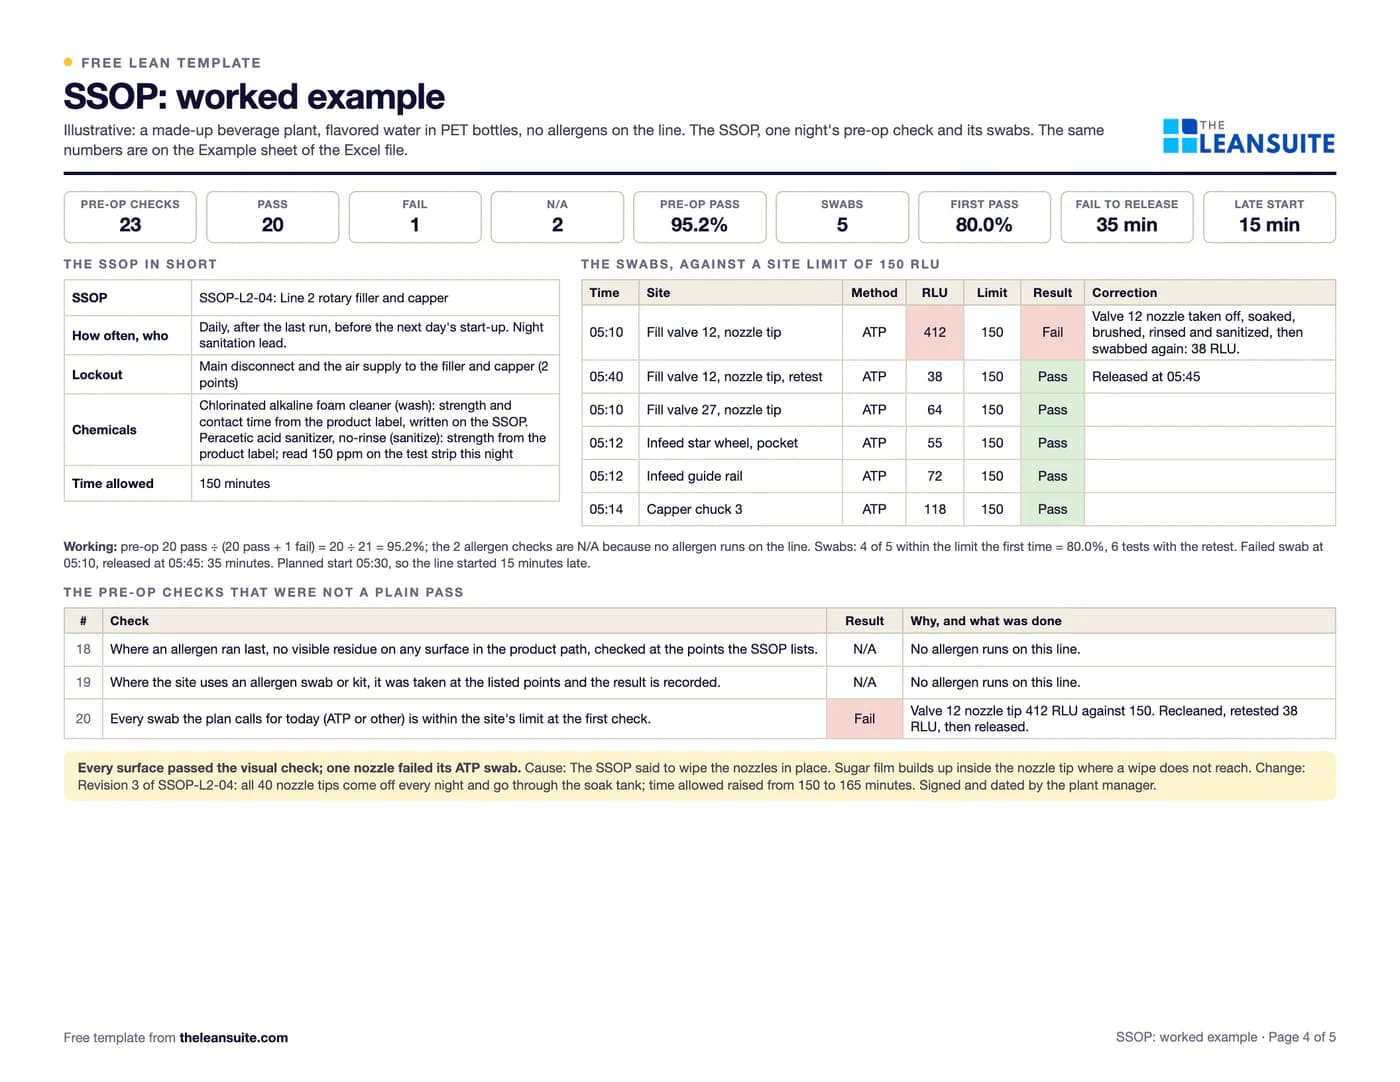
Illustrative, not a benchmarkAn example (illustrative): a made-up beverage plant bottling flavored water in PET, with no allergens on the line. SSOP-L2-04 covers the line 2 rotary filler and capper, cleaned every night by the night sanitation crew.
The five ATP swabs at pre-op, against the site limit
- Fill valve 12, nozzle tip412fail, retest 38
- Fill valve 27, nozzle tip64pass
- Infeed star wheel, pocket55pass
- Infeed guide rail72pass
- Capper chuck 3118pass
Bar chart of the example swabs on the line 2 filler and capper against a site limit of 150 RLU: fill valve 12 nozzle 412 (fail, retest 38), fill valve 27 nozzle 64, infeed star wheel 55, infeed guide rail 72, capper chuck 3 118. 4 of 5 passed the first time, 80.0 percent.
- The SSOP: lock out the main disconnect and the air supply (2 points), dry clean the deck, pre-rinse, take the star wheels, guides and capper chucks to the soak tank, foam with a chlorinated alkaline cleaner, scrub, rinse, inspect, put back, then sanitize with a no-rinse peracetic acid sanitizer (test strip reading 150 ppm). Time allowed: 150 minutes.
- Pre-op at 05:00 by the QA technician: 23 checks, 20 pass, 2 N/A (no allergen ran) and 1 fail. Every surface passed the visual check.
- The fail was an ATP swab: the nozzle tip of fill valve 12 read 412 RLU against the site's limit of 150, an example limit the plant set from its own data. The other four swabs read 64, 55, 72 and 118.
- Correction: the nozzle was taken off, soaked, brushed, rinsed and sanitized, and swabbed again at 05:40: 38 RLU. The line was released at 05:45, 15 minutes after the planned 05:30 start. No product had run, so none was held.
- Cause and change: the SSOP said to wipe the nozzles in place, and sugar film builds up inside the tip. Revision 3 takes all 40 nozzle tips off every night and allows 165 minutes instead of 150, signed and dated by the plant manager.
4 of 5 swabs passed the first time (80.0%), 20 of the 21 graded pre-op checks passed (95.2%), and 35 minutes went by between the failed swab and the release. The lesson is the visual pass with an ATP fail: a surface can look clean and not be, so put the swab sites where film hides.
Common mistakes
One SSOP for the whole plant
"Clean and sanitize all equipment daily" cannot be followed at a filler at 2 am. Write one sheet per machine or area, with its own parts, points and times.
Strengths and times from memory
Detergent strength, water temperature, contact time and sanitizer concentration come from the product label, and PPE from the safety data sheet. Write them on the SSOP, and check the sanitizer with a test strip every time.
The cleaner checks their own work
A pre-op by the person who just cleaned finds little. Someone else looks, with a torch, at the points the SSOP lists.
Treating a visual pass as clean
Film inside a nozzle or under a gasket is invisible. Swab the points where residue hides, on a plan, and act on the reading against your own limit.
Rechecking instead of changing the method
If the same point fails twice, another reclean is not a corrective action. Change the step, the tool or the time allowed, sign the new revision and retrain the crew.
Download the template
Free to use: print it, copy it and edit it for your team. Enter your name and work email once to download.
Run this template in LeanSuite
In Lean Creator you set up your own GMP inspections, HACCP verification checks and pre-operational sanitation checks, schedule them to the right people and complete them on a phone or tablet with photos.
See it in a 45-minute demoIn the lean glossary
Free tools
Guides
- Master sanitation schedule: when each cleaning task is due
- Food plant GMP inspection checklist (21 CFR 117 subpart B)
- SQF internal audit checklist, mapped to BRCGS and FSSC 22000
- HACCP plan template: hazard analysis and CCP worksheet
- Sanitation and cleaning verification, ready in the LeanSuite app
- Pre-operational inspection, ready in the LeanSuite app
- Cleaning verification swab audit, ready in the LeanSuite app
- Allergen changeover verification, ready in the LeanSuite app
- What an SOP is and the format that works on the floor
- Lockout tagout: the steps and who applies the locks
- LeanSuite for food and beverage plants
FAQ
SSOP template: sanitation standard operating procedure: common questions
A sanitation standard operating procedure: the written method for cleaning and sanitizing one area or machine, with the steps, chemicals, strengths, contact times, who does it, how often and how it is checked. It is how a plant shows that cleaning is done the same way every time, and the record that it was done and verified.
The eight conditions FDA's juice and seafood HACCP rules (21 CFR 120.6 and 123.11) ask processors to monitor: safe water and ice; clean food-contact surfaces, including gloves and outer garments; no cross-contamination from dirty objects or raw product; working hand-wash, hand-sanitizing and toilet facilities; food and packaging protected from lubricants, chemicals, condensate and other contaminants; toxic compounds labelled, stored and used properly; sick employees kept from contaminating food; and pests kept out.
The master sanitation schedule lists every cleaning task in the plant with its frequency, owner and next due date: it says when. The SSOP is the method for one task or machine: it says how. Each line of the schedule points to an SSOP number, and the pre-op check and swabs show the SSOP worked.
In the US, meat and poultry plants under USDA FSIS inspection (9 CFR 416) and FDA-regulated juice processors (21 CFR 120.6). FDA recommends them for seafood processors (21 CFR 123.11). Other FDA plants must keep the plant and food-contact surfaces clean (21 CFR 117.35), and where the food safety plan needs sanitation controls they must be written, with written monitoring. Customers and certification schemes such as SQF and BRCGS expect written cleaning procedures too.
ATP testing swabs a cleaned surface for adenosine triphosphate, found in food residue and cells, and reads it on a meter in relative light units (RLU) within seconds. There is no universal pass mark: meters differ, and the limit is a site value set from your own readings and the meter maker's guidance. ATP shows residue, not pathogens, so plants still run microbiological swabs on a plan.
More free templates
All templates- Leader standard work templateA team leader's daily, weekly and monthly routine with a box per day, follow-ups and a weekly review.
- Supervisor leader standard work templateA supervisor's daily, weekly and monthly routine with a box per day, an escalation log and a weekly review.
- Production manager leader standard work templateA production or value stream manager's routine by day, week and month, with an escalation log and a weekly review.
- Plant manager leader standard work templateA plant manager's short routine by day, week and month, with an escalation log and a weekly review.
- 8D report templateD0 to D8 with targets, containment counts, occurrence, escape and systemic causes, verified actions and a worked example.
- Poka-yoke worksheetEach step's errors and what they cost, the device (approach, function, method), payback, and a log that proves each device works.
- Standard work sheet templateTakt time, each element's manual, machine and walk time on a time chart, key points and standard WIP.
- One point lesson (OPL) templateOne topic on one page: wrong way and right way pictures, checkable key points, the standard it belongs to and a sign-off record.
- Layered process audit (LPA) checklist20 yes, no or N/A checks at the station, a layer and frequency matrix, question banks for four processes and a findings table.
- IATF 16949 internal audit checklist40 audit questions in three parts, one for each internal audit IATF 16949 names (system, manufacturing process, product), each with its clause, the evidence to look for, a core tool tag and a column for the customer's own requirement.
- Process audit checklistAudit one process from inputs to results: 32 questions graded conforms, minor or major, a product check, a score by group and a findings list.
- PFMEA template (process FMEA)Failure modes, effects and causes rated for severity, occurrence and detection, with RPN before and after action.
- Pareto chart templateA tally sheet, the Pareto by count and by cost with the cumulative line and the 80% cut, and a before and after comparison. Excel sorts and draws it.
- Control plan templateWhat is checked at each step, against which limits, how, how often, and what to do when a result is out.
- Corrective action request (CAPA) formOne problem from containment to proof the fix worked, with occurrence and escape causes and a closure check that tells you when it can close.
- Time study sheetTime each element over 10 cycles and work out the average, lowest repeatable and standard time. Excel does the sums.
- ISO 9001 management review kitA 90-minute agenda, data sheet, minutes and action log for the clause 9.3 review, with an Excel planner that flags the next review due.
- Non-conformance report (NCR) formA two-page NCR from the requirement against what was found to disposition and closure, and an Excel NCR log.
- CAPA log templateAn Excel CAPA tracker with status, days open, late flags and counts by source, plus a printable log and monthly review.
- Supplier corrective action request (SCAR) formA SCAR from the problem and containment asked for to the supplier's 8D-style response, verification and closure, with a filled-in example.
- First article inspection report template (AS9102 forms)The three forms in the AS9102 layout (part number, product and characteristic accountability), 22 review checks, the full and partial FAI triggers, and a worked example with one failed characteristic.
- FOD walk checklist (foreign object debris)26 checks for a FOD walk on the production floor in six groups, a FOD found log, an area plan with the route and frequency, and a worked six-week trend of finds per walk.
- Welder continuity log templateA continuity log for welder qualifications with the next lapse date worked out for each process, 20 checks on the records and the log, and a worked example with three welders and one lapse.
- Weld inspection checklist (visual welding inspection)30 checks before, during and after welding, a guide to the discontinuities visual inspection looks for, a weld map report and a worked example on a 12-weld frame.
- AS9100 internal audit checklist42 audit questions on AS9100D clauses 4 to 10 with the aerospace additions, the evidence to look for and a sample for each area, five grades, a finding and corrective action report, and a worked audit carried through to closure.
- Manufacturing process instruction (MPI) templateOperation steps with parameters, tools, quality checks, safety and a photo each, plus revision history and approval.
- Engineering process instruction (EPI) templateScope, parameters and limits, equipment and materials, validation steps, acceptance criteria, change history and approvals.
- Design FMEA (DFMEA) templateA design FMEA worksheet with S, O, D and RPN before and after action, a class column and a design rating guide.
- PPAP checklistThe 18 PPAP elements with owner, due date and status, the five submission levels and a readiness count.
- Process capability (Cpk) study sheet25 subgroups of readings with Cp, Cpk, Pp and Ppk worked out, control limits to check stability, and a histogram.
- Incoming inspection checklistReceiving inspection checks from paperwork to sample, the sampling plan, the decision, and an Excel log by supplier.
- Supplier audit checklistA supplier process audit of 32 questions scored 0 to 3, with section scores, a rating and the findings.
- Supplier scorecardMonthly PPM, on-time delivery and SCAR measures turned into points, a weighted score and a rating per supplier.
- Pre-shipment inspection checklistThe last check before shipping: part, quantity, labels, packaging, paperwork and photos, then release.
- Changeover checklist25 checks for every changeover, a record of planned and actual times, and a log of changeover time against target.
- Standard work audit checklist24 checks of a job against its written standard, ten timed cycles, and each gap sorted by cause before anyone acts.
- Defect check sheetTally defects by type and day, with units inspected, defect rates, a location sheet and the week's Pareto.
- TWI job breakdown sheetThe TWI Job Instruction breakdown of a job into important steps, key points and reasons, with a worked example and the four steps.
- Standard work combination tableOne operator's manual, machine, walk and wait time on a time chart against takt, with machine cycles and a process capacity sheet.
- QA matrix templateDefect modes against stations in flow order: where each is made and first caught, a weight × occurrence × detection score, an AA to C class and the escapes flagged.
- Is / is not analysis templateWhat, where, when and extent with is, is not, distinctions and changes, then each possible cause tested against every pair and ranked.
- Yokoten tracker (horizontal deployment)Copy a proven improvement line by line: the source result, each candidate's own before and after, its share of the source's improvement and the standard updated.
- 4M change management sheet (change point)A shift log of every change to Man, Machine, Material, Method or Design, the extra checks after it and when normal checks resume, with a change point board.
- Histogram templateReadings, bins set by the square root rule, a tally and counts, the spec limits drawn and the share out of spec, with the common shapes explained.
- Scatter diagram templateUp to 50 pairs with a group code, r and R², the least squares line, the quadrant count and r for each group.
- Gauge calibration logA gauge register with next due dates and status, a calibration record with as-found and as-left readings, and the steps when a gauge fails.
- Quality alert formA quality alert to post at the line, a sign-off sheet for every shift, and a log of open, expired and closed alerts.
- TQM self-assessment templateThe eight TQM principles in 24 statements you can check on the floor, scored 0 to 4 by several people, with the spread, the top 3 gaps and an action plan.
- Quality circle meeting recordA circle's charter, a one-page record for each meeting and a problem register that follows every problem from selected to closed or escalated.
- Process capacity sheet templateEach machine in a part's routing with manual, auto and tool change time, its capacity per shift, and the step that limits the cell against demand.
- Jidoka worksheet (stop at abnormality)For one line or cell, every abnormality that should stop the work: how it is detected, how the work stops, who is called, the immediate fix and the root cause step, plus a log of real stops.
- Chaku-chaku line plannerPlan a load-load cell: time each machine, load and walk, check that every machine is ready when the operator comes back, compare the cell cycle with takt and size the crew.
- Standard operating procedure (SOP) templateA full SOP in the hierarchical step format, from purpose and scope to the steps, records, revision history and approvals, with review checks and an SOP register.
- X-bar and R control chart template25 subgroups with means and ranges, control limits from A2, D3 and D4, signal flags, both charts and a reaction log.
- Gage R&R study sheet10 parts, 2 or 3 appraisers, 2 or 3 trials: EV, AV, GRR, PV, %GRR and ndc by the average and range method.
- Root cause analysis templateOne report from problem statement to proof: containment, evidence, analysis, verified causes, actions and the effectiveness check.
- Quality control pillar 90-day model area planThirteen weeks from the QA matrix to the QM matrix on one model area, a KPI board, the day-90 gate and expansion waves.
- Error-proofing verification log (daily master-sample check)Each poka-yoke device proved every day or week with a known-bad sample, with missed checks counted and the hours and parts at risk worked out when one fails.
- Defect catalogue template with boundary samplesEvery defect with a definition, a class and the reason for it, measured accept and reject limits by zone, boundary samples, a defect log with DPU and Pareto, and an inspector agreement check.
- I-MR chart template (individuals and moving range)Up to 100 single readings with moving ranges, limits from a baseline, five run-rule flags, both charts, a second phase and a reaction log.
- Attribute control chart template (p, np, c and u charts)p, np, c and u charts in one workbook: a chart selector, a sample size check, limits for each subgroup, signal flags and four worked examples.
- HACCP plan template: hazard analysis and CCP worksheetThe Codex 12 steps in one workbook: team and product, process steps checked on site, hazard analysis with the CCP decision tree, the CCP table with completeness checks, an allergen matrix and a verification schedule.
- Mock recall template: traceability exercise worksheetTrace a finished lot back to every input lot and forward to every first customer, reconcile the quantities against a tolerance and time it against your target.
- ISO 9001 internal audit checklist (production area)46 audit questions for the production floor in 11 processes, each with its ISO 9001:2015 clause, what evidence to look for and the sample to take, plus five defined grades, a findings log, a finding report and a summary by clause.
- Food plant GMP inspection checklist (21 CFR 117 subpart B)55 checks in the order of 21 CFR 117 subpart B, each citing its paragraph and saying what to look at, with a grade, finding, owner and due date; results by section and grade, a walk route and a bakery example.
- Master sanitation schedule with pre-op verificationA master list of cleaning tasks by area and equipment with frequency, chemical, lockout, who and next due date, a weekly on-time count, and the pre-operational verification log with a release step.
- Measurement uncertainty budget templateA GUM uncertainty budget: Type A and B rows, divisors by distribution, sensitivity coefficients, uc, νeff, k from the t-table, U, TUR and a guard band check.
- Video time study filming checklistA pre-shoot checklist and shot log for filming a time study on video: camera, light, people, settings, power and review.
- Defect detection matrix templateMap where each defect is created and where it is found, score the gap and move the check closer to the cause.
- Hazard prediction worksheetA pre-task worksheet: score what could go wrong at each step of a job, add a countermeasure and score again.
- APQP checklistThe five APQP phases as a checklist: deliverables, owners, due dates, gate reviews and an issues list.
- Out-of-control action plan (OCAP) templateA reaction plan for a control chart: the steps, what each signal means, who to call and a log of events.
- Quality inspection checklistAn in-process and final inspection record: measured characteristics, visual checks, a decision and first pass yield.
- AQL sampling plan templatePick a sample size, read accept and reject numbers, record the defects and decide on the lot.
- MSA study workbookBias, linearity and stability study sheets for a gauge, with the arithmetic done and a guide to which study when.
- Incoming quality control stage sheetA register that shows how much control each purchased part has and plans the move from your dock to the supplier's process.
- Internal audit schedule templateA year of internal audits planned by risk: the programme, the register, the auditors and the findings.
- Approved supplier list templateThe list of suppliers you may buy from, with the evidence behind each, certificate expiry alerts and re-evaluation dates.
- Pest control inspection checklistA pest control walk-round for a food plant, with a log of traps and stations and action levels for each type of device.
- Cleanroom audit checklist33 cleanroom checks split by how often they run (each shift, weekly, per plan, system), a gowning order to watch against, a differential pressure log and a findings log, with a worked week of readings.
- GMP audit checklist for drug manufacturing42 self-inspection checks ordered by the subparts of 21 CFR 211, each with its section, the matching EU GMP chapter and whether it is seen on the floor or in records, graded critical, major or minor, with a worked audit of a packaging line.
- Line clearance checklist28 line clearance checks in six sections (area, equipment, materials, printed materials, documents, coder and vision settings), cleared by the operator and verified by a second person, with a printed-materials reconciliation and a worked example that does not balance.
- ISO 13485 internal audit checklist38 questions on ISO 13485 clauses 4 to 8, each with the FDA QMSR section that brings it in or adds to it, a production floor tab (records, current instructions, training, nonconforming product, CAPA) and a worked audit of a catheter line.
- ISO 22716 GMP audit checklist for cosmetics25 cosmetic GMP checks following the sections of ISO 22716, split into a floor walk (people, premises, equipment, materials, production) and system checks (lab, out of specification, deviations, complaints, change control, audits, documents), with a worked audit of a filling line.
- SQF internal audit checklist for food manufacturing54 questions in the two parts of the SQF manufacturing code (system elements and GMP), each group mapped to BRCGS and FSSC 22000, graded Conforms to Critical, with findings, a score and a yearly plan.
- Injection molding defects chart16 molding defects with causes by machine, material, mold and method, first checks, and an Excel defect log with a Pareto.
- ESD audit checklist29 checks for an ESD protected area, with daily tests split from periodic verification, a measurement log and a worked audit.
- 5S audit checklist template25 checks, five per S, scored 1 to 5, with a score summary and a chart of the five S's.
- 1-1-90 method worksheetOne page: score areas 1 to 5, write the pain point with a before and target number, check days 30, 60 and 90, and plan the next three areas.
- Gemba walk checklistA walk plan and route, 30 prompts in six groups and a findings table with owners and due dates.
- Gemba walk field guideA 20-page pocket guide: the rules, 48 questions by area with good and warning answers, a 30-day route and the follow-through loop, plus an action-log workbook.
- Autonomous maintenance (CILR) checklist20 clean, inspect, lubricate and retighten checks with a box per day, an abnormality log and sign-off.
- A3 problem solving templateThe standard seven-box A3 from background to follow-up, with a filled-in worked example. PDF and Excel.
- PDCA templateOne improvement cycle on one page: plan, do, check against the goal, then standardize or adjust. PDF and Excel.
- 5 Whys templateA problem statement, a why chain that can branch, evidence for every answer, root causes and countermeasures that are checked.
- 5W1H templateWho, what, when, where, why and how: a problem statement built from checked facts, and an action plan with nothing left open.
- Skills matrix templatePeople by tasks on a 0 to 4 scale, coverage and gaps per task and shift, and a training plan that closes them.
- SMED changeover worksheetChangeover steps with times, internal or external, what can move, ideas and before/after totals.
- Kaizen event charter templateProblem, goal, scope in and out, boundaries, metrics from baseline to target, team and roles, and sign-off before day one.
- RACI matrix template17 kaizen project tasks by 10 roles, with R, A, C, I drop-downs and a check for one accountable per task.
- 5S red tag log and red tagsA log of every red-tagged item with its decision, and six printable red tags to cut out.
- Shift handover templateSafety, production against plan, holds, downtime events, materials and people, and the open actions the next shift takes over.
- Shift schedule packTen shift patterns defined exactly, each with a 28-day calendar, hours worked out from the cycle and a US 40-hour check, plus an Excel roster.
- Kanban card templateSix production and six withdrawal kanban cards to print and cut out, with loop sizing and a card register.
- Idea suggestion formA one-page idea form with the supervisor's answer and points, and an idea log that tracks days to answer.
- Just Do It (JDI) card templateSix Just Do It cards per sheet for quick fixes, with the rules for what counts and a log of every card.
- Quick kaizen templateOne page for a small improvement: before and after, the cause, the countermeasure, the results and whether the standard changed.
- Spaghetti diagram templateSquared paper to trace every trip, a trip log that turns grid squares into feet, meters and walking time, and a before and after comparison.
- OEE tracking sheetOne row per shift for a week. The Excel version works out availability, performance, quality and OEE and charts the week.
- OSHA 300 log workbookA log laid out like OSHA Form 300, a 300A that totals itself, TRIR and DART rates, and an is-it-recordable walk traced to 29 CFR 1904.
- Near miss report formA two-page near miss report from the first report to closure, and an Excel log with status and days open.
- Safety observation card templateFour behavior-based safety cards per sheet, with safe and at-risk checks, the conversation and a tally sheet.
- Job safety analysis (JSA) templateJob steps, hazards, risk scored before and after the controls, the hierarchy of controls, PPE and sign-off.
- Risk assessment matrix template (5×5)A color-coded 5 × 5 severity and likelihood matrix, a scoring guide and a risk register.
- Incident investigation report templateFacts and a sourced timeline, causes at three levels, actions by the hierarchy of controls, a US recordkeeping screen and a closure check.
- Incident report templateThe first report, filled in the same shift: what happened, people, injury or damage, treatment, a US recordkeeping screen, actions and an Excel incident log.
- Toolbox talk templateA record of a short safety talk: topic, key points, questions raised, actions and an attendee sign-in sheet.
- Lockout/tagout (LOTO) procedure templateA machine-specific LOTO procedure: energy sources and isolation points, the steps from shutdown to restart, and the annual review.
- Forklift inspection checklist23 pre-shift checks for a week on one page, a do-not-operate rule, and a defect and repair log.
- Preventive maintenance checklist templateA PM checklist per machine with readings and sign-off, and a PM schedule that works out the next due date.
- Equipment downtime log (MTTR and MTBF)A breakdown and downtime log, with MTTR, MTBF and downtime by machine and cause worked out in Excel.
- Environmental aspects and impacts registerAn ISO 14001-style register of aspects and impacts, with significance scoring, legal requirements, controls and owners.
- Training sign-off sheetAn attendance and sign-off record where each person signs they understood, with a competence check and an Excel log.
- Learning curve and ramp-up workbookBoth learning curve models side by side, a fit from your own observed hours, batch hours, the unit that reaches standard and a weekly ramp plan.
- Operator staffing calculatorTakt, work content, the operators a line needs, a check of your station plan and the roster with absence cover, from your own demand and element times.
- On-the-job training (OJT) checklistThe training record for one trainee on one job: the four TWI steps signed, every try judged, qualified when your rule is met, then tapering follow-up checks.
- New hire onboarding checklist (manufacturing)29 onboarding items from before day 1 to the 90-day review, with owners, dates and review notes.
- Competency assessment formThe one-person assessment behind a skills matrix rating: each task rated 0 to 4 from evidence, checked, with a training plan for every gap.
- Cross-training plan templateWho is learning which task, from and to which level, by when, and how many are qualified on each task.
- Absenteeism tracker templateA monthly attendance grid with codes, absence rate by person and team, and an optional Bradford factor.
- Engineering change request (ECR) formAn ECR form with the change, what it touches, risk and approvals, and an Excel log that tracks each change to done.
- Process flow diagram templateA squared sheet to draw the flow with a symbol key, and a step table that counts operations, moves, checks, waits and storage.
- Office 5S audit checklist25 checks written for offices and shared areas, five per S, scored 1 to 5, with a score summary and actions.
- Floor marking color guideA floor marking color standard with swatches, marks and line widths to fill in, and a floor marking check with a layout sketch.
- Shadow board plannerTool inventory with fetch time, a layout planned from each tool's outline size, a month of daily checks with 5S audit evidence, and a missing tool log.
- Lubrication schedule templateEvery lube point with lubricant, method, amount, frequency and who, with next due dates and a monthly sign-off record.
- TPM tag logEvery abnormality tag with type, who fixes it, priority and dates, with days open and counts by type and week.
- Autonomous maintenance step auditCriteria for each of the seven autonomous maintenance steps, scored 0 to 2, with the step result and the decision to move on.
- Inventory cycle count sheetA blind count sheet with variance and tolerance, an ABC count schedule and record accuracy, worked out in Excel.
- Hour-by-hour production boardHourly plan against actual with running totals and the reason for each miss, plus a shift summary by reason.
- Cost savings trackerA savings log with hard and soft savings, payback and Finance's sign-off, plus a glide path against the year's target.
- CapEx request formA capital request with options, costs, benefits, payback and NPV, and the approval levels the amount needs.
- Standard cost variance workbookEight standard cost variances from your standards and actuals, favorable or unfavorable, proved against actual cost, with the questions to ask on the floor.
- Cost-benefit analysis templateUp to three options side by side with costs, hard and soft benefits, payback, NPV and the benefit-cost ratio.
- Cost of poor quality (COPQ) worksheetCost of quality by prevention, appraisal, internal and external failure, with COPQ as a share of sales.
- Receiving logA dock receiving log with quantities, damage, QC holds and putaway, plus a discrepancy report and dock-to-stock time.
- Warehouse safety inspection checklistThirty warehouse safety checks from aisles to fire exits, marked OK or Not OK, with an action for every finding.
- Pallet racking inspection checklistRack checks per aisle with a green, amber and red damage rating, and a damage log with repair dates.
- Material shortage logEvery part short with its need date, line impact, ETA and escalation, and counts by reason and supplier.
- Safety audit checklistThirty-four plant-wide safety checks answered Yes, No or N/A, scored by area, with a risk rating and an action for every No.
- Ergonomic risk assessment checklistScreen a task for 21 ergonomic risk factors, score how long each lasts, and rank tasks so the worst get controls first.
- Work order template for maintenanceA work order template for maintenance: one form per job from request to handback, and a log of response, completion and backlog by priority.
- Six big losses worksheetWhere a machine's planned time goes: the six big losses in minutes, ranked, with A, P, Q and OEE worked out.
- Andon response logEvery andon call with response and fix times, flags against your targets, and counts by type and station.
- Kanban sizing calculatorHow many kanban cards each loop needs, per part, with the change from today's cards and what the loop holds in days.
- Kaizen event trackerEvery kaizen event on one sheet: status, roles, the metric against target, open actions and the 30, 60 and 90 day checks.
- Lead time worksheetProduction lead time from the inventory waiting at each step, value-added time and process cycle efficiency, plus an order traced from order to delivery.
- Waste walk checklist (TIMWOODS)32 things to look for across the eight wastes, with where and how much, and a findings log with dot votes, owners and dates.
- Maintenance KPI trackerMTBF, MTTR, availability and PM compliance per asset and month, plant figures from the totals, planned maintenance % and backlog in weeks.
- Daily huddle agendaA 15-minute start-of-shift stand-up in six timed blocks, with yesterday's SQCDP results, today's plan, actions and escalations.
- DMAIC project charter templateThe Define-phase charter on one page: problem and goal, metrics, scope, team and phase dates, with savings and a tollgate checklist.
- Water spider route plan (mizusumashi)A water spider's fixed route: stops with arrival times, what is delivered and collected, route time against the cycle, cart load and a trip log.
- Cost deployment matrixWCM cost deployment on paper and in Excel: loss quantities by process, causal and resultant losses, the cost of each loss, a Pareto and the projects that recover them.
- Equipment criticality analysisAssets scored 1 to 5 on six criteria with your own weights, ranked and sorted into classes A, B and C with a safety override and a suggested maintenance strategy.
- Bottleneck analysis worksheetEffective capacity per station from cycle time, parallel units, availability and yield, the bottleneck, takt and utilization, a queue cross-check and the five focusing steps.
- Fault tree analysis templateA drawing area with the FTA symbols, an event table with probabilities and minimal cut sets, and the gates worked out bottom-up in Excel.
- 5G investigation sheetConfirm the facts before naming a cause: 5W1H, the five G's with 20 prompts, the gap against the principle and the standard, and the countermeasures.
- Coaching kata template (improvement kata storyboard)The learner's storyboard (target condition, current condition, obstacles, PDCA cycles) and a fold-over card with the coach's five questions.
- SMART goals templateWrite a goal, test it against the five SMART letters, then track progress toward the target against the time used.
- Lean readiness assessment templateTwenty statements in four factors, scored 1 to 5 by several people on their own, with averages, the spread between them and the actions.
- Nemawashi template (stakeholder plan)Plan the one-to-one conversations before a decision: who to talk to in what order, their concerns, what changed and where they stand.
- Breakdown analysis reportOne equipment breakdown from the stop to the 90-day check, plus a breakdown log with repeat flags, MTBF and MTTR by asset and a Pareto of causes.
- Heijunka box planner (production leveling)Weekly demand turned into containers a day, takt, pitch and slots, a leveled sequence of products and the heijunka box, with a check that the changeovers fit.
- Future state value stream map worksheetThe eight future-state questions worked through in order: takt, pitch, flow, supermarkets, the pacemaker and the mix, with an EPEI check and current against future lead time.
- Value stream plan (VSM action plan)The future-state map cut into loops, each with an objective and a measurable goal, and its kaizen bursts turned into owned, dated projects on a 12-month timeline.
- Kaizen project plan (Gantt chart)One improvement project as a Gantt chart: tasks by phase with owners, predecessors and working days, a 16-week grid, milestones and a status from planned against actual % done.
- Escalation matrix templateWho is called for each type of issue and after how long, with severity rules, contacts and an escalation log.
- Visual management audit checklist29 checks of whether anyone can tell normal from abnormal at a glance, scored by group, with a trend and actions.
- Employee recognition program templateDesign a recognition program on one page, then run it: points per action, prizes, budget, a points ledger, a monthly leaderboard and a fairness check by team and shift.
- Lean transformation roadmapA plant-wide lean program on one sheet: six phases with exit criteria, six workstreams by quarter over 24 months, the model line, metrics with baseline and target, cadence and risks.
- Obeya room plannerPlan the walls, owners, cadence, agenda and rules of an obeya, then run the weekly review of KPIs, problems, actions and milestones.
- Paper forms inventory (paperless manufacturing worksheet)Every paper form, checklist and log in one list: hours a month, who acts on it, how long the paper waits, and which forms to move first.
- Continuous improvement software evaluation scorecardCompare CI software vendors: a must-have gate, eight weighted criteria scored 1 to 5, points out of 100 and a rank, with a demo script and reference questions.
- Lean principles assessment templateThe five lean principles as 25 things you can see on one value stream, answered yes, partly or no on a walk, with a score per principle, the next step and a trend over walks.
- Employee engagement survey templateA short anonymous pulse survey for shop floor staff: 14 statements in six drivers, two open questions, results by driver and team, and the actions.
- Hansei reflection sheet (lessons learned)A written look back at one finished project, event or launch: goals against results in numbers, causes rather than blame, lessons to keep or change, and where else they apply.
- Safety cross calendarA month drawn as the green cross, colored each day by the most serious safety event, with totals and days since the last injury.
- Daily kaizen routine boardA team's 10 to 15 minute daily routine at the board: one problem from each person, small fixes with one owner, counted every week.
- Weekly maintenance schedule templateNext week's maintenance jobs, scheduled only when ready, loaded against each craft's hours by day, with schedule compliance and break-ins at week end.
- Operational excellence assessment templateThe ten principles of operational excellence as 30 behaviors and practices you can see, scored 1 to 5 by several people, with the spread, the three lowest principles and an action plan.
- Scrum meeting agenda templateTimed agendas for the five scrum meetings, a sprint planning sheet, a retrospective sheet, and an Excel sprint backlog with a burndown.
- Toyota Production System (TPS) house templateThe TPS house for one plant or value stream: roof, two pillars and foundation, with what you do today, the evidence, a status and the next step for each element.
- EPEI and batch size calculatorHow often each part can come round on a shared machine (EPEI) and how big each batch must be, from demand, cycle times and changeovers, now and after SMED.
- People, process, technology (PPT) assessmentCheck one change before go-live: 18 people, process and technology statements scored 1 to 4 by the people who will use it, the lowest element and the actions.
- Team charter templateA one-page charter for a standing team: purpose, scope, roles, the KPIs it owns, which decisions it makes itself, norms and cadence.
- Process improvement method selectorEight questions about one problem, an example rule that suggests a method and a matrix of nine methods: when each fits, the usual team and time, and the template to start with.
- Safety pillar 90-day model area planThirteen weeks from the incident pyramid to safety standards on one model area, a KPI board, the day-90 gate and expansion waves.
- Autonomous maintenance 90-day model area planAM steps 0 to 3 on one model machine in 13 weeks, a KPI board, the day-90 gate and expansion waves for months 4 to 12.
- Professional maintenance (PM) 90-day model area planThirteen weeks from breakdown analysis to a running PM calendar on one model machine, a KPI board, the day-90 gate and expansion waves.
- Environment and energy pillar 90-day model area planThirteen weeks from waste and energy maps to area standards on one model area, a KPI board, the day-90 gate and expansion waves.
- Focused improvement 90-day model area planThirteen weeks from the loss Pareto to standardized fixes on one model line, a KPI board, the day-90 gate and expansion waves.
- Logistics and customer service pillar 90-day model area planThirteen weeks from the current-state map to pull on one model value stream, a KPI board, the day-90 gate and expansion waves.
- People development pillar 90-day model area planThirteen weeks from the skills matrix to trained cover on critical tasks in one model area, a KPI board, the day-90 gate and expansion waves.
- Early equipment management 90-day model area planThirteen weeks from lessons on current machines to a tracked start-up on one model equipment project, a KPI board, the day-90 gate and expansion waves.
- Cost deployment pillar 90-day model area planThirteen weeks from the loss map to costed, ranked projects in one model area, a KPI board, the day-90 gate and expansion waves.
- Moving from Excel to one system checklistA 34-point checklist and a file inventory for moving trackers from spreadsheets to one system: keep, move, connect or retire, clean, pilot, run both, retire.
- Prioritization matrix templateScore up to 20 improvement ideas on weighted criteria, rank them, test the ranking with equal weights and place each one on an effort and benefit grid.
- Cost per unit worksheet (manufacturing cost per good unit)One product's cost per good unit by materials, labor, machine and overhead, the gap to target, and which cost lever is worth most a year.
- Digital manufacturing readiness assessmentScore 24 statements on process, technology and people from 0 to 4, check the balance between them and rank the gaps by what matters in your plant.
- Manufacturing KPI dashboard templateWeekly plant numbers in, 14 KPIs out: OEE and its parts, first pass yield, scrap, on-time delivery, recordable rate, cost and absence, each against a target.
- RCM worksheet (failure mode and task selection)Failure modes classed as hidden, safety, operational or non-operational, then a task chosen for each: condition-based, discard, failure-finding, redesign or run to failure.
- Training matrix template with expiry datesPeople by required trainings with expiry dates, OK, due, expired and missing flags, compliance by person and area, cover per training and a renewal list.
- Downtime reason codes template26 starter codes mapped to the six big losses, a log with drop-downs, a Pareto by code and by loss, and a code card for the line.
- Kaizen event preparation checklistEverything that has to be ready before a kaizen event and done after it: 44 items with owners and due dates from 6 weeks before day 1 to 30 days after, five go or no-go gates and a day-by-day agenda.
- Critical spare parts list and stocking levelsAssets ranked by consequence, each part classed and given a stocking policy, and min and max worked out from usage and lead time, with the downtime each stock-out would cost.
- Tier 2 meeting agenda and escalation sheetA 15-minute tier 2 agenda in ten timed blocks, fixed roles and rules, escalation triggers with time limits, and a log that ages every escalation and sends the answer back down.
- Forklift operator training and evaluation recordPer-operator training and evaluation record, a register with three-year due dates and refresher triggers, and a weighted practical evaluation scoresheet.
- REBA worksheet (Rapid Entire Body Assessment)Score up to six postures with REBA: body-part drop-downs, Tables A, B and C as lookups, final score and action level, and a before and after comparison.
- ISO 45001 internal audit checklist44 audit questions for the plant floor in 16 safety topics, each with its ISO 45001:2018 clause, the evidence to look for and the sample to take, plus 12 worker interview prompts, a findings log and a summary by clause.
- Plan for every part (PFEP) templateOne row per part: supplier, pack, container, usage, lead time and locations, with ABC classes, market and line kanban counts and a lineside space check.
- Changeover matrix templateA from-to matrix of changeover minutes with the clean each transition needs (allergen, colour, format), and a weekly planner that totals the order and suggests a shorter one.
- Overhead crane inspection checklist: frequent and periodic34 crane checks tied to OSHA 1910.179: an operator's pre-shift card, frequent and periodic inspections with signed records, a deficiency and tag-out log, and a register of next due dates.
- Maintenance job plan templateOne job planned on one sheet: steps and craft hours, parts checked against stock, tools, lockout and permits, documents, a ready check for the schedule, and technician feedback.
- Reorder point and safety stock sheet (many parts)Safety stock, reorder point, order quantity and an order list for up to 500 parts, worked out from each part's own demand and lead time history.
- OSHA compliance calendar (general industry)37 recurring federal OSHA duties with the paragraph, interval, owner, next due date and an overdue flag, plus a 12-month view and counts by owner.
- TRIR and DART rate trackerMonthly hours, OSHA 300 case counts and near misses in; rolling 12-month TRIR and DART rate, a case budget against your target and a trend chart out.
- Energy use and EnPI trackerMonthly electricity, gas and fuel in one unit, a 12-month regression baseline, expected against actual energy for each month, an EnPI ratio, the running saving and the tests that say whether the model can be trusted.
- FIFO lane sizing sheetThe maximum for a FIFO lane from the stop it must cover, in whole containers, with length, refill and wait checks for up to eight lanes.
- Pugh matrix templateCompare up to 8 concepts with a datum as better, same or worse on up to 12 criteria, flag must-haves, and carry the strongest into a second round.
- Machine guarding inspection sheetA machine register with due dates and a status per machine, 21 checks tied to OSHA 1910.212, .219 and .147, a guard opening check against Table O-10, and an action log.
- Condition monitoring route sheetA route of measuring points with baselines, alert and alarm limits, a check interval from the P-F interval, readings with rising and overdue flags, and an exceptions list worst first.
- Fire extinguisher inspection checklist and logThe 8 monthly checks for each portable extinguisher, plus a log with the hydro test interval from OSHA Table L-1, annual and 6-year due dates and open issues.
- Quad chart templateA project on one page in four boxes: idea and owner, problem, approach, and cost, schedule and result.
- Toolbox talk topics (52 weekly topics)52 weekly toolbox talk topics, each with a one-line key message and a discussion question, and a tracker for the year.
- Loss tree worksheetBreak one big loss number into area, line, machine, loss type and cause, and stop at the cause a team can fix.
- Equipment register templateOne row per asset, with hierarchy, criticality, PM strategy and owner, and a check that flags what is missing.
- Machine history record templateOne record per machine: components and their life, every breakdown and repair with cost, MTBF and MTTR, and a repair-or-extend check.
- Compressed air leak survey logWalk sheet, printable leak tags and a tracker that puts an annual cost on every leak and follows it to a verified fix.
- Project savings validation checklistThe gate between a project's claim and a reported saving: 20 checks, a claims register and a six-month sustainment check.
- Life cycle cost analysis templateCompare up to three machines over ten years: price, energy, upkeep, failures and down time, discounted to present value.
- Equipment design review checklistGate reviews for a new machine before order, before build and before start-up, with a safety buy-off and a problems journal.
- Emergency action plan templateA written emergency plan for a plant: site facts, roles and backups, warden coverage, scenario steps and a drill record.
- Preliminary hazard analysis (PHA) worksheetFind and score the hazards of a new line, machine or process before design is fixed, then choose controls and re-score.
- Risk register templateOne scored list of operational risks with owners, actions and dates, a heat map and a review log.
- Hot work permit templateA hot work permit with a precautions checklist, fire watch record and close-out, plus an Excel permit log.
- Confined space entry permit templateA confined space entry permit with checks, an air test log, an entry log and cancellation, plus an Excel register.
- Energy loss matrix templateSeven types of energy loss by six energy sources with a cost in each cell, an action plan and an idle-period shutdown checklist.
- Management safety tour formA leader's scheduled safety walk: observation form, operator interview, tally, actions, rota and a tour log with a dashboard.
- Chemical inventory and SDS register templateA register of every chemical on site with its hazard class, safety data sheet and label, and a check that incompatible products are kept apart.
- Safety committee meeting minutes templateMinutes for a safety committee: attendance, nine agenda items, an action log that carries open actions forward, and monthly numbers.
- Environmental compliance audit checklistAn internal environmental audit: 37 questions with what to look for, a findings log with classes and a score by section.
- Management of change formA change request and review form for a plant: what changes, the hazard review, approvals, pre-startup review, training and close-out.
- Silica exposure control plan templateA written silica plan for general industry: tasks, controls and housekeeping, plus monitoring, medical surveillance, training and a 31-check plan audit.
Can't find the template you need?
Tell us what you're looking for. We'll make it and send it to your inbox, free.
A shift handover sheet, a red tag log, a changeover checklist for one machine: if your team uses it on the floor, ask.